For industrial operations dealing with sintered ash powders, the selection of an appropriate conveying equipment is crucial for efficiency and safety. This article explores the nature of sintered ash powder conveying equipment and delves into its core design principles, providing insights that can aid in understanding and selecting the right solution for specific applications.
Introduction to Sintered Ash Powder Conveying Equipment
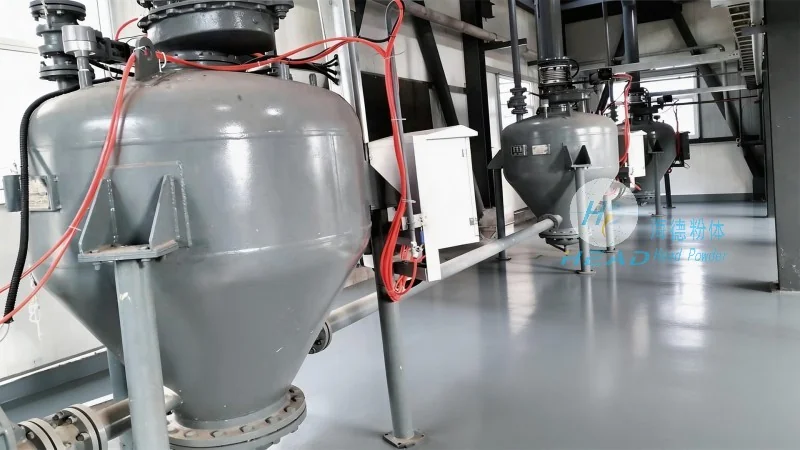
Sintered ash powder, a byproduct of industrial processes such as power generation and metal smelting, requires specialized handling due to its fine particle size and potential for dust generation. Conveying equipment designed for this material must address challenges like dust control, material flow uniformity, and equipment durability. The equipment in question, often referred to as a sintered ash powder conveying system, is engineered to transport these powders from one location to another within industrial facilities, ensuring seamless integration into production workflows.
About HeadPowder: A Leading Provider of Conveying Solutions
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a reputable company based in Shandong, China, specializing in the design, manufacturing, and supply of advanced conveying equipment for various industrial applications. With a strong commitment to quality and innovation, HeadPowder has established itself as a trusted partner for businesses seeking reliable solutions for material handling challenges. The company’s expertise lies in developing customized conveying systems that meet the unique demands of clients, ensuring optimal performance and longevity.
Key Features of Sintered Ash Powder Conveying Equipment
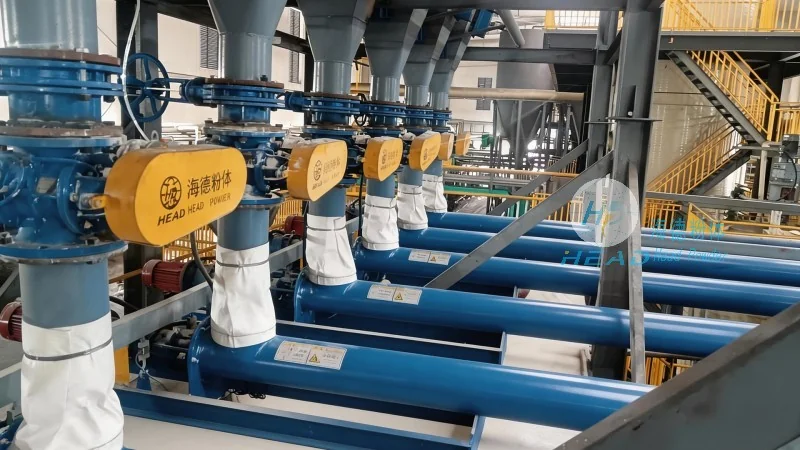
The sintered ash powder conveying equipment typically incorporates several key components that work in harmony to ensure efficient operation. These may include a hopper for material storage, a feeding mechanism to control the flow rate, a conveyor system (such as a screw or pneumatic conveyor) to transport the powder, and a dust collection system to maintain air quality. The design emphasizes minimal material degradation, preventing agglomeration or loss of fine particles, which is critical for maintaining product quality. Additionally, the equipment is constructed from materials resistant to corrosion and abrasion, ensuring it can withstand the harsh conditions associated with sintered ash handling.
Design Principles Underpinning the Equipment
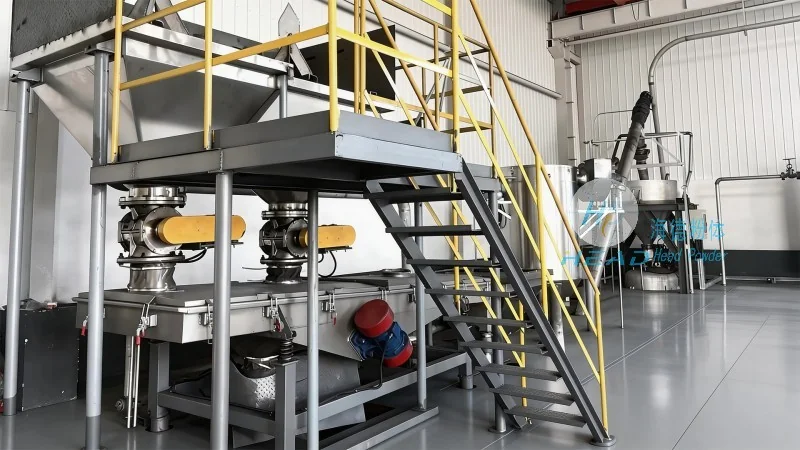
The design principles of sintered ash powder conveying equipment are centered on several critical factors. First, the system must ensure consistent and controlled material flow to prevent blockages or uneven delivery. This is achieved through precise control mechanisms and appropriate hopper geometry. Second, dust containment is a paramount concern, as sintered ash powders are often fine and can create hazardous airborne particles. The equipment incorporates sealed enclosures and efficient filtration systems to minimize dust emissions and maintain a safe working environment. Third, energy efficiency is a key design consideration, with systems optimized to reduce power consumption while maintaining high throughput. Finally, the equipment is designed for easy maintenance and cleaning, allowing for quick adjustments and minimizing downtime during operation.
Application-Specific Considerations
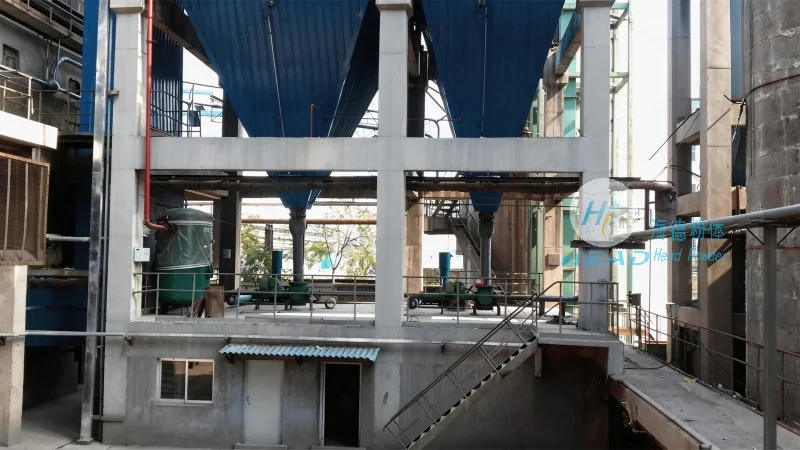
When selecting a sintered ash powder conveying equipment, several factors must be considered to ensure it meets the specific needs of the application. The particle size distribution of the sintered ash, for instance, influences the choice of conveyor type—screw conveyors may be suitable for cohesive materials, while pneumatic conveyors are better for fine, free-flowing powders. The distance and elevation changes between the source and destination of the material also impact the design, with some systems requiring additional components like elevators or vertical conveyors. Furthermore, the scale of the operation, whether it is a small-scale process or a large industrial plant, dictates the capacity and complexity of the conveying system. HeadPowder’s expertise allows them to tailor solutions to these specific requirements, providing customized equipment that maximizes performance and reliability.
Conclusion
In conclusion, sintered ash powder conveying equipment is a specialized solution designed to handle the unique challenges of transporting fine, potentially dusty materials. The design principles, which prioritize material flow control, dust containment, energy efficiency, and ease of maintenance, are crucial for ensuring the equipment operates effectively and safely. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these advanced systems, helping industrial facilities optimize their material handling processes and improve overall operational efficiency. By understanding the design and functionality of such equipment, businesses can make informed decisions that enhance productivity and compliance with safety standards.




