Understanding the cement fly ash powder conveying system equipment and its design principles is crucial for industries dealing with bulk powder materials. This equipment is specifically engineered to handle the transportation of cement and fly ash, two key components in construction and industrial applications. The system ensures efficient, reliable, and safe movement of these powders from storage to processing or application points.
Overview of the Cement Fly Ash Powder Conveying System
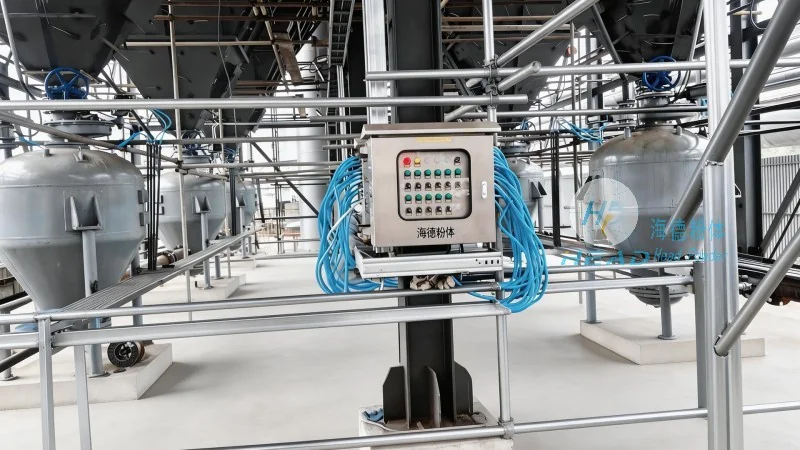
The cement fly ash powder conveying system is a specialized piece of industrial equipment designed to transport bulk powders such as cement and fly ash. These materials are often used in large quantities in construction, manufacturing, and other industrial sectors. The system typically includes components like hoppers, feeders, conveyors, and control systems to ensure smooth and continuous operation. The primary goal is to maintain the integrity of the powders, prevent segregation, and minimize dust generation during transport.
Key Components and Their Functions
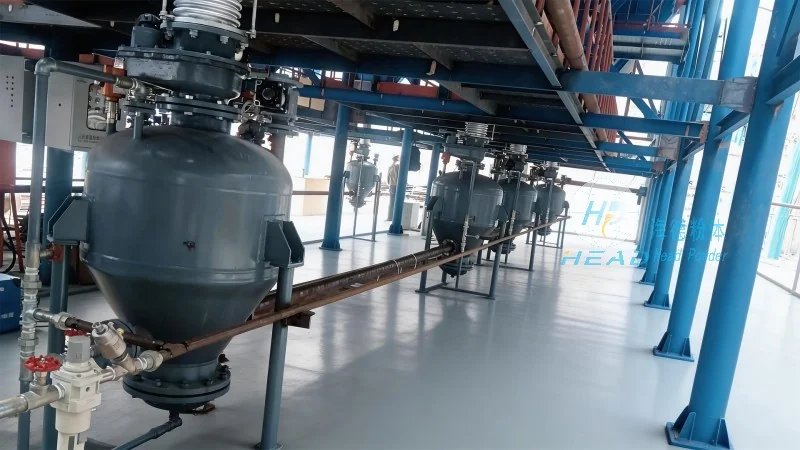
Several critical components make up the cement fly ash powder conveying system. The hopper serves as the storage container, holding the bulk material until it is needed. The feeder, often a rotary or vibratory type, regulates the flow of material from the hopper into the conveyor. The conveyor itself, which can be a pneumatic or mechanical system, transports the powder to the desired location. Control systems are integrated to monitor and adjust the flow rate, ensuring optimal performance and safety. Each component plays a vital role in maintaining the efficiency and reliability of the entire system.
Design Principles for Efficient Powder Conveying
The design principles of the cement fly ash powder conveying system focus on several key aspects to ensure effective operation. First, the system must handle the physical properties of the powders, such as particle size, density, and flowability. This involves selecting appropriate materials for the hopper and conveyor to prevent wear and ensure durability. Second, the system is designed to minimize segregation, where different particle sizes or densities separate during transport. This is achieved through proper feeding mechanisms and conveyor design. Third, dust control is a critical design consideration, as powders like cement and fly ash can be hazardous if inhaled. The system incorporates dust collection and filtration systems to maintain a safe working environment. Finally, the design prioritizes energy efficiency and low maintenance, making it suitable for long-term industrial use.
Application in Cement and Fly Ash Handling
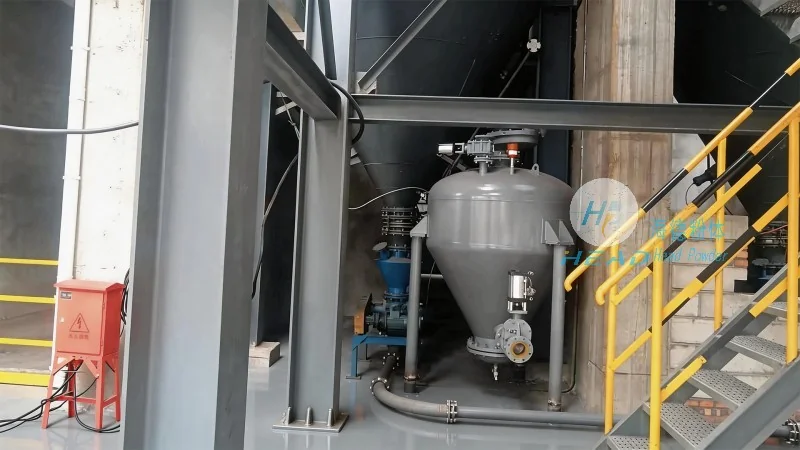
The cement fly ash powder conveying system is widely used in the cement industry for transporting raw materials and finished products. In the case of fly ash, which is a byproduct of coal combustion, the system helps in the efficient handling and utilization of this material. The system ensures that fly ash is transported from storage facilities to cement production lines or other processing sites without loss or contamination. This not only improves operational efficiency but also contributes to sustainable practices by utilizing fly ash as a supplementary cementitious material.
Advantages of the System
Implementing a cement fly ash powder conveying system offers several advantages for industrial operations. One of the main benefits is the reduction in labor costs associated with manual handling of bulk powders. The system automates the process, allowing for continuous and consistent operation. Additionally, it minimizes material loss and contamination, which can be costly in the cement and construction industries. The system also enhances safety by reducing exposure to dust and preventing accidents related to manual handling. Furthermore, the design allows for easy integration with existing production lines, making it a versatile solution for various industrial applications.
Conclusion
In conclusion, the cement fly ash powder conveying system equipment is a vital component in industries that rely on bulk powder materials. Its design principles focus on efficiency, safety, and durability, ensuring reliable transportation of cement and fly ash. The system's components work together to maintain the quality of the powders and optimize operational performance. For companies dealing with these materials, investing in such a system can lead to significant improvements in productivity and cost-effectiveness. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality conveying systems tailored to the specific needs of various industrial applications.




