Rare earth minerals are crucial components in modern industrial applications, and the efficient transport of these fine powders is essential for maintaining production efficiency and product quality. This article explores the nature of rare earth mineral powder material handling equipment and delves into its fundamental design principles, providing a comprehensive understanding of how such systems operate and are engineered.
Components and Core Design Principles of the Equipment
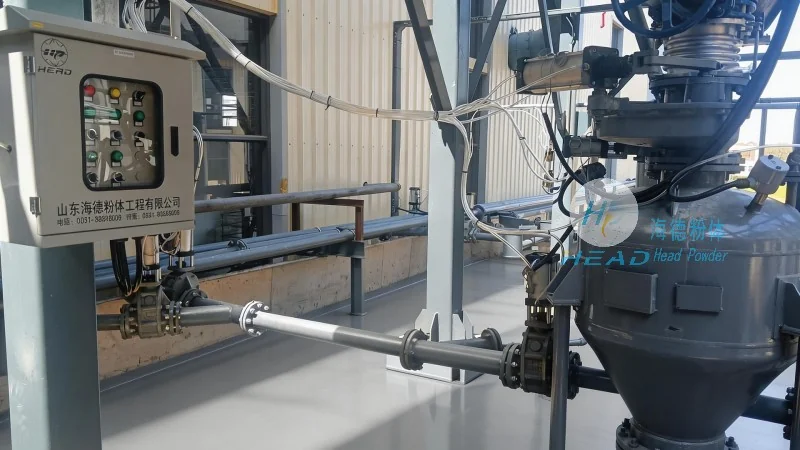
Headpowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced material handling solutions for rare earth mineral powders. The equipment typically consists of several key components, each playing a vital role in the overall system. The primary design principles are centered on ensuring high efficiency, minimal material loss, and compliance with safety and environmental standards.
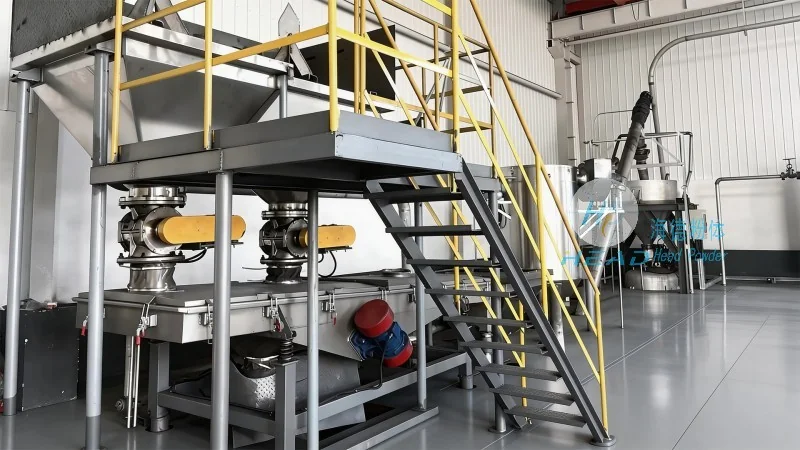
One of the critical components is the feeding system, which is designed to handle the fine, abrasive nature of rare earth powders. This system often includes a hopper or feeder that can control the flow rate of the material, preventing overloading and ensuring a consistent feed to the subsequent processing stages. The design of the feeding mechanism is crucial to avoid agglomeration or caking of the powder, which could lead to blockages and reduced system performance.
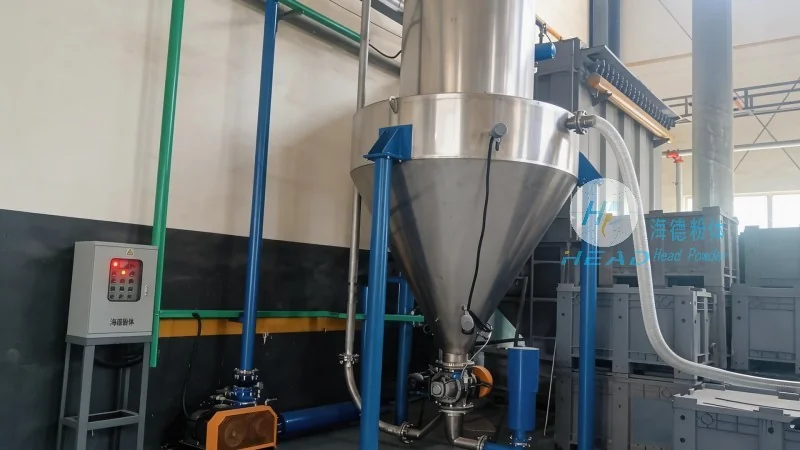
The conveying mechanism, another essential part of the equipment, is engineered to transport the powder from the feeding point to the discharge point. Common types include pneumatic conveying systems, screw conveyors, and belt conveyors, each with its own advantages and applications. For rare earth powders, which are often sensitive to moisture and contamination, the choice of conveying method is critical. For instance, pneumatic systems can provide a closed-loop transport, minimizing exposure to the environment and reducing the risk of dust emissions. The design of the conveying line, including the pipe diameter, velocity, and pressure, is carefully calculated to ensure that the powder is transported without degradation or loss.
The control and monitoring system is also a key element, enabling operators to manage the equipment efficiently. This system may include sensors to monitor flow rates, pressure, and temperature, as well as control panels to adjust settings in real-time. The design of the control system is aimed at providing precise control over the entire process, allowing for quick adjustments to maintain optimal performance and prevent issues such as overloading or underflow.
About Headpowder: Your Trusted Partner in Material Handling
Headpowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable company dedicated to providing high-quality material handling solutions for various industrial applications, with a particular focus on rare earth mineral powders. The company leverages years of experience and advanced engineering capabilities to design and manufacture equipment that meets the stringent requirements of modern industries. By adhering to rigorous quality standards and employing innovative design approaches, Headpowder ensures that its equipment is reliable, efficient, and durable, helping clients enhance their production processes and achieve better results.
Conclusion
In summary, rare earth mineral powder material handling equipment is a sophisticated system designed to address the unique challenges of transporting fine, valuable powders. The design principles, including careful consideration of material properties, efficient conveying methods, and robust control systems, are essential for achieving optimal performance. With the expertise and commitment of companies like Headpowder, these systems can effectively support industrial operations, ensuring the safe and efficient handling of rare earth minerals.




