Stone aggregate conveyor systems are essential equipment in various industrial and construction applications, designed to transport bulk materials such as gravel, sand, and crushed stone efficiently. These systems play a crucial role in material handling processes, ensuring smooth and continuous operation in mining, quarrying, and construction sites. Understanding the components and design principles of such systems is vital for optimizing productivity and operational efficiency.
Key Components of a Stone Aggregate Conveyor System
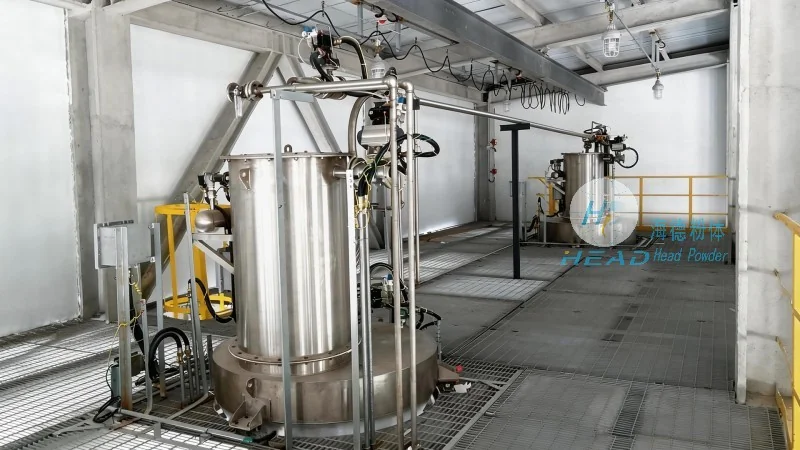
A typical stone aggregate conveyor system consists of several key components that work together to facilitate material transport. The primary components include the conveyor belt, idlers, pulleys, drive systems, and feeding mechanisms. The conveyor belt, often made from durable materials like rubber or synthetic fabrics, carries the aggregate from the source to the destination. Idlers support the belt and maintain proper tension, while pulleys guide the belt and provide the necessary friction for movement. Drive systems, such as electric motors and gearboxes, power the conveyor, ensuring consistent speed and performance. Feeding mechanisms, like hoppers or feeders, control the flow of material onto the belt, preventing overloading and ensuring uniform transport.
Design Principles for Efficient Material Handling
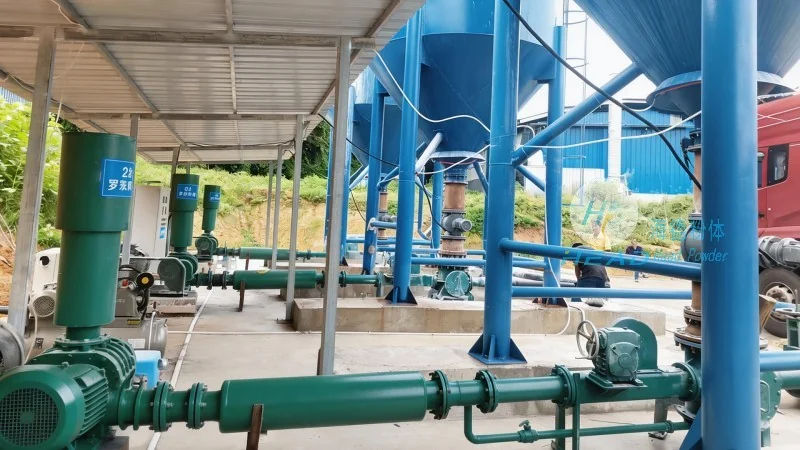
The design of a stone aggregate conveyor system is based on several critical principles to ensure optimal performance. First, the system must be designed to handle the specific characteristics of the material, including its size, shape, and moisture content. This involves selecting appropriate belt materials and pulley sizes to prevent material degradation or belt damage. Second, the system must be engineered for durability and longevity, as it operates in harsh environments with high stress and wear. Materials like heavy-duty steel and reinforced belts are commonly used to withstand continuous use. Third, the design must prioritize energy efficiency, minimizing power consumption while maintaining high throughput. This is achieved through optimized belt tension, efficient drive systems, and proper maintenance protocols. Additionally, the system should be designed for easy maintenance and accessibility, allowing for quick repairs and component replacements without disrupting operations.
Applications in Industrial and Construction Settings
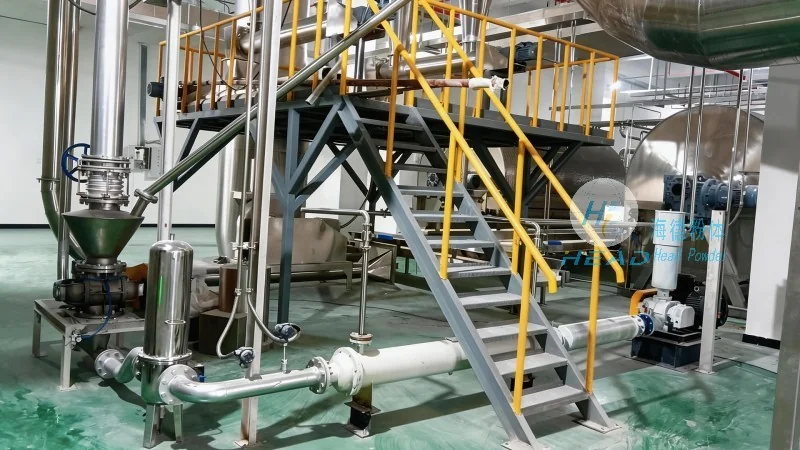
Stone aggregate conveyor systems are widely used in various industries, including mining, quarrying, and construction. In mining operations, these systems transport extracted stone from the quarry to processing facilities or storage areas. In construction sites, they move aggregates from stockpiles to mixing plants or other work areas, supporting the production of concrete, asphalt, and other building materials. The versatility of these systems makes them suitable for both large-scale industrial applications and smaller construction projects. By efficiently handling bulk materials, conveyor systems contribute to improved workflow, reduced labor costs, and enhanced overall productivity in these settings.
Advantages of Using Stone Aggregate Conveyor Systems
Implementing a stone aggregate conveyor system offers numerous advantages for businesses in the material handling sector. One of the primary benefits is increased efficiency, as these systems can transport large volumes of material continuously without the need for manual labor. This reduces the time and effort required for material movement, allowing workers to focus on other critical tasks. Another advantage is cost savings, as conveyor systems minimize material handling costs and reduce the risk of accidents or injuries associated with manual handling. Additionally, these systems improve safety by eliminating the need for workers to handle heavy or bulky materials, thereby reducing workplace hazards. Furthermore, the consistent and controlled flow of material provided by conveyor systems enhances the quality of the final product, as it prevents material segregation and ensures uniform composition. These advantages make stone aggregate conveyor systems a valuable investment for businesses seeking to optimize their material handling processes.
Conclusion and Company Overview
Stone aggregate conveyor systems are indispensable tools in modern material handling, offering efficient and reliable solutions for transporting bulk materials. The design principles and components of these systems are carefully engineered to meet the demands of industrial and construction applications, ensuring durability, efficiency, and safety. For businesses looking to enhance their material handling capabilities, investing in a well-designed conveyor system is a strategic decision that can lead to improved productivity and cost savings. As a leading provider in the industry, Shandong HeadPowder Engineering Co., Ltd. specializes in manufacturing high-quality stone aggregate conveyor systems tailored to the specific needs of its clients. With a focus on durability, efficiency, and customer satisfaction, HeadPowder offers solutions that meet the rigorous demands of the mining, quarrying, and construction sectors. Based in Shandong, China, the company leverages its expertise and advanced technology to deliver reliable and effective conveyor systems that contribute to the success of its clients' operations.




