

What is an Intelligent Bulk Bag Unloading Pneumatic Conveying Machine? And What Are Its Design Princ
For industries dealing with bulk powders, efficient and reliable material handling is crucial. The intelligent bulk bag unloading pneumatic conveying machine has emerged as a sophisticated solution to streamline the process of handling and transporting powders from bulk bags. This equipment integrates advanced technology to automate the unloading, conveying, and storage of powders, significantly improving operational efficiency and reducing labor costs. Understanding its design principles is essential for users to make informed decisions about implementing such systems in their facilities.
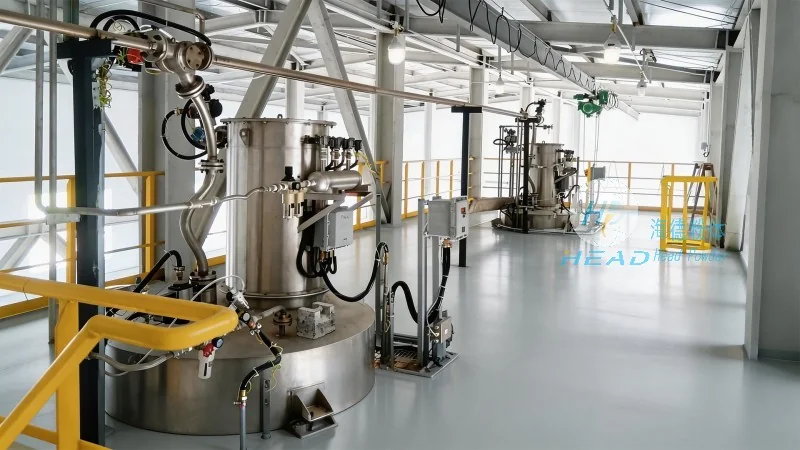
Understanding the Intelligent Bulk Bag Unloading Pneumatic Conveying Machine
At its core, an intelligent bulk bag unloading pneumatic conveying machine is a system designed to handle the entire process of transferring powders from a bulk bag into a storage silo or other processing equipment. The system typically comprises several key components, including a bulk bag discharger, a pneumatic conveying line, a dust collection system, and a control panel. Each component works in harmony to ensure a seamless and efficient operation.
Key Components and Their Functions
The bulk bag discharger is the initial stage of the system, responsible for safely and efficiently opening the bulk bag and releasing the powder into the conveying system. This component often includes a bag support frame, a bag opening mechanism (such as a valve or a spout), and a hopper that collects the material as the bag empties. The design of the discharger is critical to prevent spillage and ensure a clean transfer, which is vital for maintaining product quality and compliance with safety regulations.
The pneumatic conveying system is the heart of the machine, responsible for transporting the powder from the discharger to the destination silo or processing unit. This system utilizes compressed air to move the powder through a pipeline. There are two main types of pneumatic conveying: positive pressure and negative pressure. Positive pressure systems blow air into the conveying line, pushing the powder forward, while negative pressure systems create a vacuum to draw the powder. The choice of system depends on factors such as the powder's properties, the distance to be conveyed, and the desired flow rate.
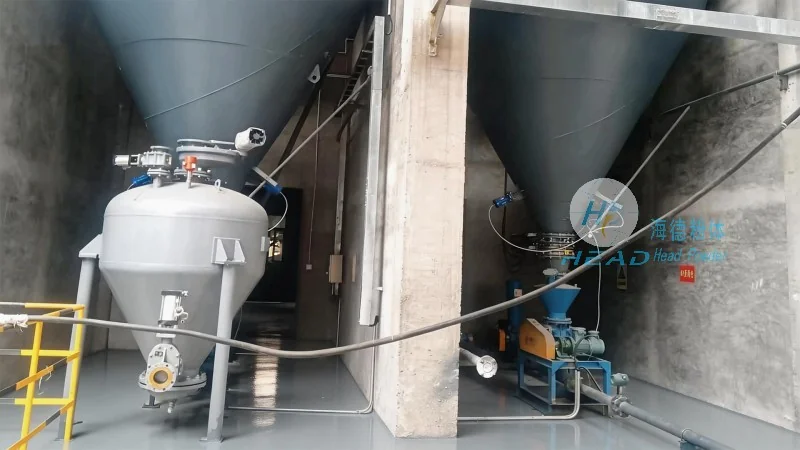
The dust collection system is an integral part of the design, ensuring that the operation is safe and environmentally compliant. It captures any airborne particles and returns them to the conveying line or stores them in a separate container. This not only prevents dust contamination but also helps maintain a clean working environment, which is essential for both employee health and product integrity.
Design Principles and Operational Efficiency
The design of an intelligent bulk bag unloading pneumatic conveying machine is guided by several key principles aimed at maximizing efficiency and reliability. One of the primary principles is automation, which reduces the need for manual intervention and minimizes the risk of human error. The control panel, equipped with sensors and programmable logic controllers (PLCs), monitors the entire process and adjusts parameters in real-time to maintain optimal performance.
Another important principle is modularity, allowing the system to be customized to meet specific operational requirements. Users can select components such as the type of bulk bag discharger, the conveying line diameter, and the control system based on their application needs. This flexibility ensures that the machine can be adapted to handle a wide range of powder types, from fine powders to bulkier materials, and accommodate varying production volumes.
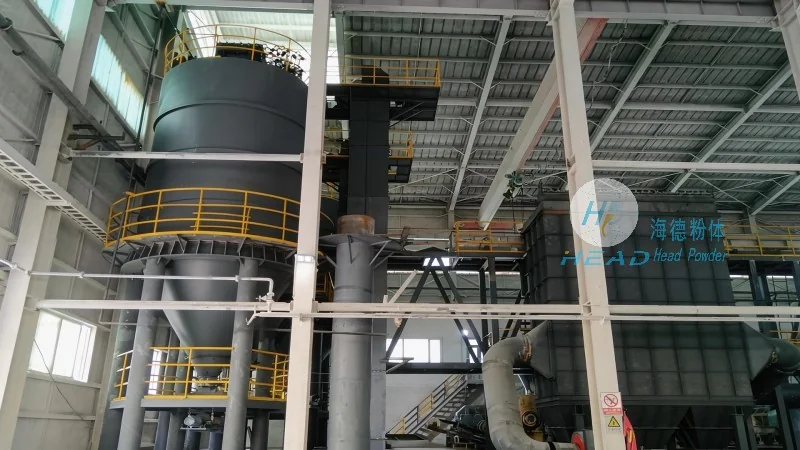
Energy efficiency is also a critical design consideration. Modern systems incorporate features such as variable frequency drives (VFDs) to regulate the speed of the air compressor, reducing energy consumption during low-demand periods. Additionally, the use of high-efficiency filters and optimized conveying line designs minimizes air loss and improves overall energy efficiency.
Benefits of Implementing This Technology
Adopting an intelligent bulk bag unloading pneumatic conveying machine offers numerous benefits for industrial operations. Firstly, it significantly improves operational efficiency by automating the entire powder handling process. This reduces downtime and increases production throughput, allowing companies to meet higher demand without additional labor. Secondly, it enhances product quality by minimizing contamination and ensuring a consistent flow of material. The enclosed system prevents exposure to dust and moisture, which can affect the quality of the powder.
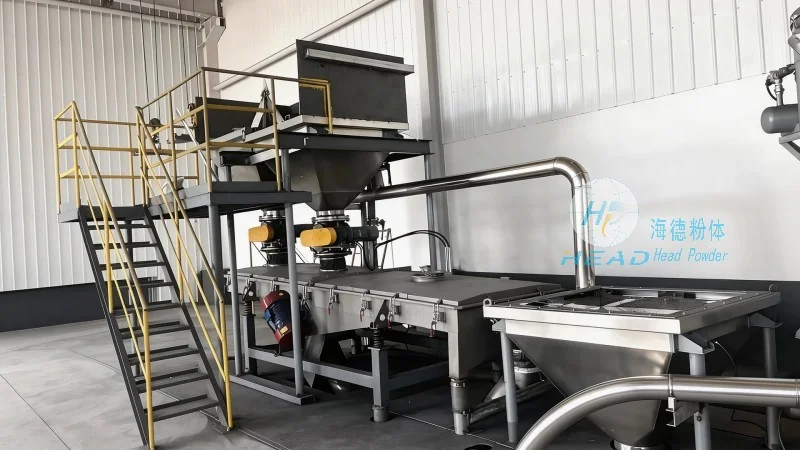
Thirdly, the system enhances safety by reducing the risk of manual handling of bulk bags, which can be hazardous. The automated process eliminates the need for workers to handle heavy bags or operate equipment manually, thereby reducing the risk of accidents and injuries. Additionally, the dust collection system helps maintain a safe working environment by controlling airborne particles.
Fourthly, the system improves cost-effectiveness by reducing labor costs and minimizing material waste. The automated unloading and conveying process reduces the need for manual labor, which can be a significant expense in many industries. Additionally, the enclosed system minimizes material loss during transfer, reducing waste and lowering overall operational costs.
Conclusion
The intelligent bulk bag unloading pneumatic conveying machine is a sophisticated and efficient solution for handling bulk powders. Its design, based on principles of automation, modularity, and energy efficiency, ensures that it can meet the diverse needs of modern industrial operations. By integrating advanced technology and components, this equipment streamlines the powder handling process, improves product quality, enhances safety, and reduces costs. For companies looking to optimize their material handling operations, investing in such a system can provide significant long-term benefits.