

Working Principle and Features of Gravity Dust Removal Pneumatic Conveying Equipment
Gravity dust removal pneumatic conveying equipment is a specialized system designed to handle and transport fine particulate materials while simultaneously removing dust from the air. This technology is widely used in industrial settings where air quality control and material handling efficiency are critical. The equipment combines dust filtration and material transport functions, making it an essential component in processes such as cement production, chemical processing, and food processing.
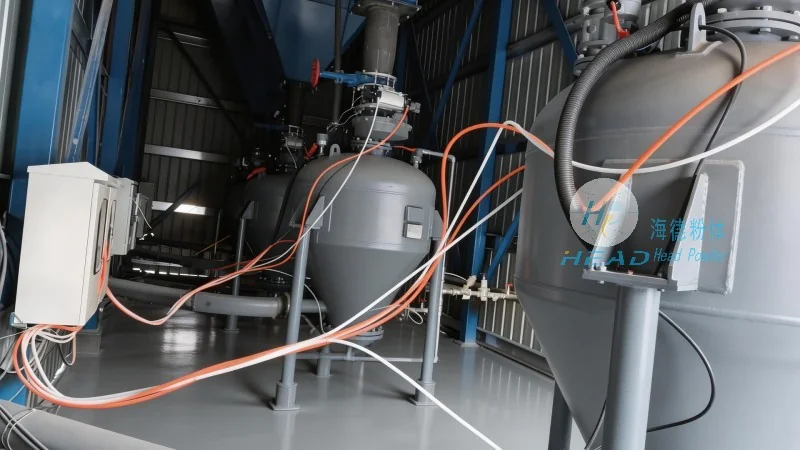
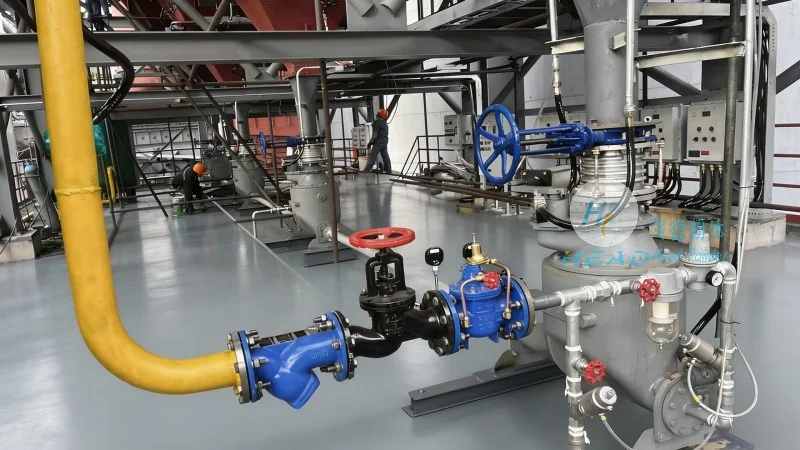
Working Principle of the Gravity Dust Removal Pneumatic Conveying Equipment
The core working principle of this equipment involves the use of a combination of gravity separation and pneumatic conveying mechanisms. The system typically consists of a dust collector, a conveying pipeline, and a material discharge unit. As air flows through the system, fine dust particles are separated from the air stream by a gravity separator or cyclone. The purified air is then directed back into the environment or re-used in the process. Simultaneously, the separated dust is collected and transported through the conveying pipeline to a designated storage or processing location. The equipment operates by creating a pressure differential between the inlet and outlet, which enables the efficient movement of both the air and the material. The design ensures that the dust removal process is integrated seamlessly with the material conveying process, minimizing energy consumption and maximizing operational efficiency.
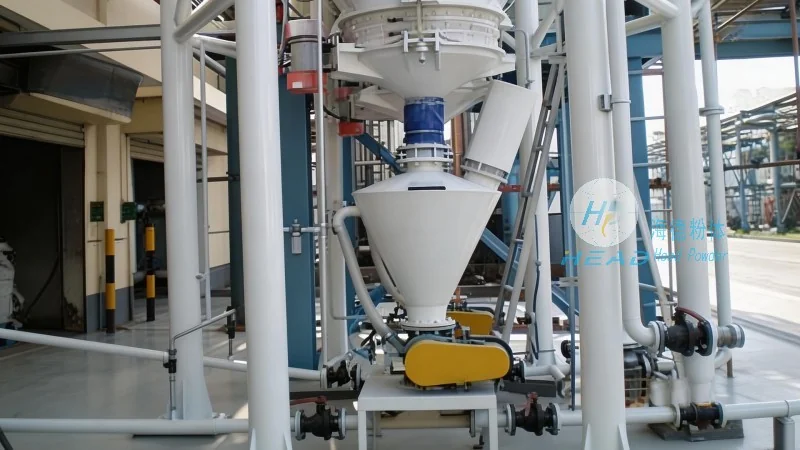
Key Features of the Equipment
One of the primary features of gravity dust removal pneumatic conveying equipment is its high efficiency in dust filtration. The system is capable of capturing a large proportion of fine particulate matter, reducing air pollution and improving workplace safety. Another significant feature is the stable and reliable material conveying performance. The equipment can handle a wide range of materials, including powders, granules, and fine particles, with minimal degradation or loss. The design also emphasizes low energy consumption, as the use of gravity separation reduces the need for high-pressure air systems, which are often energy-intensive. Additionally, the equipment is designed for easy maintenance and operation, with accessible components and automated control systems that simplify routine checks and adjustments.
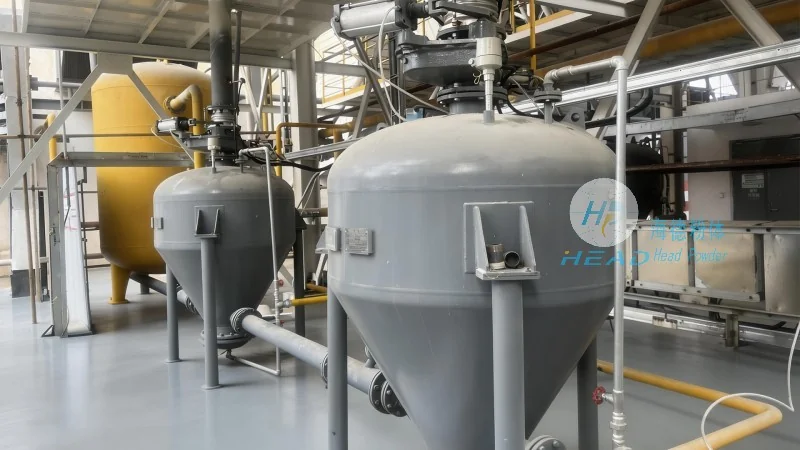
Technical Advantages and Practical Applications
The technical advantages of this equipment make it a preferred choice for industries that require both efficient material handling and effective air purification. For example, in cement manufacturing, the equipment can be used to transport raw materials and remove dust from the production line, contributing to cleaner emissions and improved product quality. In chemical processing, it helps in handling hazardous powders while maintaining a safe working environment. The equipment is also suitable for applications in the food industry, where dust removal is crucial for maintaining product purity and compliance with health regulations. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized gravity dust removal pneumatic conveying systems tailored to the specific needs of various industries. The company’s expertise ensures that each system is optimized for performance, durability, and cost-effectiveness, providing long-term value to its clients.