Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in engineering solutions for material handling, including advanced pneumatic conveying systems tailored for corn cobs and similar bulk materials. This article explores the working principle and key characteristics of pneumatic conveying for corn cobs material, providing insights into how such systems operate and their benefits in industrial applications.
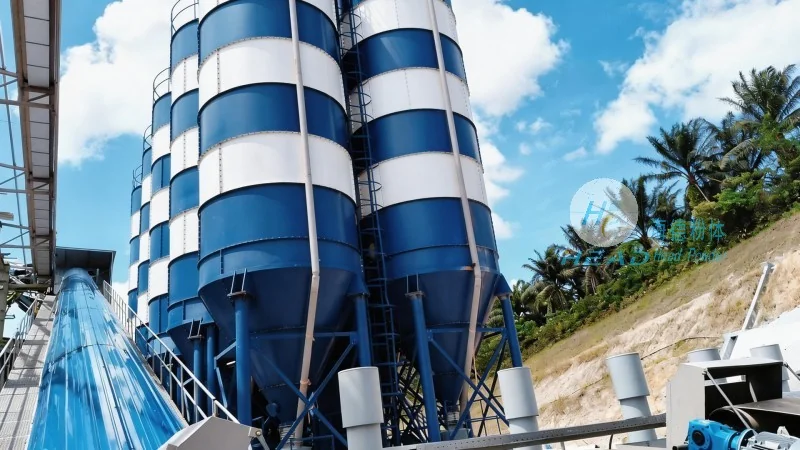
Pneumatic conveying, also known as air conveying, is a method of transporting bulk solid materials through a pipeline using a stream of air. The core principle involves creating a pressure differential—either by generating positive pressure (pressure conveying) or negative pressure (vacuum conveying)—to move the material. For corn cobs, which are typically irregularly shaped and have a relatively low bulk density, pneumatic conveying offers an efficient solution to transport these materials over short to medium distances within industrial facilities.
The working principle of corn cobs material pneumatic conveying systems can be broken down into several key components. First, the material is fed into a hopper or feeder, where it is introduced into the conveying line. A fan or blower then generates the necessary air flow, either by pushing air through the line (pressure system) or pulling air from the line (vacuum system). The air stream, combined with the material, travels through the pipeline to the discharge point. At the end of the line, a separator or cyclone separates the material from the air, allowing the corn cobs to be collected while the air is either filtered or recirculated.
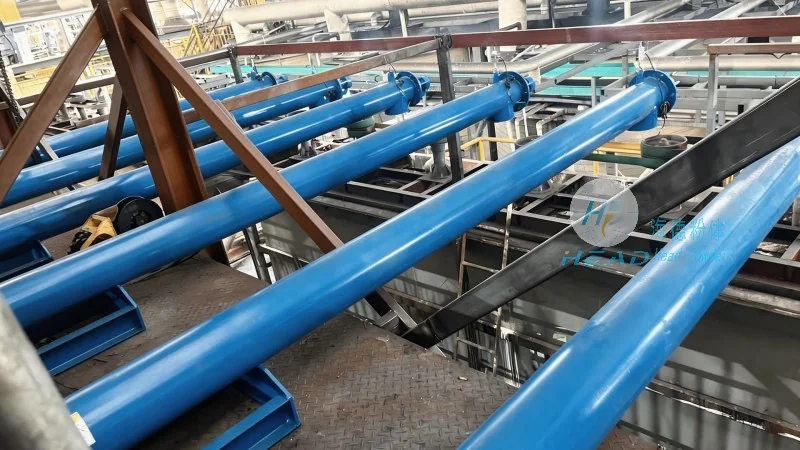
One of the primary advantages of pneumatic conveying for corn cobs is its ability to handle materials with varying properties. Corn cobs are often mixed with other byproducts or have moisture content that can affect traditional handling methods. Pneumatic systems can accommodate these variations, ensuring consistent and reliable transport. Additionally, this method is highly efficient in terms of space utilization, as it eliminates the need for large storage silos or conveyor belts that occupy significant floor space.
Another significant characteristic is the environmental benefits of pneumatic conveying. Unlike mechanical systems that may generate dust or require frequent maintenance, pneumatic systems are enclosed, reducing dust emissions and improving workplace safety. The enclosed design also minimizes the risk of material spillage or contamination, which is crucial for food-grade or high-purity applications where corn cobs might be used as animal feed or in biofuel production.
Efficiency and automation are also key features of corn cobs pneumatic conveying systems. Modern systems often integrate sensors and control panels that monitor air pressure, material flow, and system performance in real-time. This allows for automatic adjustments to maintain optimal conveying rates, reducing downtime and increasing overall productivity. For industrial operations that process large volumes of corn cobs, such automation is essential to meet production demands while maintaining quality standards.
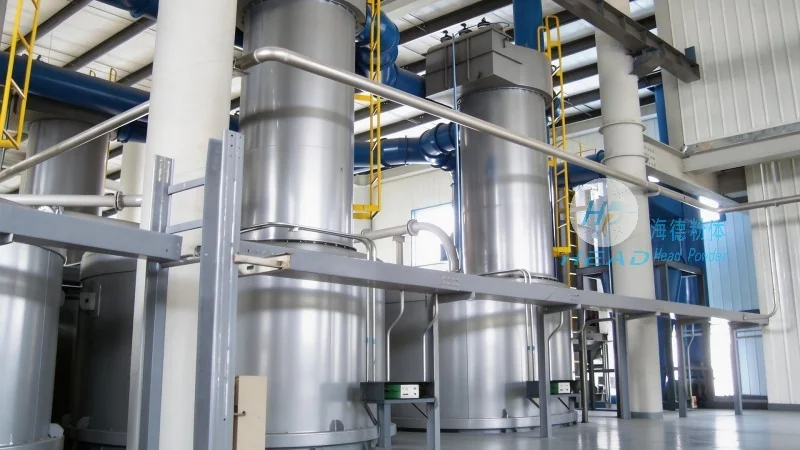
Furthermore, the flexibility of pneumatic conveying systems makes them suitable for various applications within the corn processing industry. Whether used for transporting raw corn cobs from storage to processing units, moving byproducts to storage areas, or even for transporting finished products like corn meal or feed, these systems can be customized to fit specific workflow requirements. The ability to adjust the conveying line length, diameter, and pressure levels allows for adaptability across different plant layouts and operational scales.
In summary, pneumatic conveying for corn cobs material is a robust and efficient method that leverages air flow to transport bulk materials. By understanding the working principle—combining material feeding, air generation, and separation—and recognizing its characteristics, such as adaptability, environmental friendliness, and automation capabilities, industries can optimize their material handling processes. Shandong HeadPowder Engineering Co., Ltd. provides specialized engineering solutions for these systems, ensuring that corn cobs are handled safely and effectively in various industrial settings.




