HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. The intelligent centralized pneumatic conveying line is a sophisticated solution that integrates modern technology to enhance material handling efficiency and operational reliability in various industrial settings.
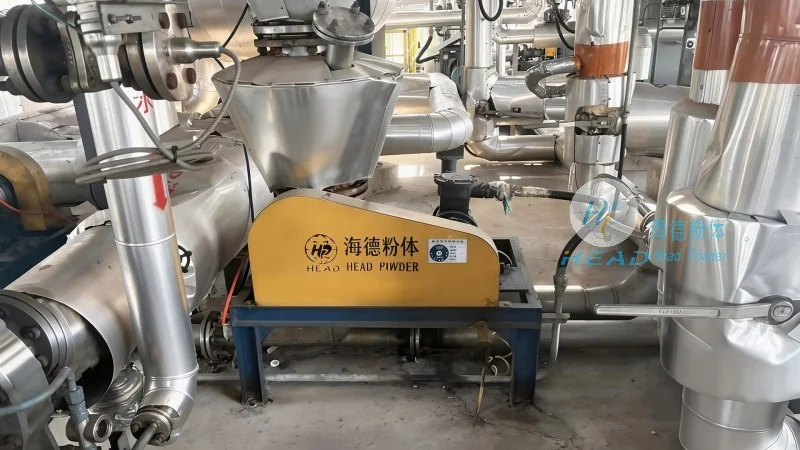
Principles of Intelligent Centralized Pneumatic Conveying Lines
The core principle of an intelligent centralized pneumatic conveying line lies in its centralized control and automated material transport. Unlike traditional systems that rely on multiple individual components, this system uses a single, centralized control unit to manage the entire conveying process. This approach minimizes the need for manual intervention and reduces the likelihood of operational errors. The system typically operates by drawing material from a storage hopper or silo and transporting it through a network of pipes using compressed air. The intelligent features may include real-time monitoring of pressure, flow rates, and material levels, as well as automatic adjustments to optimize performance. This centralized approach ensures consistent and reliable material transport, even with varying material types and flow rates.
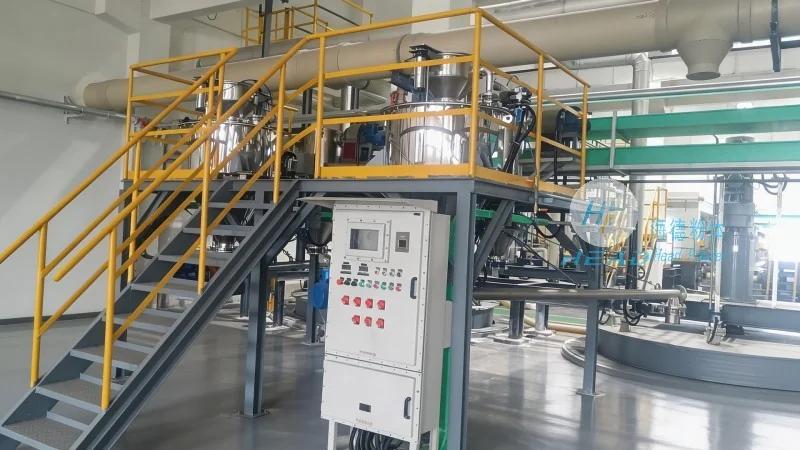
Key Components and Their Functions
Several critical components work together to ensure the smooth operation of the intelligent centralized pneumatic conveying line. The primary components include a material feed hopper, a rotary airlock valve, a main conveying pipe, a dust filter system, and a central control panel. The material feed hopper stores the bulk material and feeds it into the system at a controlled rate. The rotary airlock valve acts as a gate, preventing backflow and ensuring a steady flow of material into the conveying pipe. The main conveying pipe transports the material from the feed point to the discharge point, often using a combination of positive and negative pressure to move the material efficiently. The dust filter system captures any airborne particles, ensuring compliance with environmental regulations and maintaining a clean working environment. The central control panel allows operators to monitor and adjust system parameters, such as air pressure, flow rate, and material feed speed, in real-time. This integration of components ensures that the system operates efficiently and safely, minimizing downtime and maintenance requirements.
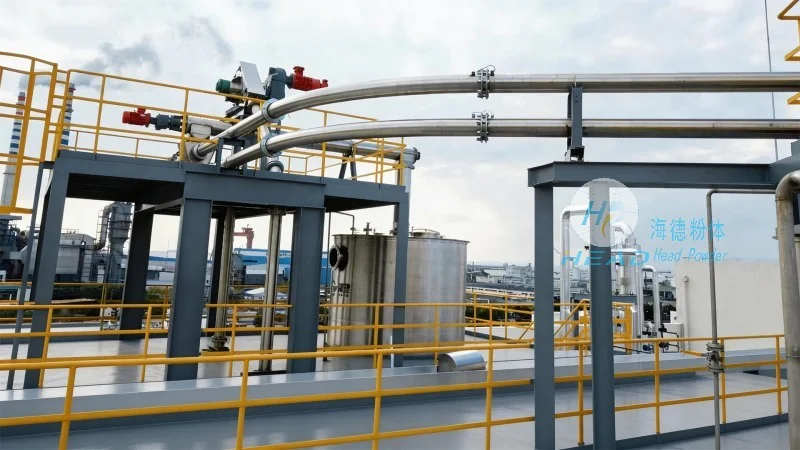
Application Scenarios and Benefits
The intelligent centralized pneumatic conveying line is particularly well-suited for applications in industries that require the handling of bulk materials, such as chemicals, food processing, pharmaceuticals, and cement. In these industries, the system offers several key benefits. First, it provides a dust-free and hygienic environment, which is crucial for industries like food and pharmaceuticals where contamination control is paramount. Second, the centralized control system reduces labor costs by minimizing the need for manual handling and monitoring. Third, the system's efficiency in material transport reduces energy consumption and operational costs compared to traditional methods. Additionally, the system's flexibility allows it to handle a wide range of material types, from fine powders to bulk solids, making it a versatile solution for various industrial needs. In the chemical industry, for example, the system can transport hazardous materials safely and efficiently, while in the food industry, it can handle sensitive products without compromising quality. The benefits extend to improved product quality, as the system minimizes material degradation and contamination during transport. Overall, the intelligent centralized pneumatic conveying line offers a reliable and efficient solution for material handling in modern industrial applications.
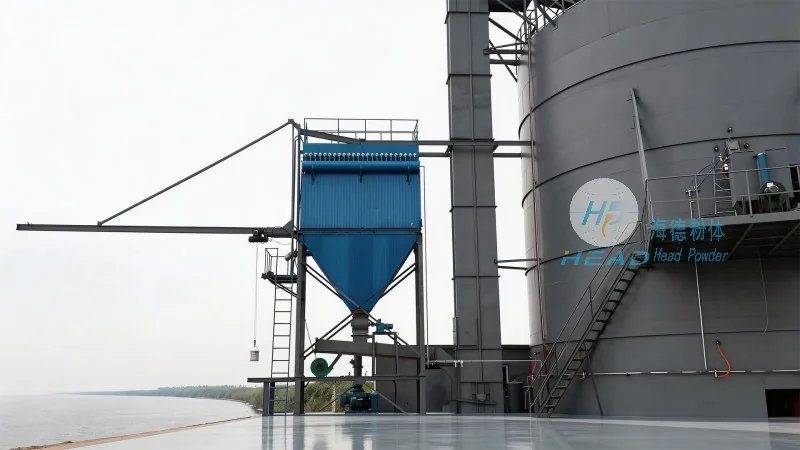
Operational Advantages and Performance Metrics
One of the significant advantages of the intelligent centralized pneumatic conveying line is its ability to maintain consistent performance under varying conditions. The system's automated controls adjust to changes in material properties, such as density and moisture content, ensuring optimal conveying rates. This adaptability is particularly important in industries where material characteristics can fluctuate, such as in mining or agricultural processing. Performance metrics, such as conveying capacity, pressure drop, and energy efficiency, are closely monitored and optimized through the central control system. The system's design also minimizes maintenance requirements, as components are strategically placed and easily accessible for inspection and repair. This reduces downtime and increases the overall availability of the system. Furthermore, the system's scalability allows it to be expanded or modified to accommodate growing production needs, making it a long-term investment for industrial operations. The combination of these operational advantages makes the intelligent centralized pneumatic conveying line a preferred choice for companies seeking to enhance their material handling capabilities.




