HeadPowder, a leading manufacturer based in Shandong, China, specializes in designing and manufacturing advanced pneumatic conveying equipment tailored for grain silos. This equipment is essential for efficiently handling bulk materials like grains, seeds, and other agricultural products within storage facilities. The following sections will explore the fundamental principles behind these systems and the diverse operational scenarios where they are applied.
Core Principles of Pneumatic Conveying Technology
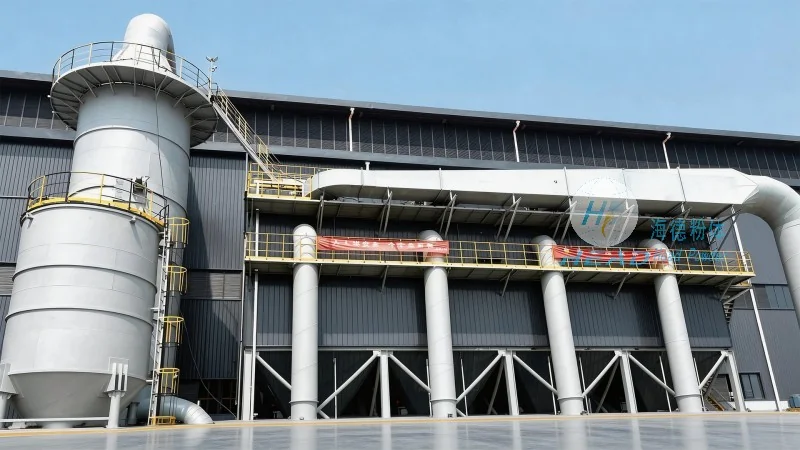
The primary principle of pneumatic conveying involves using air or gas to transport bulk materials through a pipeline system. Unlike traditional mechanical conveyors, which rely on physical components like belts or buckets, pneumatic systems utilize pressure differentials to move materials. There are two main types of pneumatic conveying: pressure and vacuum systems. Pressure systems operate by forcing air and material through a sealed pipeline, typically using positive pressure from a blower or compressor. Vacuum systems, on the other hand, create a negative pressure environment that draws material into the pipeline from a hopper or storage bin. Both methods are widely used in grain silos, with the choice depending on factors such as material characteristics, distance, and system complexity.
Key Working Scene Characteristics
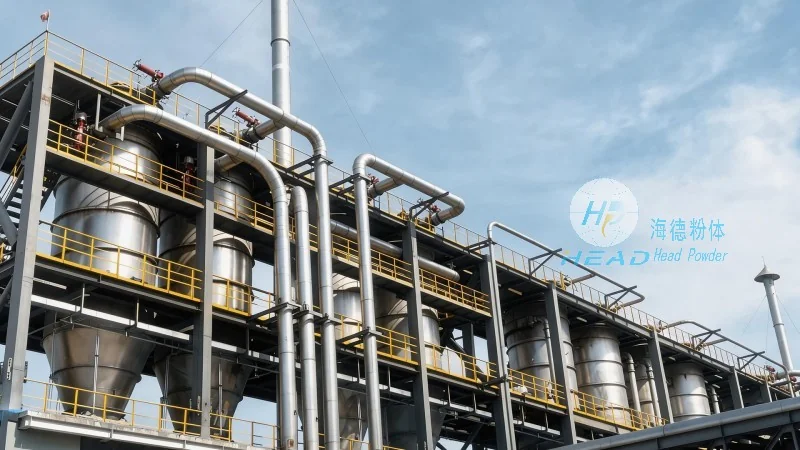
The application of pneumatic conveying equipment in grain silos is characterized by several distinct features that enhance operational efficiency and material handling capabilities. First, these systems are designed to handle large volumes of bulk materials with minimal labor requirements. The automated nature of pneumatic conveyors reduces the need for manual loading and unloading, which is particularly beneficial in large-scale grain storage operations. Second, the equipment is built to withstand the abrasive nature of agricultural products, ensuring long-term durability and low maintenance costs. This is achieved through the use of high-quality materials, such as stainless steel and corrosion-resistant components, which are standard in HeadPowder's product line.
Operational Scenarios in Grain Storage Facilities
Pneumatic conveying systems are employed in various operational scenarios within grain silos, each tailored to specific needs. One common application is the transfer of grain from storage bins to processing units, such as mills or elevators. This process involves moving material from the top of the silo to lower-level processing areas, often over considerable distances. Another scenario is the loading and unloading of trucks or railcars, where the equipment can efficiently transfer grain from the silo to transportation vehicles. Additionally, pneumatic conveyors are used for blending different grain varieties or for transferring materials between multiple silos, enabling precise inventory management and quality control.
Advantages of Choosing HeadPowder's Equipment
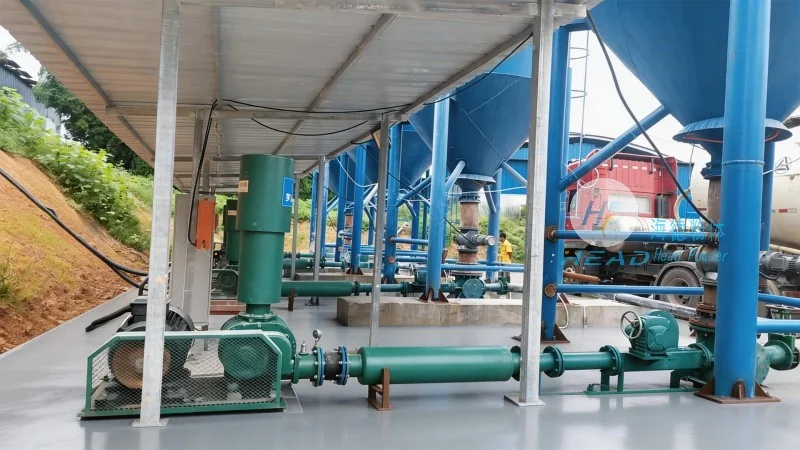
HeadPowder Engineering Co., Ltd. offers a range of pneumatic conveying solutions that address the unique challenges of grain silo operations. The company's products are engineered to provide high efficiency, reliability, and durability, ensuring consistent performance in demanding environments. Key advantages include: efficient material transfer with minimal product degradation, reduced labor costs through automation, and flexible system designs that can be customized to meet specific operational requirements. Furthermore, HeadPowder's equipment is designed with safety and compliance in mind, adhering to industry standards and regulations for grain handling.




