Sugar processing facilities often require efficient and hygienic material handling solutions to ensure smooth production operations. Pneumatic conveying systems have emerged as a preferred choice for transporting bulk materials like sugar, offering advantages such as reduced contamination risk, improved process control, and enhanced safety. This article provides an overview of sugar pneumatic conveying equipment, detailing its structural components, working principles, and key features designed specifically for the sugar industry.
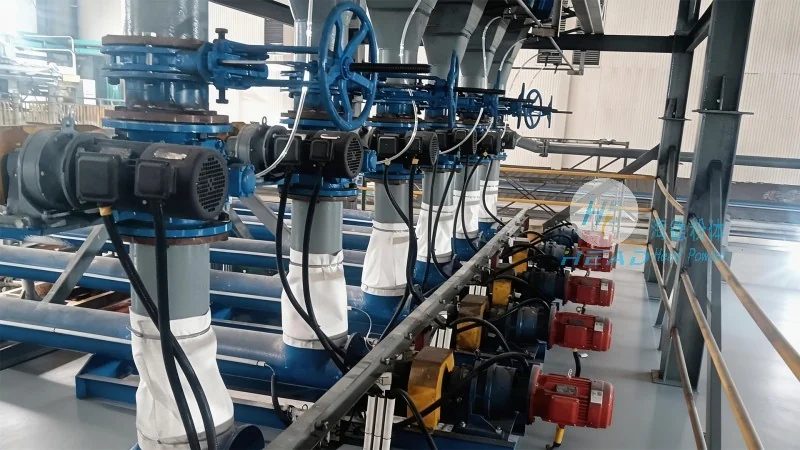
Overview of Sugar Pneumatic Conveying Equipment
Sugar pneumatic conveying equipment is engineered to transport granular or powdered sugar from one location to another within a processing plant using compressed air or other gases. Unlike traditional mechanical conveyors, these systems utilize air flow to move the material, minimizing physical contact and preserving product quality. The equipment is typically composed of several key components, including a hopper, feeder, airlock, conveying line, and receiver, each playing a critical role in the overall operation.
Structural Components and Working Principle of the Equipment
The structural design of sugar pneumatic conveying equipment is tailored to meet the unique demands of the sugar industry, focusing on hygiene, durability, and operational efficiency. The primary components include:
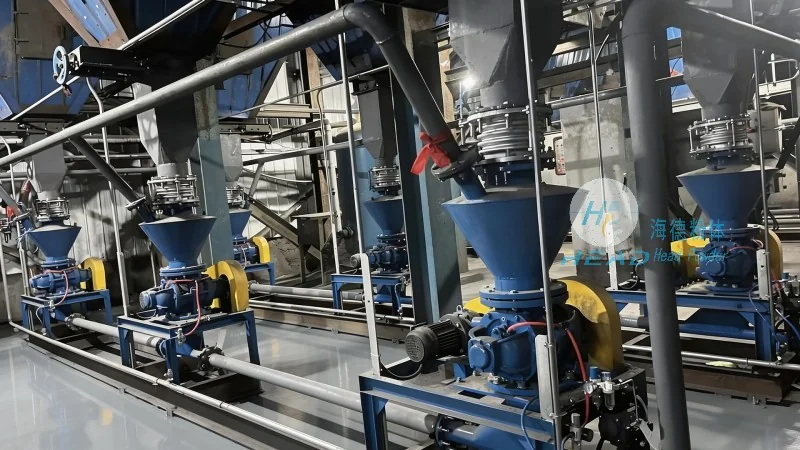
- Hopper: A storage container that holds the raw sugar before it is fed into the system. It is designed with smooth, easy-to-clean surfaces to prevent product buildup and contamination.
- Feeder: A device that controls the flow rate of sugar from the hopper into the conveying line. Common types include rotary valves and screw feeders, which ensure consistent and controlled material discharge.
- Airlock: A sealed chamber that connects the feeder to the conveying line, preventing air leakage and ensuring that only the required amount of sugar is fed into the system. This component is crucial for maintaining pressure and preventing product spillage.
- Conveying Line: The main pipeline through which compressed air and sugar particles are transported. The line is typically made of stainless steel or other corrosion-resistant materials to withstand the acidic and humid conditions often encountered in sugar processing.
- Receiver: A container that collects the sugar at the destination point, such as a storage silo or processing unit. It is equipped with a discharge valve to regulate the outflow of the material.
The working principle of the equipment involves creating a pressure differential between the hopper and the receiver. Compressed air is introduced into the conveying line, generating a flow that lifts and transports the sugar particles. The air-sugar mixture travels through the line under positive or negative pressure, depending on the system design. As the mixture reaches the receiver, the air is separated from the sugar, either through a cyclone separator or a filter, and the sugar is collected in the receiver.
Key Features and Advantages for Sugar Handling
Sugar pneumatic conveying equipment offers several advantages that make it ideal for sugar processing applications:
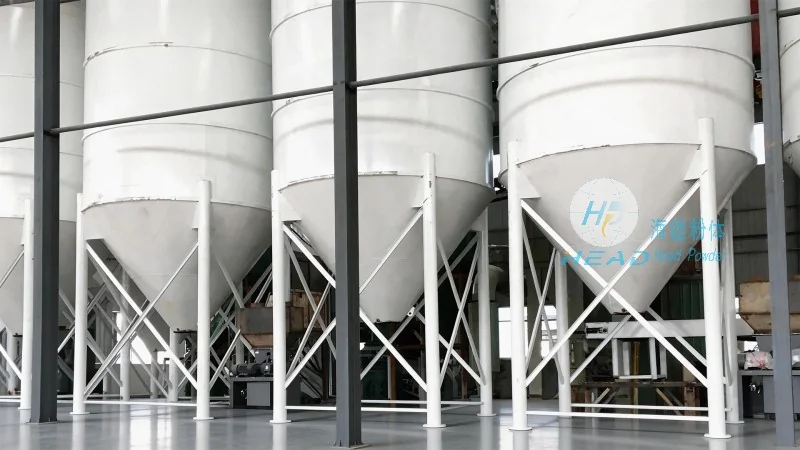
- Hygienic and Clean Operation: The enclosed system minimizes exposure to contaminants, ensuring that the sugar remains free from dust, moisture, or foreign particles. This is particularly important in food processing, where product purity is a top priority.
- Reduced Product Loss and Waste: The precise control of material flow reduces spillage and waste, leading to cost savings and improved efficiency.
- Energy Efficiency: Modern pneumatic conveying systems are designed to optimize air usage, reducing energy consumption compared to traditional mechanical conveyors.
- Flexibility in Layout: The equipment can be easily integrated into existing plant layouts, allowing for flexible placement of hoppers, feeders, and receivers to accommodate different production requirements.
- Low Maintenance: The components are designed for durability and ease of maintenance, with minimal moving parts that require regular servicing.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of pneumatic conveying equipment for the food and chemical industries. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's expertise lies in designing customized systems that meet the specific needs of clients, ensuring optimal performance and durability.
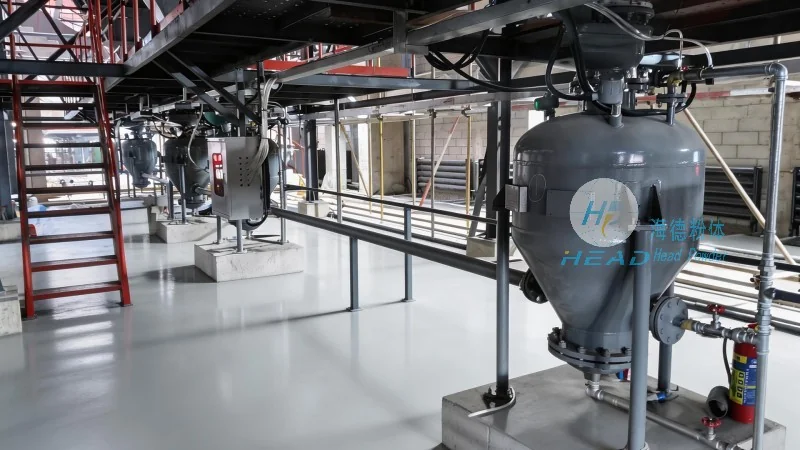
Technical Specifications and Application Scenarios
HeadPowder's sugar pneumatic conveying equipment is available in various configurations to suit different production capacities and operational requirements. The systems can handle a wide range of sugar types, including granulated, powdered, and crystalline forms, with capacities ranging from small-scale laboratory applications to large industrial processing plants. Typical applications include transporting sugar from storage silos to processing lines, moving sugar between different stages of production, and delivering sugar to packaging units. The equipment is also suitable for use in environments where space is limited or where traditional conveyors may not be feasible.
In conclusion, sugar pneumatic conveying equipment offers a superior solution for efficient and hygienic sugar handling in processing facilities. With its advanced structural design and working principles, the equipment ensures consistent performance, minimal product loss, and enhanced operational safety. As a leading provider in the industry, Shandong HeadPowder Engineering Co., Ltd. continues to deliver high-quality, customized solutions that meet the evolving needs of the sugar industry, supporting businesses in achieving their production goals while maintaining the highest standards of product quality and safety.




