Phosphate calcium pneumatic conveying equipment is a specialized system designed for the efficient and safe transportation of phosphate calcium materials in industrial settings. This equipment plays a crucial role in various industries, including chemical processing, mining, and food production, where the handling of bulk materials requires precision and reliability. The system typically operates by using air or other gases to transport the material through a pipeline network, eliminating the need for traditional mechanical conveyors that may cause material degradation or contamination.
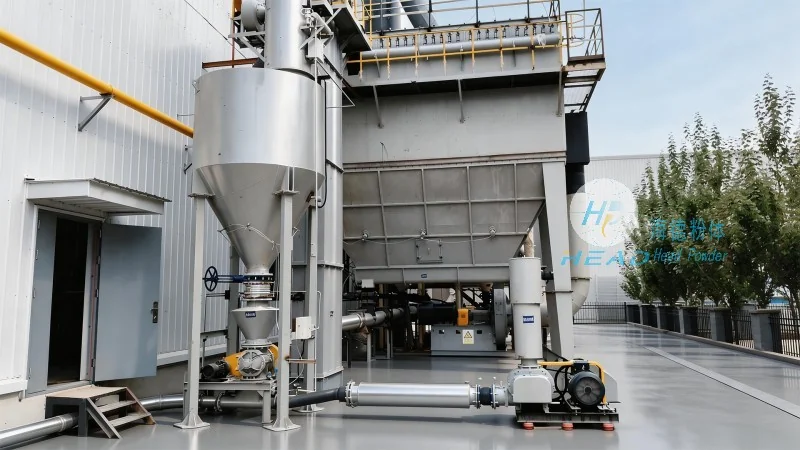
HeadPowder: Specializing in Phosphate Calcium Pneumatic Conveying Solutions
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design, manufacturing, and integration of advanced pneumatic conveying solutions tailored to the unique needs of phosphate calcium applications. Our expertise lies in understanding the specific properties of phosphate calcium, such as its particle size, moisture content, and flow characteristics, to develop optimal conveying systems that ensure minimal product loss and maximum operational efficiency. The company, commonly known as HeadPowder, has established itself as a leading provider of customized pneumatic conveying equipment, serving clients across China and beyond.
The Core Design Principles of Phosphate Calcium Pneumatic Conveying
The core design principle of phosphate calcium pneumatic conveying equipment revolves around the balance between air velocity and material flow. The system uses a combination of positive and negative pressure or vacuum to move the material through the pipeline. In positive pressure systems, compressed air is introduced at the material inlet, creating a pressure differential that propels the material forward. Negative pressure systems, on the other hand, use a vacuum at the discharge end to draw the material through the line. The choice between these systems depends on factors like the distance to be covered, the material's density, and the required throughput. A well-designed system ensures that the air velocity is sufficient to keep the material suspended without causing excessive wear on the equipment or the pipeline.
Key Components and Their Functions
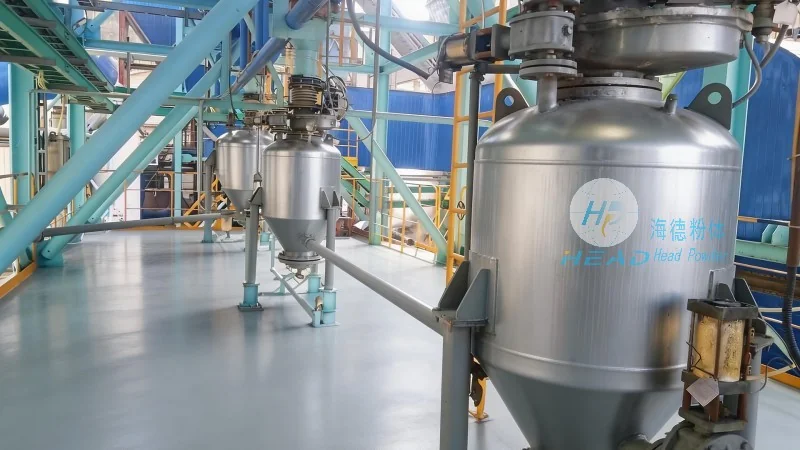
Key components of a phosphate calcium pneumatic conveying system include the material feed hopper, the air compressor or vacuum pump, the conveying pipeline, and the discharge unit. The feed hopper is designed to handle the bulk storage and controlled release of phosphate calcium, preventing material bridging and ensuring a consistent flow rate. The air compressor or vacuum pump provides the necessary pressure or vacuum to move the material through the pipeline. The pipeline is typically made of corrosion-resistant materials, such as stainless steel or special alloys, to withstand the chemical properties of phosphate calcium and prevent degradation over time. The discharge unit, often equipped with a filter or separator, ensures that the material is delivered to the destination without any air or dust contamination.
Optimizing Air Velocity and System Performance
One of the critical aspects of the design is the selection of the appropriate air velocity. The velocity must be high enough to keep the material particles suspended in the air stream but low enough to avoid excessive energy consumption and wear on the system components. This balance is achieved through careful calculation of the material's terminal velocity and the required conveying distance. The system also incorporates features like flow meters and pressure sensors to monitor the conveying process in real-time, allowing for adjustments to maintain optimal performance. These monitoring systems help in detecting any blockages or changes in material flow, ensuring that the operation remains efficient and safe.
Preventing Material Degradation and Contamination
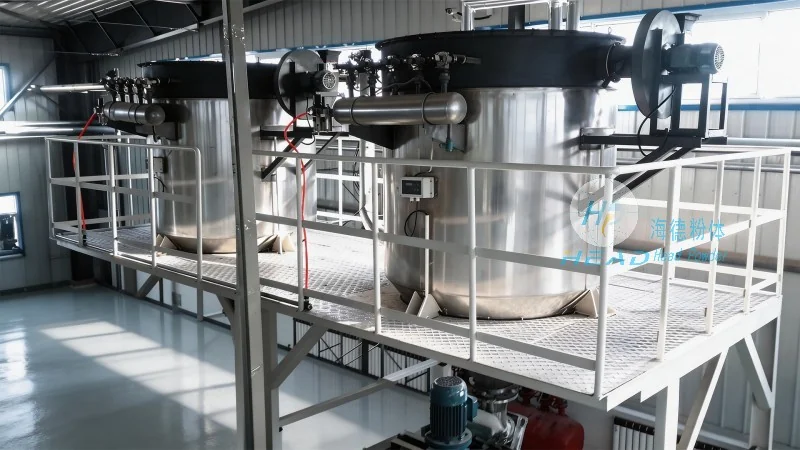
Another important consideration in the design is the prevention of material degradation. Phosphate calcium can be sensitive to moisture and temperature changes, which may affect its quality and usability. The conveying equipment is designed to minimize exposure to these factors by maintaining a controlled environment within the pipeline. For instance, the use of insulated pipelines can help regulate the temperature, while the incorporation of moisture control systems can prevent the material from becoming too wet during transport. These measures are essential for industries where the quality of the phosphate calcium is critical, such as in the production of fertilizers or food additives.
Customized Solutions from HeadPowder
HeadPowder's approach to designing phosphate calcium pneumatic conveying equipment involves a comprehensive understanding of the client's operational requirements. We work closely with clients to assess their specific needs, including the volume of material to be conveyed, the distance between the source and destination, and any regulatory or environmental constraints. Based on this assessment, our engineers develop a customized solution that meets all the technical and operational standards. The company's commitment to quality is evident in its adherence to international standards and the use of advanced manufacturing techniques to ensure the durability and reliability of the equipment.
Installation and Maintenance Support
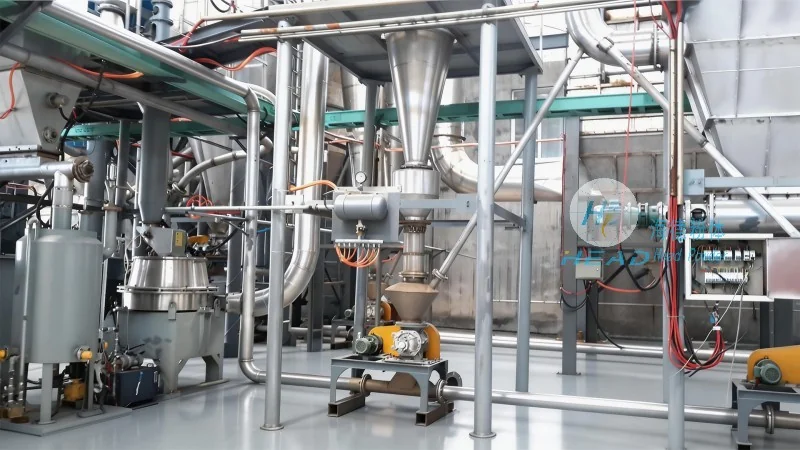
The installation and maintenance of phosphate calcium pneumatic conveying systems require specialized knowledge and expertise. HeadPowder provides comprehensive support to its clients, including on-site installation, commissioning, and regular maintenance services. Our team of experienced technicians is trained to handle the unique challenges associated with phosphate calcium materials, ensuring that the system operates at peak performance throughout its lifespan. Regular maintenance, such as cleaning the pipeline and replacing worn components, is essential to prevent downtime and extend the equipment's service life. By offering these services, HeadPowder ensures that its clients can rely on their conveying systems for consistent and efficient material handling.
Conclusion: Reliable and Efficient Phosphate Calcium Conveying
In conclusion, phosphate calcium pneumatic conveying equipment is a sophisticated solution for the efficient transportation of bulk materials. The design principles, which focus on balancing air velocity, material flow, and system durability, are crucial for ensuring optimal performance. At Shandong HeadPowder Engineering Co., Ltd., we specialize in providing tailored pneumatic conveying solutions that meet the specific needs of phosphate calcium applications. Our commitment to quality, customization, and customer support makes us a trusted partner for industries relying on reliable and efficient material handling systems.




