Multi-hopper powder conveying systems represent a sophisticated approach to handling and transporting bulk powders efficiently. At the core of this technology lies the multi-hopper pump, a device engineered to manage the flow of various powder materials through pneumatic conveying methods. Understanding what multi-hopper powder conveying is and its underlying design principles is crucial for industries that rely on consistent and reliable material transport, such as pharmaceuticals, food processing, and chemical manufacturing.
Defining Multi-Hopper Powder Conveying
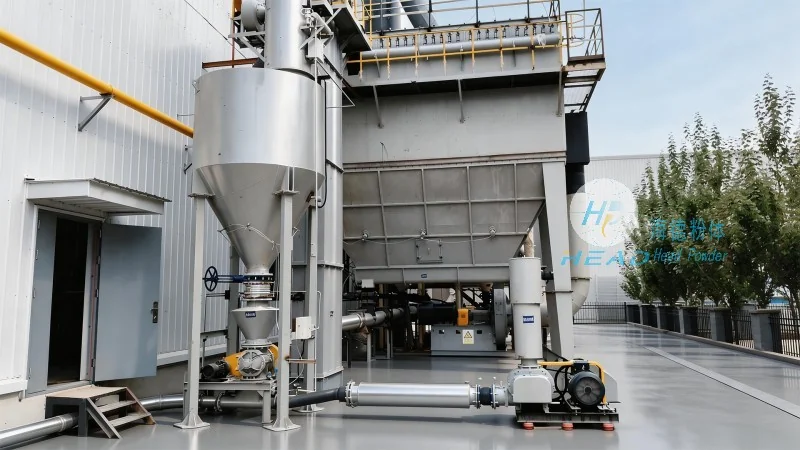
Multi-hopper powder conveying, often referred to as multi-hopper pneumatic conveying, is a system that utilizes multiple hoppers to store and feed different powder types into a single conveying line. This configuration allows for the simultaneous or sequential transport of multiple powders, enhancing operational flexibility and efficiency. The system typically includes a series of hoppers, each dedicated to a specific powder, connected to a central conveying pipeline. As material is drawn from each hopper, it is mixed with an air stream, creating a slurry that travels through the pipeline to the destination point, such as a silo, storage tank, or processing unit.
The Role of Multi-Hopper Pumps in the System
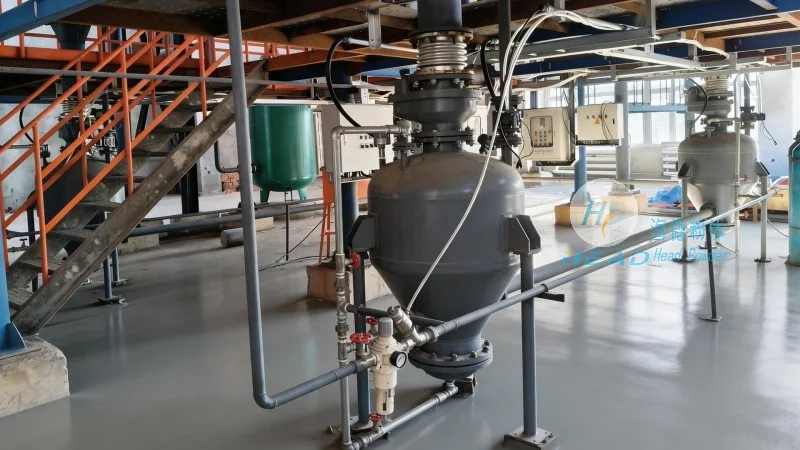
At the heart of the multi-hopper powder conveying system is the multi-hopper pump, which serves as the primary mechanism for material transport. This pump is designed to handle the varying characteristics of different powders, including differences in density, flowability, and moisture content. The pump operates by creating a vacuum or pressure differential within the conveying line, drawing the powder-air mixture from the hoppers and propelling it through the system. The design of the pump, including its internal components like the impeller and housing, is critical to ensuring smooth and consistent material flow, minimizing blockages and ensuring that each powder type is conveyed without degradation or contamination.
Key Design Principles for Efficient Operation
Several key design principles underpin the effectiveness of multi-hopper powder conveying systems. First, the system must be tailored to the specific properties of the powders being transported, such as particle size distribution, bulk density, and cohesive behavior. This involves selecting appropriate hopper designs—often with conical or wedge-shaped bottoms—to promote uniform flow and prevent material bridging or arching. Second, the air-to-powder ratio is a critical parameter that must be optimized to ensure efficient transport while minimizing energy consumption. The ratio is determined by factors like powder characteristics, pipeline length, and system pressure, and is typically adjusted through control valves and pressure sensors. Third, the system incorporates safety features to prevent over-pressurization or vacuum issues, including pressure relief valves and vacuum breakers, which protect both the equipment and the material from damage.
Advantages of Multi-Hopper Powder Conveying
Implementing a multi-hopper powder conveying system offers several advantages for industrial applications. One of the most significant benefits is the ability to handle multiple powder types simultaneously, reducing the need for separate conveying lines and equipment. This leads to cost savings in terms of capital investment and operational space. Additionally, the system provides greater flexibility in production scheduling, as different powders can be added or removed from the process without disrupting the entire operation. Another key advantage is improved material handling efficiency, as the system can maintain consistent flow rates and minimize downtime caused by material blockages or equipment failures. The use of pneumatic conveying also reduces the risk of product contamination compared to mechanical systems, which is particularly important in industries like pharmaceuticals and food processing where product purity is paramount.
Applications in Various Industries
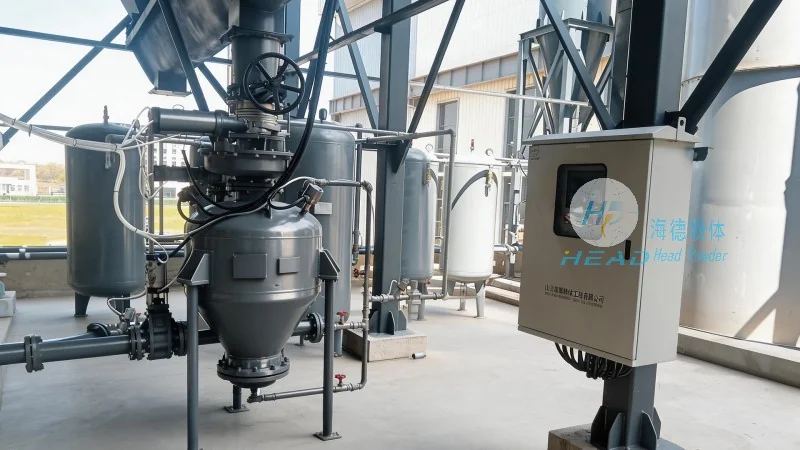
Multi-hopper powder conveying systems are widely used across a range of industries due to their adaptability and efficiency. In the pharmaceutical industry, these systems are employed to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that each batch is handled under controlled conditions to maintain product quality and safety. In the food processing sector, the technology is used to convey ingredients like flour, sugar, and spices, where hygiene and product integrity are critical. The chemical industry also benefits from multi-hopper systems when handling powders such as catalysts, pigments, and specialty chemicals, which may have varying flow properties and require careful handling to avoid degradation. Overall, the versatility of multi-hopper powder conveying makes it an essential tool for industries that demand reliable, clean, and efficient material transport solutions.
Conclusion
Multi-hopper powder conveying represents a sophisticated and efficient method for handling and transporting bulk powders. By integrating multiple hoppers with a central conveying system and a multi-hopper pump, this technology enables industries to manage diverse powder materials with precision and reliability. The design principles, including tailored hopper configurations, optimized air-to-powder ratios, and robust safety features, ensure that the system operates efficiently and safely. As a result, multi-hopper powder conveying systems are increasingly adopted across various sectors, contributing to improved operational efficiency, cost savings, and product quality. For companies seeking to enhance their material handling capabilities, understanding the design and benefits of such systems is essential for making informed decisions about equipment selection and process optimization.




