Tonne bag automatic feeding material handling systems are advanced industrial solutions designed to efficiently and safely transfer bulk materials from large tonne bags into processing equipment. These systems are widely used in various industries, including chemical, food, pharmaceutical, and mining, where handling large volumes of powders or granules is essential for production processes. The primary function of such systems is to automate the material transfer process, reducing manual labor, minimizing material loss, and enhancing overall operational efficiency.
Key Components of the System
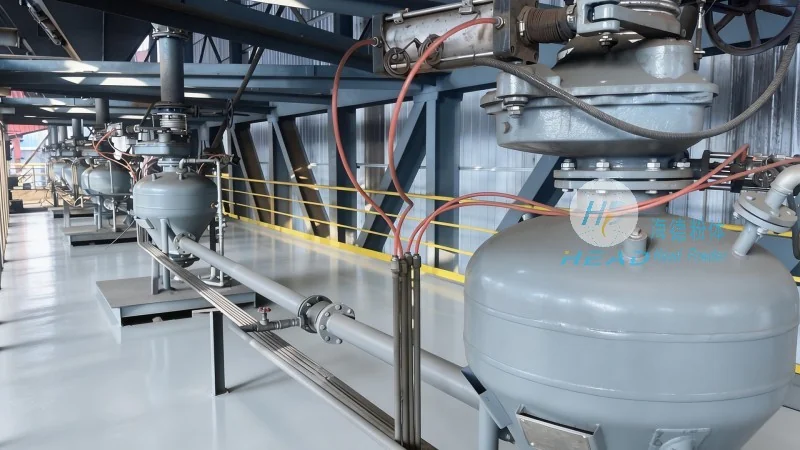
The tonne bag automatic feeding system typically consists of several critical components that work in tandem to ensure smooth operation. The main components include a tonne bag discharging unit, a conveyor system, a feeding hopper, a control panel, and sometimes a dust collection system. Each component plays a vital role in the overall functionality of the system.
The tonne bag discharging unit is responsible for opening the top of the tonne bag and allowing the material to flow out. This unit may use a mechanical or pneumatic mechanism to cut or tear the bag open and then release the contents. The conveyor system, often a screw conveyor or a belt conveyor, transports the material from the discharging unit to the feeding hopper. The feeding hopper acts as a buffer, storing the material before it is fed into the processing equipment. The control panel allows operators to monitor and control the system's operations, ensuring safe and efficient material transfer. In some cases, a dust collection system is integrated to manage dust emissions and maintain a clean working environment.
Design Principles and Operational Mechanisms
The design principles of a tonne bag automatic feeding system are centered on safety, efficiency, and reliability. The system is engineered to handle a wide range of materials, from fine powders to coarse granules, with minimal degradation or contamination. The key design considerations include material flow control, dust suppression, and system integration with existing production lines.
Material flow control is achieved through the use of adjustable valves, gates, and conveyor speeds. This allows operators to regulate the flow rate of the material, preventing overloading of the processing equipment and ensuring consistent feed rates. Dust suppression is a critical aspect of the design, as many bulk materials are prone to generating dust during handling. The system incorporates features such as sealed containers, dust collection hoods, and filtration systems to minimize dust emissions and protect both the material and the environment.
System integration is another important design principle. The tonne bag automatic feeding system is designed to be compatible with existing production lines, allowing for seamless integration without major modifications. This ensures that the system can be easily incorporated into current operations, reducing downtime and increasing productivity. The control panel provides real-time monitoring of system parameters, such as material level, conveyor speed, and pressure, enabling operators to quickly identify and address any issues that may arise.
Advantages of Using a Tonne Bag Automatic Feeding System
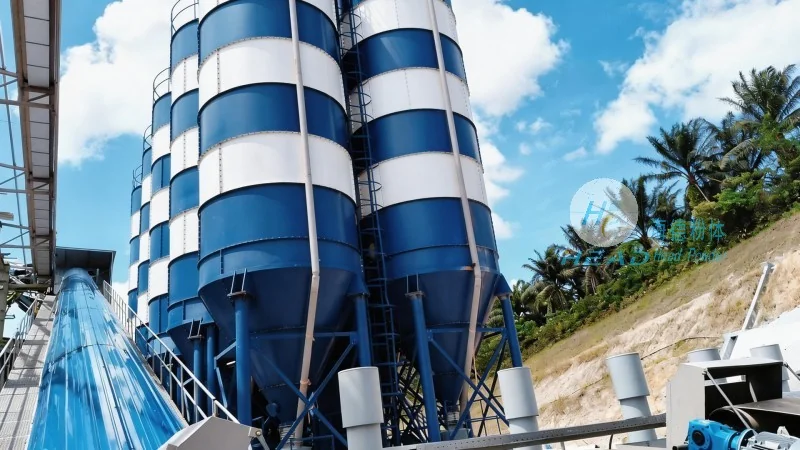
Implementing a tonne bag automatic feeding material handling system offers numerous advantages for industrial operations. One of the primary benefits is the significant reduction in manual labor. Traditional methods of handling tonne bags often require workers to manually open the bags and pour the material, which is not only labor-intensive but also poses safety risks. The automated system eliminates the need for manual handling, reducing the risk of injuries and improving workplace safety.
Another key advantage is the reduction in material loss. Manual handling of bulk materials can lead to spillage and loss of product, which not only results in financial losses but also creates environmental hazards. The automated system minimizes material loss by ensuring a controlled and efficient flow of material from the tonne bag to the processing equipment. This results in higher material recovery rates and lower waste generation.
Operational efficiency is also greatly enhanced with an automated feeding system. The system can operate continuously, 24/7, without the need for breaks or rest periods, unlike manual labor. This leads to increased production throughput and reduced downtime. Additionally, the system's ability to maintain consistent feed rates ensures that the processing equipment operates at optimal levels, improving overall production quality and reducing the risk of equipment damage due to overloading or underfeeding.
Cost savings are another significant benefit of using a tonne bag automatic feeding system. While the initial investment may be higher than traditional manual methods, the long-term savings in labor costs, material loss, and equipment maintenance make it a cost-effective solution. The system also reduces the need for frequent cleaning and maintenance of the processing equipment due to reduced dust and spillage, further contributing to cost savings.
Application Examples and Industry Use Cases
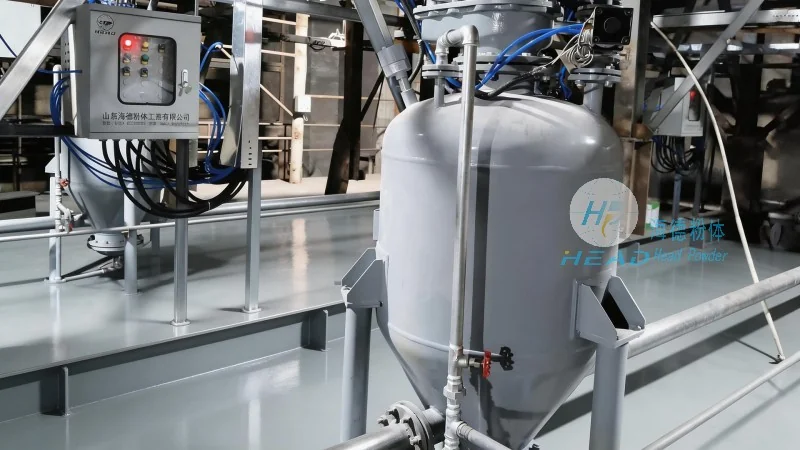
Tonne bag automatic feeding material handling systems are used in a wide range of industries and applications. In the chemical industry, these systems are commonly used to handle raw materials such as powders and granules for chemical synthesis. The systems ensure that the materials are transferred safely and efficiently, minimizing the risk of contamination and ensuring consistent feed rates for chemical reactions.
In the food and pharmaceutical industries, the systems are used to handle food ingredients and pharmaceutical raw materials. The design of the system, with its emphasis on hygiene and dust control, makes it suitable for these industries, where product purity and safety are paramount. The automated feeding system reduces the risk of cross-contamination and ensures that the materials are handled in a clean and controlled environment.
In the mining and mineral processing industry, tonne bag automatic feeding systems are used to handle mined materials such as ores and minerals. The systems are designed to handle large volumes of coarse materials and can be integrated with crushing and grinding equipment to form a complete material handling line. The efficiency and reliability of the system help to improve the overall productivity of mining operations.
Conclusion and Company Overview
Tonne bag automatic feeding material handling systems are essential tools for modern industrial operations, providing efficient, safe, and reliable material transfer solutions. The design principles and operational mechanisms of these systems are carefully engineered to meet the demands of various industries, ensuring optimal performance and minimal downtime.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of material handling equipment, specializes in designing and manufacturing tonne bag automatic feeding systems tailored to the specific needs of different industries. With a focus on quality, safety, and efficiency, the company provides comprehensive solutions that enhance operational productivity and reduce costs. HeadPowder's systems are known for their durability, reliability, and ease of maintenance, making them a preferred choice for industrial applications worldwide.




