Pharmaceutical material handling systems are critical components in modern drug manufacturing facilities, facilitating the efficient and safe movement of raw materials, intermediates, and finished products throughout the production process. These systems are designed to meet stringent regulatory requirements, ensuring product quality, safety, and compliance with Good Manufacturing Practices (GMP). The design principles behind these systems are multifaceted, integrating automation, precision, and adaptability to meet the unique needs of pharmaceutical operations.
Key Design Principles for Pharmaceutical Material Handling Systems
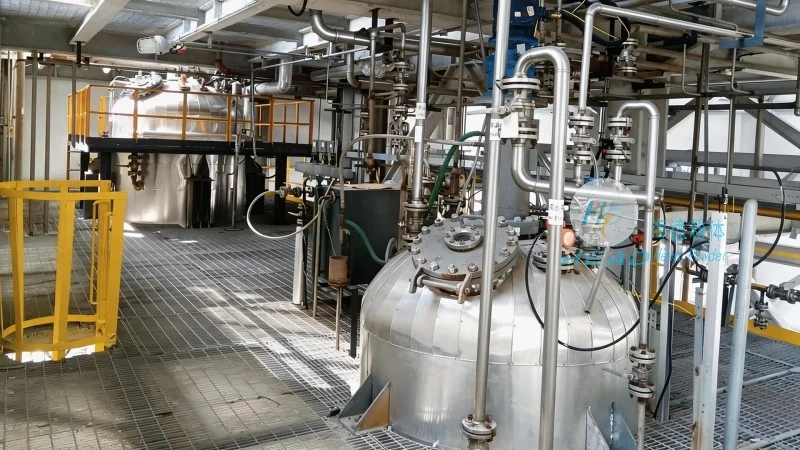
The design of a pharmaceutical material handling system is guided by several core principles that prioritize operational efficiency, product integrity, and regulatory adherence. First, modularity is a fundamental design principle, allowing systems to be scaled or reconfigured as production needs evolve. Modular components, such as conveyors, storage units, and processing stations, can be easily integrated or replaced, reducing downtime and enhancing flexibility. Second, sterility and contamination control are paramount in pharmaceutical manufacturing. Systems are typically constructed from materials like stainless steel, which resist corrosion and are easy to clean, and are equipped with sealed joints and air filtration systems to maintain a sterile environment. Third, automation and control are integrated to minimize human intervention, reducing the risk of errors and ensuring consistent performance. Advanced control systems, often linked to enterprise resource planning (ERP) software, enable real-time monitoring and data tracking, supporting traceability and quality management. Fourth, ergonomics and safety are critical considerations. Systems are designed to minimize operator exposure to hazardous materials and to comply with occupational safety standards, incorporating features like interlocks, emergency stop buttons, and ergonomic workstations.
Role of HeadPowder in Pharmaceutical Material Handling Solutions
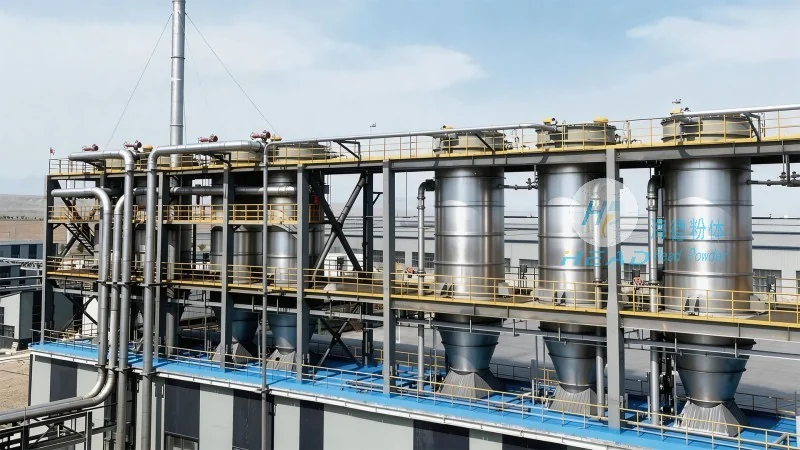
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in providing comprehensive pharmaceutical material handling solutions tailored to the specific requirements of the pharmaceutical industry. With a focus on innovation and adherence to industry standards, HeadPowder designs and manufactures systems that align with the core design principles outlined above. The company’s approach emphasizes customization, ensuring that each system is optimized for the client’s production processes, product types, and facility layout. For instance, HeadPowder may incorporate advanced automation technologies, such as robotic handling and intelligent conveyor systems, to enhance efficiency and reduce labor costs. Additionally, the company adheres to GMP guidelines, ensuring that all components and processes are validated and documented to meet regulatory expectations. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-quality solutions to clients worldwide.
Conclusion: The Importance of Well-Designed Material Handling Systems in Pharmaceutical Manufacturing
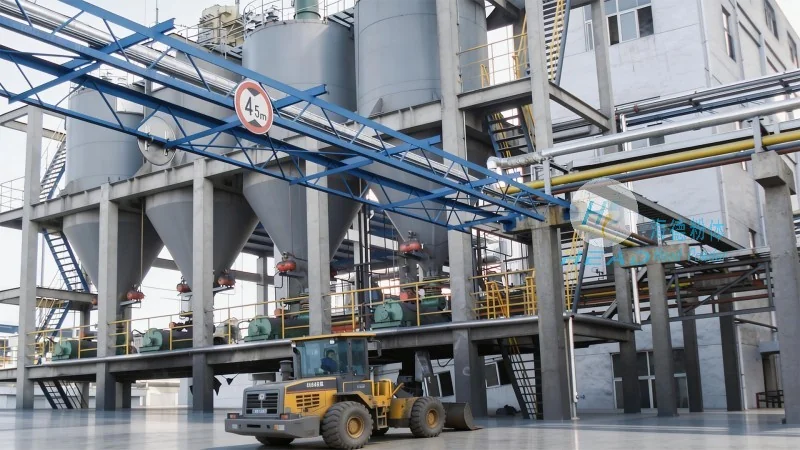
In conclusion, pharmaceutical material handling systems are essential for maintaining the integrity and efficiency of drug manufacturing operations. The design principles of modularity, sterility, automation, and safety are critical to ensuring that these systems meet the demanding requirements of the pharmaceutical industry. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing tailored solutions that incorporate these principles, helping pharmaceutical manufacturers achieve operational excellence and regulatory compliance. By investing in well-designed material handling systems, pharmaceutical companies can enhance productivity, reduce costs, and ensure the consistent quality of their products, ultimately contributing to patient safety and the success of their business.




