Organic fertilizer granule material handling equipment is a specialized system engineered to transport and manage granular organic fertilizers efficiently. This equipment is vital in agricultural and industrial contexts where bulk organic material handling is required. The design principles behind such equipment revolve around ensuring reliable, low-friction, and safe material transport, which are essential for preserving the quality and integrity of the fertilizer granules.
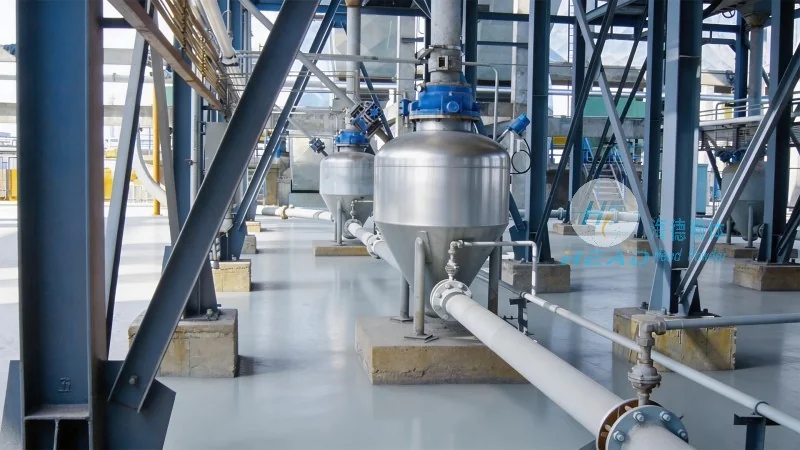
Core Components of Organic Fertilizer Granule Handling Systems
The foundation of organic fertilizer granule material handling equipment consists of several key components that operate in unison. These include feeders, conveyors, and control systems. The feeder uniformly delivers granules into the conveyor system, preventing blockages and ensuring consistent flow. Conveyors—such as belt or screw types—are designed to move granules between locations with minimal breakage. Control systems, often integrated with sensors and automation, monitor flow rate, pressure, and other critical parameters to maintain optimal performance.
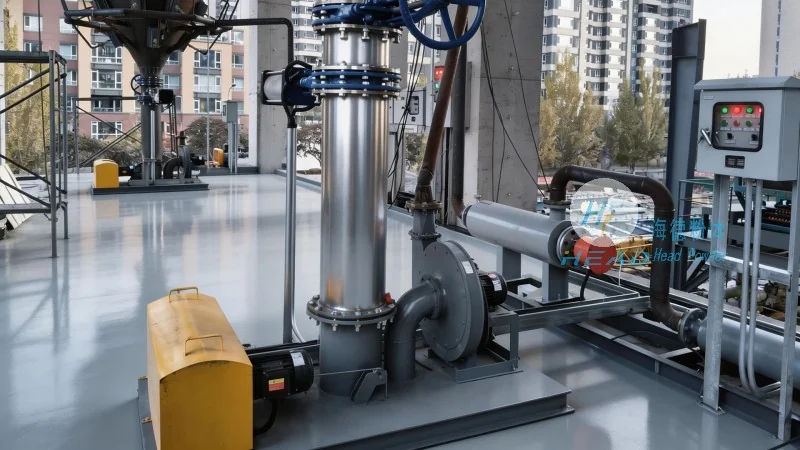
Design Principles for Efficient and Reliable Transport
The design of organic fertilizer granule handling equipment adheres to fundamental principles to achieve efficiency and reliability. A primary principle is minimizing friction and abrasion, as organic granules can be delicate and prone to damage from rough handling. This is accomplished through smooth, non-stick surfaces and appropriate conveyor materials. Another key principle is maintaining consistent flow rates to prevent overloading or underloading, which is critical for avoiding clogs and operational issues. Additionally, the design emphasizes safety, incorporating emergency stop buttons and protective guards to prevent accidents during operation.
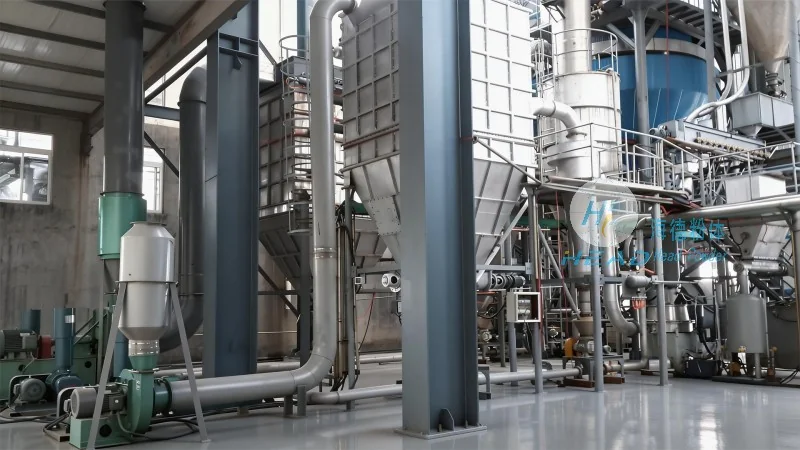
Applications in Industrial and Agricultural Settings
Organic fertilizer granule material handling equipment is widely utilized in both industrial and agricultural environments. In industrial settings, like fertilizer manufacturing plants, these systems transport granules from production lines to storage or packaging areas. The equipment ensures efficient movement without damage, preserving the quality of the final product. In agricultural settings, the equipment is used on farms to move organic fertilizers from storage to application points, such as fields or greenhouses. It is designed to handle the bulk volumes typical of agricultural operations, ensuring uniform and effective fertilizer application.
Key Features and Advantages
Organic fertilizer granule handling equipment offers several advantages that make it a preferred choice for material transport. One major advantage is its ability to handle bulk materials with minimal human intervention, reducing labor costs and increasing operational efficiency. The equipment is also built for durability and long-term use, with components that withstand continuous operation. Advanced control features allow real-time monitoring and adjustment, ensuring optimal performance under varying conditions. The design prioritizes energy efficiency, using less power to move granules compared to traditional methods, which helps reduce operational costs.
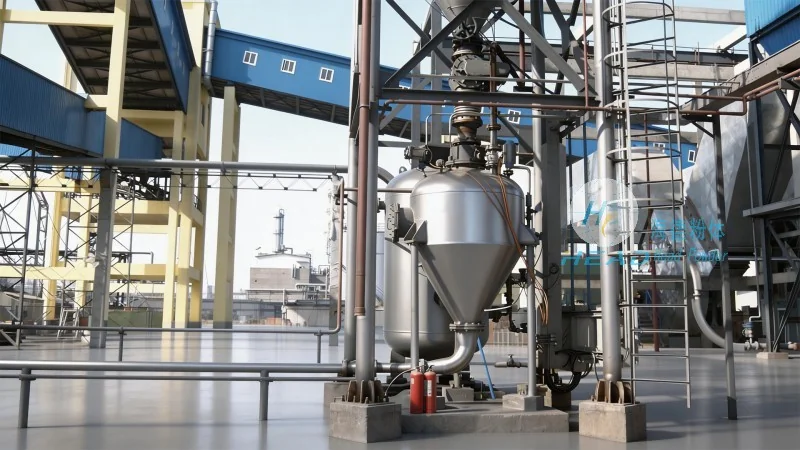
Conclusion: The Importance of Well-Designed Equipment
In summary, organic fertilizer granule material handling equipment is a critical component in agricultural and industrial sectors, playing a vital role in the efficient and safe transport of organic fertilizers. The design principles focus on minimizing friction, maintaining consistent flow, and ensuring safety—all contributing to overall efficiency and reliability. As the demand for organic fertilizers grows, the importance of well-designed material handling equipment will only increase, making it essential for businesses to invest in high-quality systems tailored to their specific needs. HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing such reliable solutions to meet modern industry demands.




