

What is a Dust Material Pneumatic Conveying Machine? And What Are Its Design Principles?
For industries dealing with bulk powder materials, efficient and reliable material handling is crucial. A dust material pneumatic conveying machine, also known as a pneumatic conveyor, is a system designed to transport dry, powdery substances through a pipeline using air or gas as the conveying medium. This technology offers a flexible and effective solution for moving materials like flour, cement, and other fine powders over short to medium distances. The design principles behind these machines are centered on creating a controlled flow of material within the pipeline, ensuring minimal product degradation and operational efficiency.
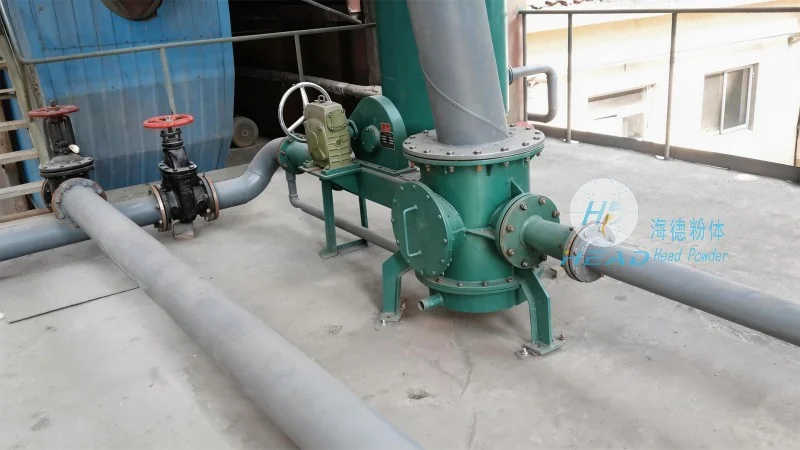
Key Components and Working Principle
The core components of a pneumatic conveying system typically include a hopper for material storage, a feeder to control the flow rate, a conveying line (pipeline), a blower or compressor to generate the air flow, and a receiver for the discharged material. The working principle involves feeding the powder into the hopper, where it is then drawn into the conveying line by the air flow generated by the blower. The air and material mixture travels through the pipeline, with the air pressure maintaining the material in suspension. At the end of the pipeline, the material is separated from the air, often through a cyclone separator or filter, and collected in the receiver. The air is then either recirculated or discharged, depending on the system design. This process allows for continuous, automated material transport without the need for mechanical parts in direct contact with the product, reducing wear and maintenance.
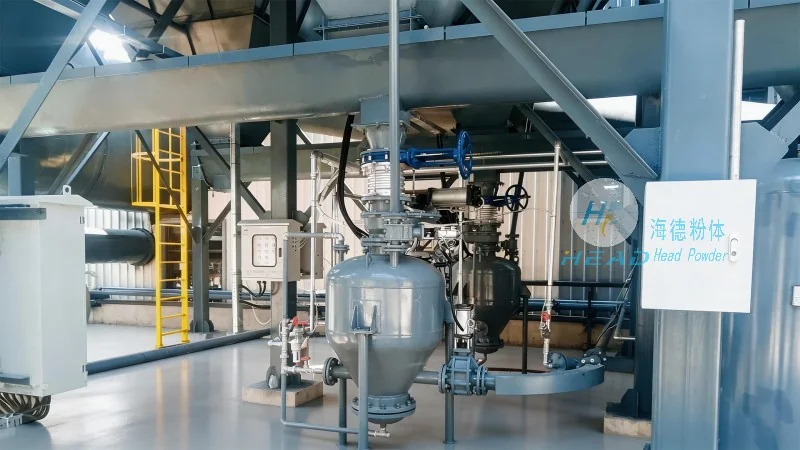
Design Principles for Optimal Performance
The design of a dust material pneumatic conveying machine focuses on several key principles to ensure efficient operation and material integrity. First, the selection of the conveying line diameter and length is critical. The diameter must be large enough to prevent excessive pressure drop and material settling, while the length should be optimized to minimize energy consumption. Second, the air velocity within the pipeline is a key factor. It must be high enough to keep the material in suspension but not so high as to cause excessive wear on the system components or degrade the material. Third, the system's pressure and flow rate are carefully controlled to maintain consistent material transport. This involves matching the blower capacity to the required conveying rate and ensuring the feeder can handle the material without causing blockages. Additionally, the design considers the material's properties, such as particle size, density, and moisture content, as these factors influence the air velocity and pressure required for effective conveying. By adhering to these design principles, the machine can achieve high conveying efficiency, low energy consumption, and minimal product degradation.
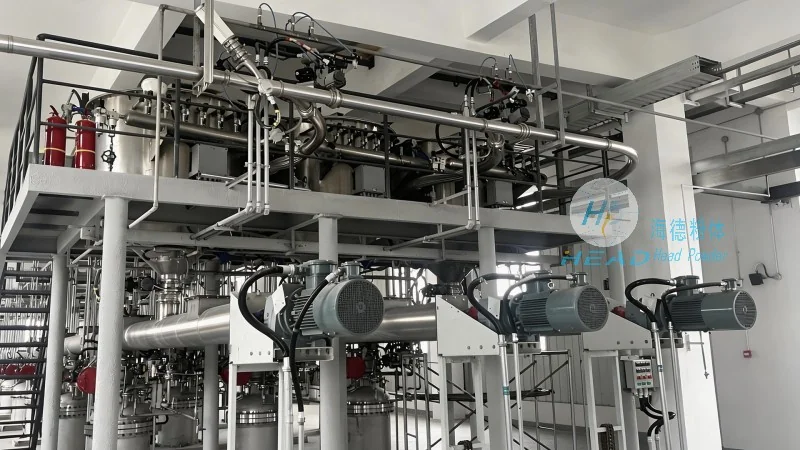
Applications and Benefits
Dust material pneumatic conveying machines are widely used in various industries, including food processing, pharmaceuticals, chemicals, and construction. In the food industry, they are used to transport flour, sugar, and other dry ingredients, ensuring hygienic and dust-free handling. In pharmaceuticals, the system's ability to handle sensitive materials without contamination makes it ideal for transporting powders like active pharmaceutical ingredients (APIs). In the chemical industry, it can transport powders like cement, limestone, and other bulk chemicals, providing a safe and efficient method for material transport. The benefits of using pneumatic conveying systems include reduced labor costs due to automated operation, improved product quality through minimal handling, and enhanced safety by eliminating manual handling of powders. Additionally, the system's flexibility allows for easy integration into existing production lines and can be adapted to different material types and conveying distances.
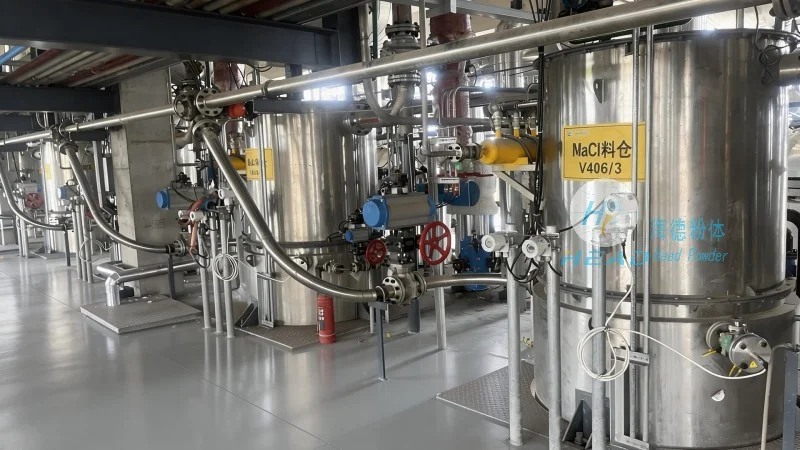
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of pneumatic conveying systems and related equipment. With a focus on innovation and quality, the company provides customized solutions tailored to the specific needs of its clients. HeadPowder's products are designed to meet the highest standards of efficiency, reliability, and safety, ensuring that clients can achieve optimal performance in their material handling operations. The company's expertise in the field, combined with its commitment to customer satisfaction, has made it a trusted partner for businesses across various industries. By leveraging advanced technology and rigorous quality control, HeadPowder delivers pneumatic conveying machines that are built to last and provide long-term value to its customers.