

What is a White Ash Material Pneumatic Conveyor? And What Are Its Design Principles?
White ash material pneumatic conveyors are specialized equipment used for the efficient and safe transportation of white ash materials in industrial settings. These systems are designed to handle the unique properties of white ash, such as its dustiness and potential for reactivity, ensuring reliable operation and minimal environmental impact. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality pneumatic conveyor solutions tailored to the specific needs of various industries.
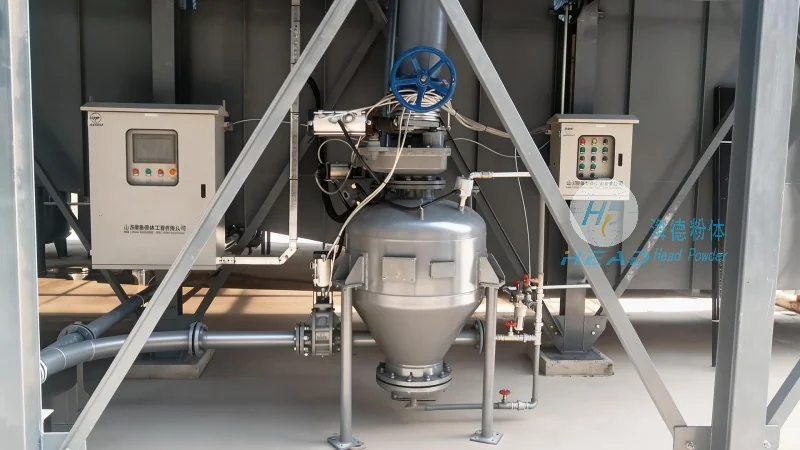
Understanding White Ash Material Pneumatic Conveyors
At the core of a white ash material pneumatic conveyor is the ability to transport dry, powdery materials like white ash through a pipeline using air pressure. This method, known as pneumatic conveying, offers several advantages over traditional mechanical conveyors, including reduced maintenance, lower energy consumption, and the ability to handle materials that are difficult to transport by other means. The system typically consists of a hopper for material storage, a blower or compressor to generate the air flow, a pipeline network to direct the material, and a discharge point where the material is released. The design of the conveyor must account for the specific characteristics of white ash, such as its particle size, moisture content, and flowability, to ensure optimal performance.
Key Design Principles of White Ash Pneumatic Conveyors
The design of a white ash material pneumatic conveyor involves several critical principles to ensure efficiency and reliability. First, the system must be designed to handle the dustiness of white ash, which can lead to clogging and wear if not properly managed. This is often addressed through the use of high-quality materials for the hopper and pipeline, such as stainless steel or special coatings, to prevent material buildup and corrosion. Second, the air flow rate must be carefully controlled to maintain a consistent material velocity, preventing the material from settling or clogging the pipeline. This is achieved through the use of variable speed blowers or pressure regulators that adjust the air flow based on the material load. Third, the system must incorporate features to prevent air leakage and maintain the integrity of the material flow, such as proper sealing of joints and the use of air filters to remove any dust that may escape. Additionally, the design must consider the potential for material reactivity, ensuring that the conveyor is constructed from materials that are compatible with the white ash and do not cause any adverse reactions.
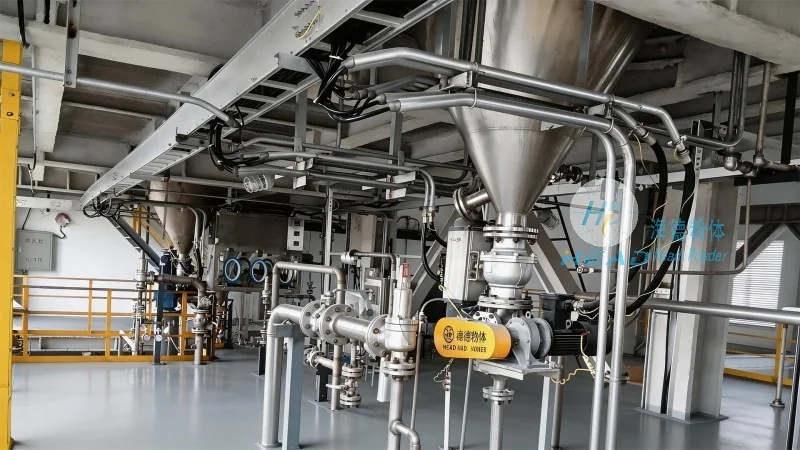
Components and Their Functions in a White Ash Pneumatic Conveyor System
A white ash material pneumatic conveyor consists of several key components, each playing a vital role in the overall operation. The hopper is the primary storage unit, designed to hold the white ash material and feed it into the conveyor system. It is typically equipped with a discharge valve or gate to control the flow of material into the pipeline. The blower or compressor is the power source, generating the air pressure needed to move the material through the pipeline. This component must be capable of providing sufficient air flow and pressure to handle the specific characteristics of white ash, such as its particle size and density. The pipeline network is the main conduit for transporting the material, and it must be designed to withstand the pressure and flow of the air and material. The pipeline is usually made of durable materials like stainless steel or PVC, with smooth interior surfaces to minimize friction and prevent material buildup. The discharge point is where the material is released from the conveyor system, and it is typically equipped with a valve or nozzle to control the flow of material out of the pipeline. Finally, the system may include additional components such as air filters, dust collectors, or vacuum pumps, depending on the specific application and the need to manage dust and air quality.
Advantages of Using White Ash Material Pneumatic Conveyors
White ash material pneumatic conveyors offer several advantages over traditional mechanical conveyors, making them a preferred choice for many industrial applications. One of the main advantages is the ability to handle materials that are difficult to transport by other means, such as white ash, which is often dusty and has a tendency to settle. The pneumatic system allows for the continuous and efficient transportation of these materials, reducing the need for manual handling and improving safety in the workplace. Another advantage is the reduced maintenance requirements, as the system has fewer moving parts compared to mechanical conveyors, resulting in lower downtime and maintenance costs. Additionally, the system is more energy-efficient, as it uses air pressure to move the material rather than mechanical components, which can lead to lower energy consumption and operating costs. The system also offers better control over the material flow, allowing for precise regulation of the material discharge rate and preventing overloading or underloading of the system. Finally, the system is more environmentally friendly, as it reduces the amount of dust and particulate matter released into the air, improving air quality and reducing the risk of environmental contamination.
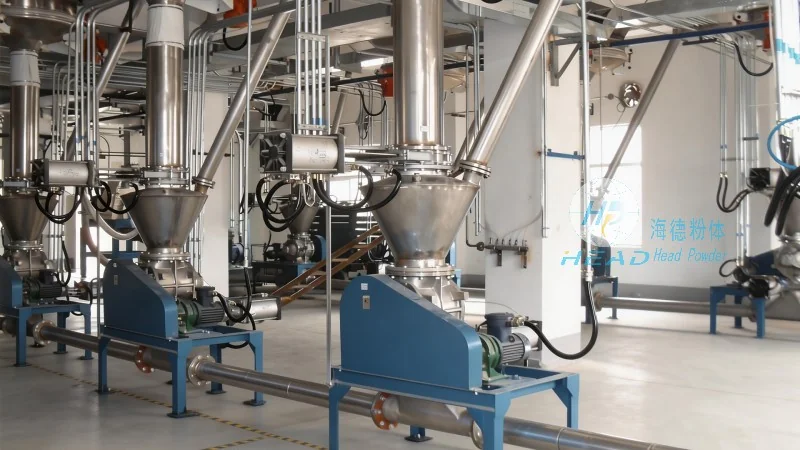
Applications of White Ash Material Pneumatic Conveyors
White ash material pneumatic conveyors are used in a variety of industrial applications where the transportation of white ash is required. These applications include power plants, where white ash is generated as a byproduct of coal combustion, and is transported to storage facilities or disposal sites. The conveyors are also used in cement plants, where white ash is used as a raw material in the production of cement, and is transported from storage to the production line. Additionally, the conveyors are used in construction and building materials industries, where white ash is used as a filler or admixture in concrete and other building materials. The system is also used in the chemical industry, where white ash is used as a raw material in the production of various chemicals, and is transported from storage to the production line. Finally, the conveyors are used in the food and beverage industry, where white ash is used as a natural ingredient in certain products, and is transported from storage to the production line.
Conclusion
In conclusion, white ash material pneumatic conveyors are an essential piece of equipment for the efficient and safe transportation of white ash materials in industrial settings. The design of these systems must account for the unique properties of white ash, such as its dustiness and potential reactivity, to ensure optimal performance and reliability. As a leading manufacturer, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality pneumatic conveyor solutions tailored to the specific needs of various industries. By understanding the key design principles and components of a white ash material pneumatic conveyor, users can make informed decisions about the best system for their application, ensuring efficient and reliable operation.