

Working Principle and Features of Bulk Bag Unloading Station Pneumatic Conveying Equipment
Bulk bag unloading station pneumatic conveying equipment is a specialized system engineered to efficiently transfer bulk materials from bulk bags into processing or storage facilities. This equipment is widely utilized across industries such as chemical, food, pharmaceutical, and construction, where handling large quantities of powders or granules is essential. The system integrates bulk bag handling capabilities with pneumatic conveying technology to ensure a seamless and controlled material transfer process, minimizing downtime and enhancing operational efficiency.
Working Principle of the Pneumatic Conveying System
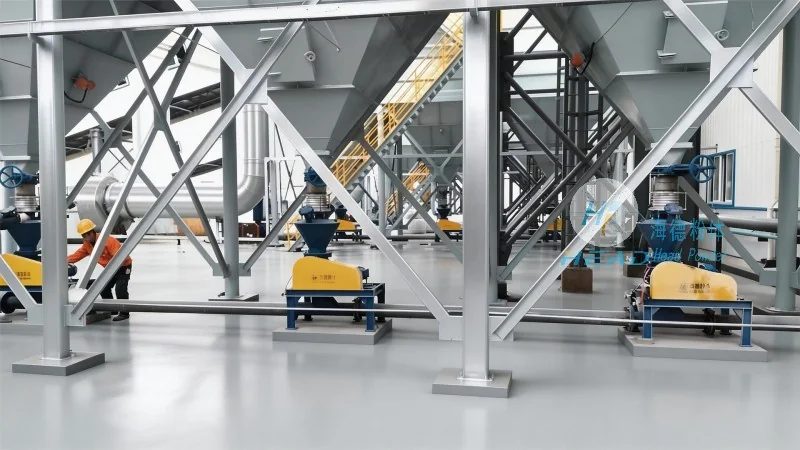
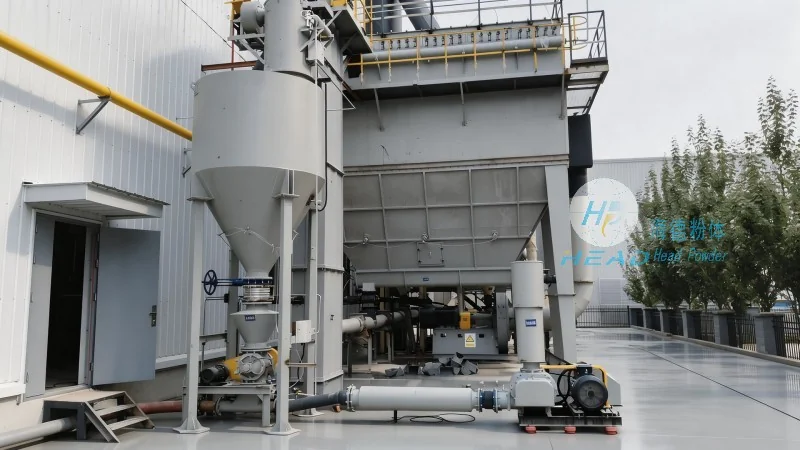
The core of the bulk bag unloading station pneumatic conveying equipment is the pneumatic conveying mechanism, which operates on the principle of air movement to transport materials. The system typically comprises a bulk bag opening device, a hopper for collecting the material, a pneumatic conveyor (either positive or negative pressure), and a discharge valve or outlet. When a bulk bag is positioned in the unloading station, the bag is opened, and the material is discharged into the hopper. Simultaneously, a fan or blower generates airflow, which draws the material from the hopper and conveys it to the desired destination. The positive pressure system employs compressed air to push the material through the pipeline, while the negative pressure system utilizes suction to pull the material. The selection between positive and negative pressure depends on material properties—including dustiness, moisture content, and particle size—as well as the distance and layout of the conveying line. This adaptability ensures optimal performance for diverse material types and operational scenarios.
Key Features and Advantages of the Equipment
The bulk bag unloading station pneumatic conveying equipment offers several key features that enhance operational efficiency and material handling capabilities. One primary advantage is its ability to handle large volumes of bulk materials without manual intervention, reducing labor costs and improving workplace safety. The system is designed to be compact and space-efficient, making it suitable for facilities with limited floor space. Additionally, the equipment is equipped with advanced control systems that allow for precise control of the conveying process, including flow rate, pressure, and material discharge. This ensures consistent material quality and minimizes the risk of product contamination or loss. Another critical feature is the integration of dust collection and filtration systems, which help to minimize dust emissions and maintain a clean working environment. The equipment is also designed for easy maintenance and cleaning, with removable components that can be cleaned and sanitized to meet industry standards. Furthermore, the system can be customized to accommodate different bulk bag sizes and material types, providing flexibility for various applications. These features collectively contribute to a reliable, low-maintenance solution for bulk material handling.