Multi-hopper pneumatic powder conveying pumps, also known as multi-chamber pneumatic conveying systems, are advanced industrial equipment designed for efficient and reliable transport of bulk powders over long distances. This article explores the working principle and key features of such systems, providing insights into their operational mechanisms and practical applications.
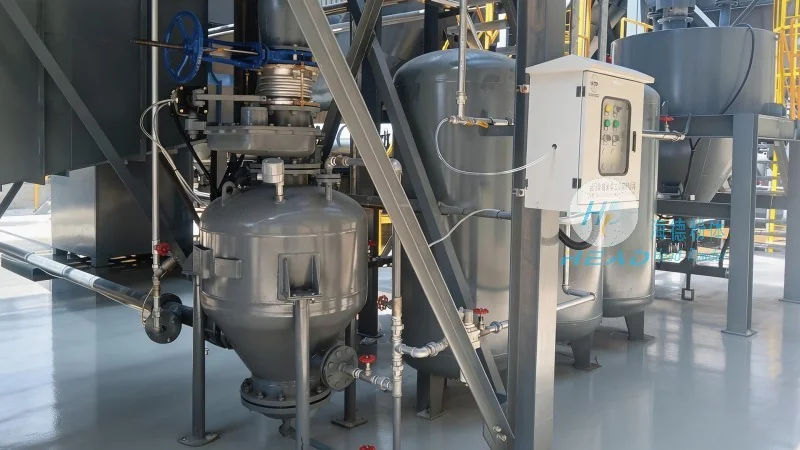
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer behind these advanced conveying solutions, is a leading company in the field of powder handling technology. Based in Shandong, China, HeadPowder specializes in the design, manufacturing, and supply of high-quality pneumatic conveying equipment. The company’s commitment to innovation and precision engineering ensures that their products meet the stringent requirements of various industrial sectors, including chemical, food, pharmaceutical, and cement industries.
Working Principle of Multi-Hopper Pneumatic Powder Conveying Pumps
The core of a multi-hopper pneumatic powder conveying pump lies in its ability to handle multiple powder streams simultaneously through a single or multiple air lines. The system typically consists of several hoppers, each equipped with a valve mechanism that allows for independent loading and unloading of different powder materials. When a hopper is activated, its valve opens, and the powder is drawn into the pump chamber by the pressure differential created by the compressed air. The air, carrying the powder particles, is then directed through the conveying line to the destination point. This process can be repeated for each hopper, enabling the simultaneous transport of multiple powders without the need for separate pipelines for each material.
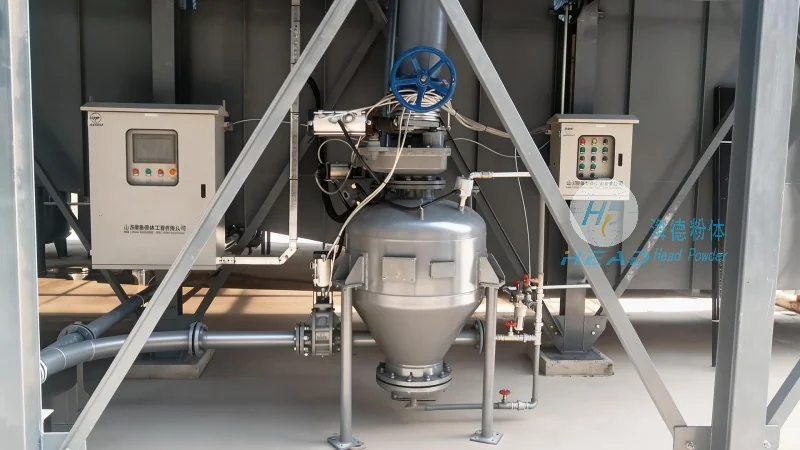
Key Features of Multi-Hopper Pneumatic Powder Conveying Systems
Multi-hopper pneumatic conveying pumps offer several distinct advantages that make them ideal for complex powder handling applications. Firstly, their ability to handle multiple powders in a single system reduces installation costs and space requirements compared to traditional single-hopper or multi-line systems. This feature is particularly beneficial for facilities that process a variety of materials, as it simplifies the overall infrastructure and maintenance. Secondly, the system’s design allows for precise control over the flow rate and pressure, ensuring consistent and uniform delivery of powders. This is crucial for applications where the quality of the final product is directly influenced by the consistency of the raw material feed. Thirdly, the use of compressed air as the conveying medium eliminates the need for mechanical components that come into direct contact with the powder, reducing wear and tear and minimizing the risk of contamination. This makes the system more durable and easier to clean, which is essential for industries with strict hygiene standards, such as food and pharmaceutical manufacturing.
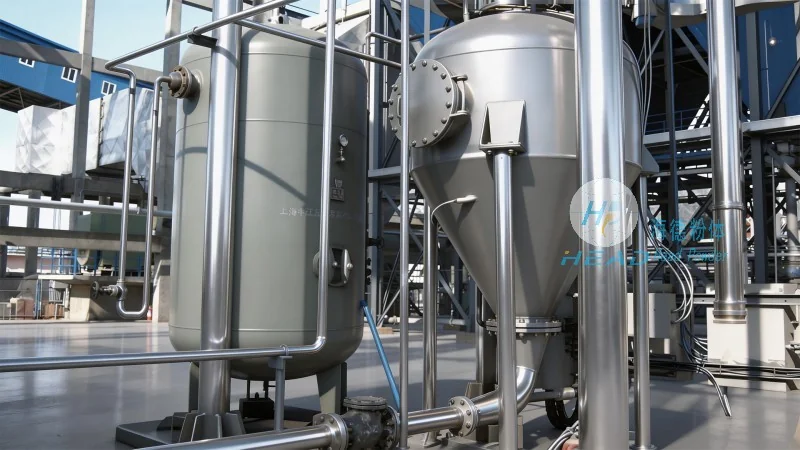
Operational Advantages and Practical Applications
Multi-hopper pneumatic powder conveying pumps excel in scenarios where flexibility and efficiency are paramount. For instance, in chemical plants, these systems can transport different raw materials to various processing units without interrupting production. In the food industry, they are used to move ingredients like flour, sugar, and spices to production lines while maintaining the product’s integrity and preventing cross-contamination. The cement industry also benefits from these systems, as they can handle large volumes of cement powder and distribute it to storage silos or mixing plants efficiently. Additionally, the system’s ability to operate under negative pressure reduces the risk of dust emissions, contributing to a safer working environment and compliance with environmental regulations.
Conclusion and Company Commitment
Multi-hopper pneumatic powder conveying pumps represent a sophisticated solution for modern powder handling challenges. By integrating multiple hoppers into a single, efficient system, these devices offer enhanced flexibility, reduced operational costs, and improved product quality. HeadPowder Engineering Co., Ltd., with its expertise and dedication to quality, continues to develop and refine these technologies to meet the evolving needs of industrial clients worldwide. For businesses seeking reliable and efficient powder transport solutions, multi-hopper pneumatic conveying pumps from HeadPowder are a proven choice.




