HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying equipment tailored for handling cement, fly ash, and mineral powders. This article explores the fundamental working principles and key characteristics of such systems, providing insights into their operational efficiency and industrial applications.
Working Principle of Pneumatic Conveying Equipment
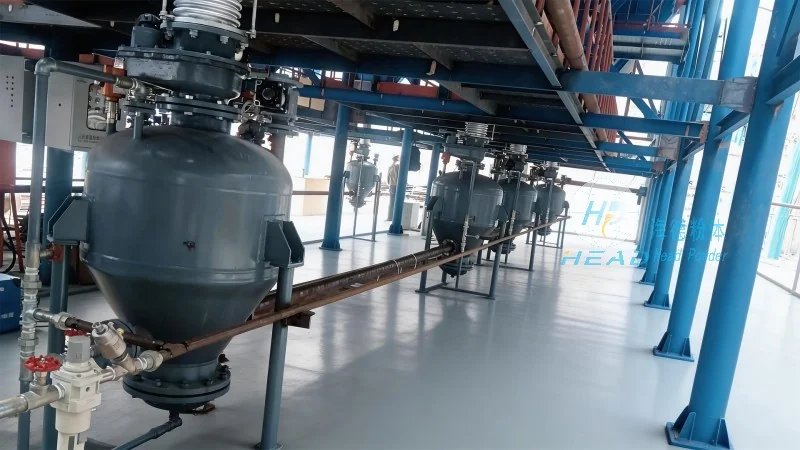
Pneumatic conveying systems for cement, fly ash, and mineral powders operate by transporting bulk materials through a pipeline using compressed air or a vacuum. The primary working principle involves creating a pressure differential that propels the material along the conveying line. There are two main types of pneumatic conveying systems: positive pressure and negative pressure (or vacuum) systems.
In positive pressure systems, compressed air is introduced at the material inlet, generating a pressure higher than the ambient air pressure. This pressurized air carries the powder particles through the pipeline, ensuring continuous and efficient transport. The system typically includes a blower or air compressor, a material feeder, and a discharge device. The compressed air provides the necessary force to overcome friction and gravitational forces, enabling the material to move smoothly from the source to the destination.
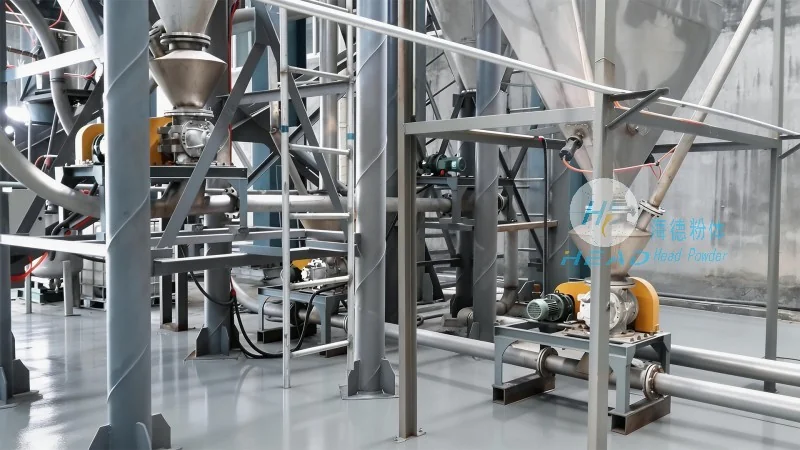
Negative pressure systems, on the other hand, create a vacuum at the discharge end of the pipeline, drawing the material into the system. The vacuum pulls the powder particles from the source and transports them through the pipeline. This method is often used for applications requiring dust control and environmental compliance, as the sealed system minimizes particle emissions. The system comprises a vacuum pump, a material inlet, and a discharge valve, with the vacuum level carefully controlled to maintain optimal conveying performance.
Key Features of Cement, Fly Ash, and Mineral Powder Pneumatic Conveyors
HeadPowder's pneumatic conveying equipment for cement, fly ash, and mineral powders is designed with several key features that enhance performance and reliability. One of the most significant advantages is the ability to handle fine and abrasive materials without causing excessive wear on the system components. The equipment incorporates robust materials of construction, such as stainless steel or corrosion-resistant alloys, to withstand the harsh conditions of mineral powder handling.
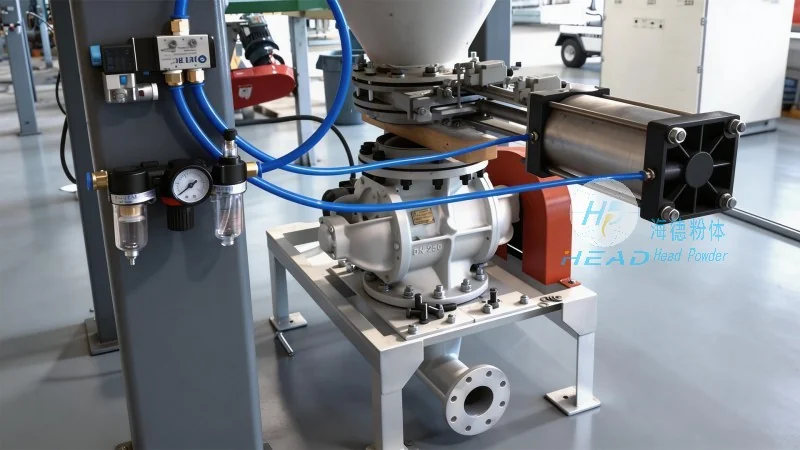
Another critical feature is the system's efficiency in terms of energy consumption and operational costs. By using compressed air or vacuum to transport materials, the equipment minimizes the need for mechanical conveyors, reducing maintenance and operational expenses. The design also allows for flexible installation, enabling the system to be integrated into existing industrial processes with minimal disruption.
Dust control is a paramount concern in the handling of cement and fly ash, and HeadPowder's systems address this with advanced sealing and filtration technologies. The enclosed pipeline design prevents dust emissions, ensuring compliance with environmental regulations and providing a safer working environment for personnel. Additionally, the system's modular construction facilitates easy maintenance and component replacement, extending the equipment's service life.
Applications and Industrial Benefits
The pneumatic conveying systems developed by HeadPowder are widely used in various industries, including cement production, power generation, and mining. In cement plants, these systems efficiently transport raw materials like fly ash and mineral powders to the grinding mills, optimizing the production process and reducing downtime. In power plants, the equipment handles fly ash from coal combustion, facilitating its reuse in concrete production and minimizing waste disposal costs.
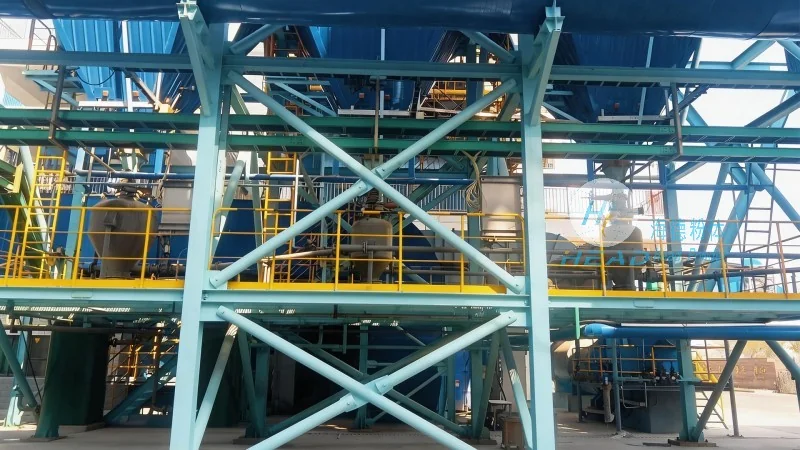
The industrial benefits of using pneumatic conveying for cement, fly ash, and mineral powders are substantial. The systems offer high throughput rates, allowing for increased production capacity and improved operational efficiency. They also reduce the risk of material contamination, as the enclosed system prevents cross-contamination between different materials. Furthermore, the low maintenance requirements and long service life of the equipment contribute to overall cost savings for industrial operations.
Conclusion
HeadPowder's pneumatic conveying equipment for cement, fly ash, and mineral powders combines advanced technology with robust design to provide efficient, reliable, and environmentally friendly material handling solutions. By understanding the working principles and key features of these systems, industrial operators can make informed decisions to enhance their production processes and meet regulatory requirements. With a strong presence in Shandong, China, HeadPowder continues to innovate and deliver high-quality equipment that meets the evolving needs of the industry.




