Principle and Working Scene Characteristics of Hydroxide Cobalt Powder Conveying System Equipment
Release time:2026-09-19 08:01:30
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For businesses in the battery materials sector, the efficient and reliable handling of hydroxide cobalt powder is crucial for maintaining production efficiency and product quality. The hydroxide cobalt powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., addresses these needs through a specialized design that ensures safe and effective material transport. This article explores the underlying principles of this system and its key working scene characteristics.
Understanding the Core Principles of Hydroxide Cobalt Powder Conveying Systems
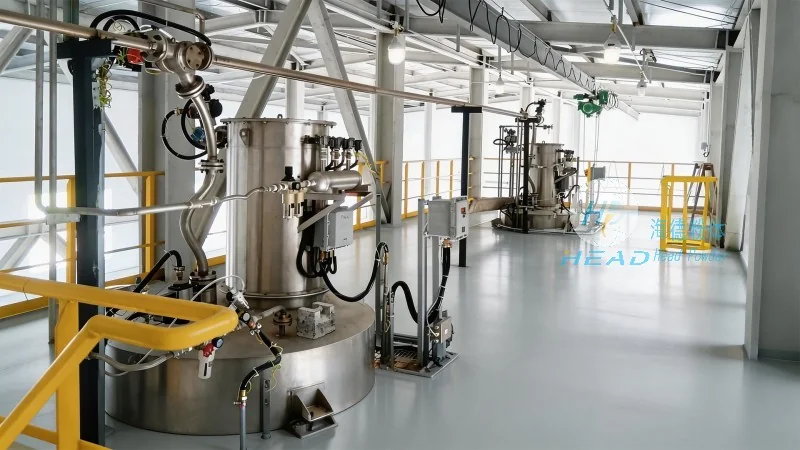
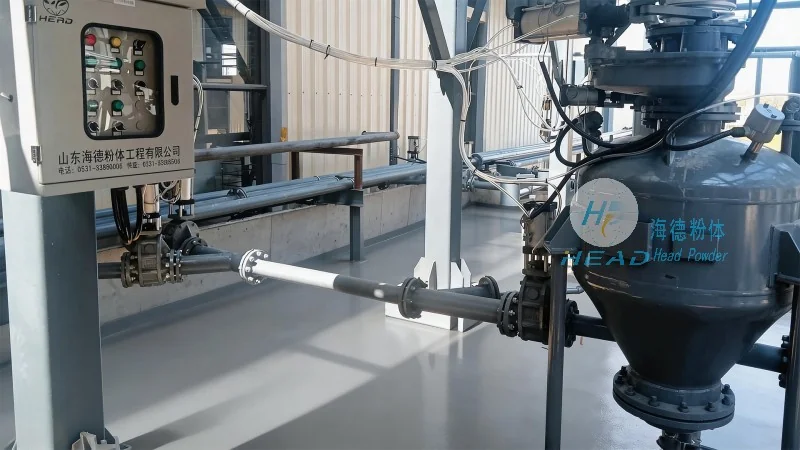
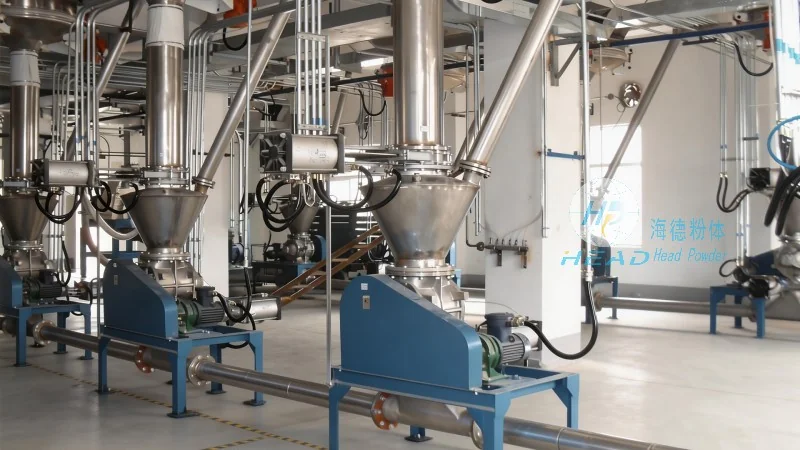
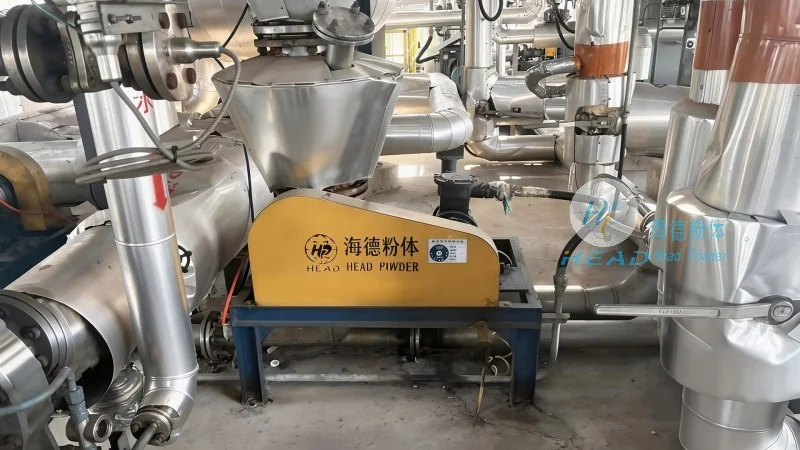
The hydroxide cobalt powder conveying system operates on the principle of utilizing advanced pneumatic or mechanical conveying technologies to transport fine powders like hydroxide cobalt. The system typically integrates components such as feeders, conveying pipes, control valves, and dust collection units. The feeding mechanism ensures a consistent and controlled flow of powder into the conveying line, while the pneumatic or mechanical action propels the material through the system. This design minimizes material degradation and ensures that the powder remains in a stable state during transport. The system's control system allows for real-time monitoring and adjustment of flow rates, pressure, and other parameters to optimize performance and prevent issues like blockages or dust emissions. The integration of these components is critical for achieving the system's overall efficiency and reliability, as each part works in concert to ensure smooth material handling from the source to the destination.
Key Working Scene Characteristics of the Conveying System
The hydroxide cobalt powder conveying system is designed to operate in various industrial environments, particularly in battery material production facilities. Its working scene characteristics are tailored to meet the specific demands of these settings. For instance, the system is built to handle the high-volume, continuous production requirements of battery material manufacturers. The equipment's robust construction and durable materials ensure it can withstand the rigorous conditions of industrial use, including exposure to moisture, temperature fluctuations, and abrasive particles. Additionally, the system's modular design allows for easy integration into existing production lines, reducing downtime during installation and maintenance. The dust control features are also critical in working scenes where air quality and safety are paramount, as hydroxide cobalt powder can be fine and potentially hazardous if not managed properly. The system's ability to maintain a clean and safe working environment is a key characteristic that enhances operational efficiency and compliance with safety regulations. Furthermore, the system's energy efficiency is a notable feature in working scenes where operational costs are a significant consideration, as it minimizes energy consumption while maintaining high transport capacity.




