Mineral powder material handling involves the efficient transportation and management of bulk materials such as ores, powders, and granules. The core principles revolve around optimizing the flow of these materials from one point to another, ensuring minimal loss, energy efficiency, and operational safety. Key principles include the selection of appropriate equipment based on material properties, the design of suitable conveying systems, and the implementation of control mechanisms to maintain consistent performance. Understanding these principles is crucial for industries like mining, cement, and chemical processing, where reliable material handling directly impacts production efficiency and cost-effectiveness.
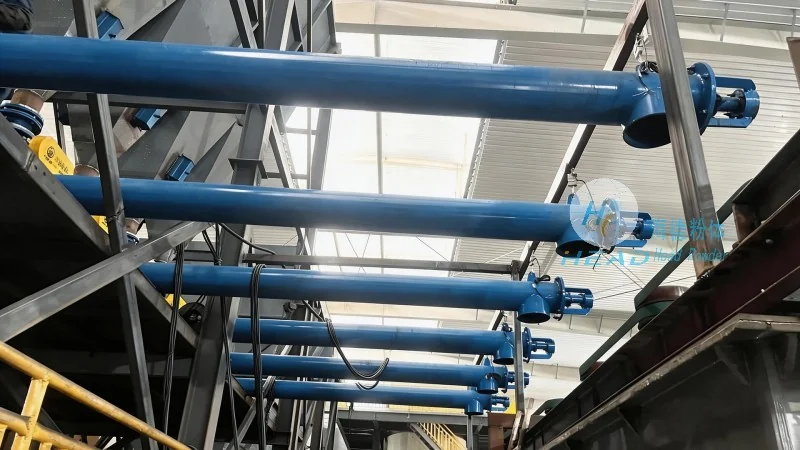
Working Scene Characteristics of Mineral Powder Conveying Systems
The working scene characteristics of mineral powder material handling systems vary significantly based on the specific application and environment. For instance, in open-pit mining operations, the systems must handle large volumes of crushed ore and dust, often under harsh weather conditions. In contrast, indoor cement plants require more controlled environments to prevent dust dispersion and maintain product quality. The characteristics also include the need for high throughput rates, especially in industrial production lines, and the importance of dust control measures to comply with environmental regulations. Additionally, the systems must be adaptable to different material types, from fine powders to coarse granules, and capable of operating in both continuous and intermittent modes depending on the production schedule.
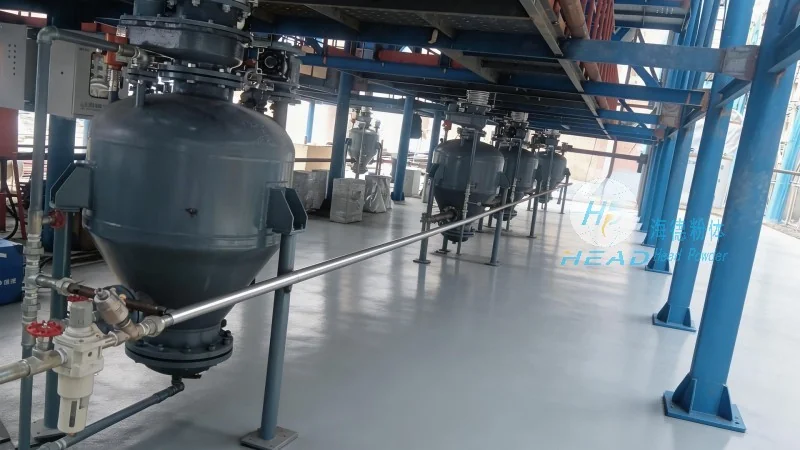
HeadPowder Engineering: Expertise in Mineral Powder Material Handling
Shandong HeadPowder Engineering Co., Ltd. specializes in providing comprehensive solutions for mineral powder material handling. With a focus on innovation and practical application, the company designs and manufactures advanced conveying systems tailored to the unique needs of each client. The company's expertise covers a wide range of equipment, including belt conveyors, screw conveyors, pneumatic conveyors, and bucket elevators, each selected based on the specific material characteristics and operational requirements. By integrating state-of-the-art technology with years of industry experience, HeadPowder ensures that its solutions are not only efficient but also durable and cost-effective. The company's team of engineers and technicians works closely with clients to understand their production challenges and develop customized solutions that enhance productivity and reduce operational costs.
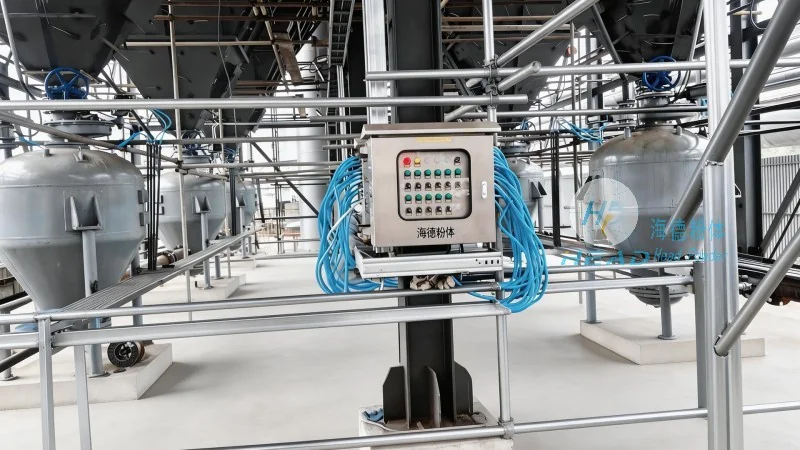
Key Features of HeadPowder's Material Handling Solutions
HeadPowder's material handling solutions are characterized by several key features that set them apart in the industry. Firstly, the systems are designed with high material handling capacity, capable of processing large volumes of mineral powders at consistent speeds. This is achieved through the use of robust components and optimized system layouts. Secondly, the solutions prioritize energy efficiency, reducing operational costs while minimizing environmental impact. Advanced control systems and energy-saving technologies are integrated into the design to achieve this goal. Thirdly, the systems are built for durability and reliability, with components made from high-quality materials that can withstand the harsh conditions of mineral processing environments. This durability ensures long service life and low maintenance requirements, contributing to overall cost savings. Additionally, the solutions offer flexibility in terms of material handling, allowing for easy adaptation to changes in production needs or material types. This adaptability is crucial for industries that may experience fluctuations in production or need to handle different product lines.
Application Examples and Case Studies
HeadPowder's mineral powder material handling systems have been successfully implemented in various applications across different industries. For example, in a cement production plant, the company installed a combination of belt conveyors and pneumatic conveyors to transport raw materials from storage to the production line. The system was designed to handle high volumes of limestone and clay, with dust control measures integrated to meet environmental standards. The result was a significant improvement in production efficiency and a reduction in material loss. In another case, a mining company used HeadPowder's bucket elevators to transport crushed ore from the mine to the processing plant. The system's ability to handle coarse materials and its robust design ensured reliable operation even under heavy load conditions. These examples illustrate the versatility and effectiveness of HeadPowder's solutions in real-world applications.
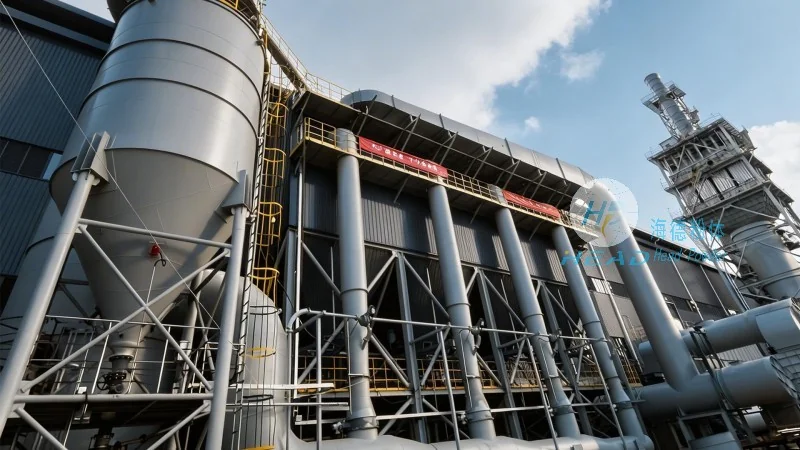
Conclusion: Enhancing Efficiency with HeadPowder Engineering
Mineral powder material handling is a critical aspect of many industrial processes, and the principles and characteristics of the systems play a vital role in their success. By understanding these principles and leveraging advanced technology, companies can optimize their material handling operations. Shandong HeadPowder Engineering Co., Ltd. stands as a leader in this field, providing expert solutions that enhance efficiency, reduce costs, and ensure compliance with environmental regulations. With a commitment to quality and customer satisfaction, HeadPowder continues to deliver innovative and reliable material handling systems that meet the evolving needs of the industry.




