Methylcellulose, a versatile polymer widely used in various industries, often requires efficient and reliable material handling solutions. The air-driven pneumatic conveying line, as a key technology in material transport, offers a solution that combines efficiency with flexibility. This article explores the fundamental principles behind such systems and highlights the specific characteristics of their application in working environments, particularly for methylcellulose materials.
The Core Principle of Air-Driven Pneumatic Conveying
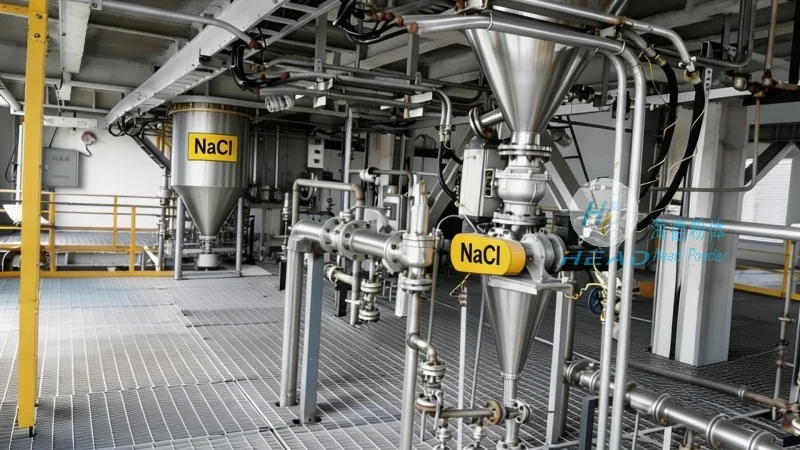
At its essence, an air-driven pneumatic conveying system operates by using compressed air to transport bulk materials through a pipeline. The process involves several critical components, including a material hopper, a rotary valve, a conveying pipe, and a receiver. The material is first fed into the hopper, where it is then discharged into the conveying pipe via the rotary valve. Compressed air, introduced at the inlet of the pipe, creates a pressure differential that propels the material forward. This method is particularly effective for fine or powdery substances like methylcellulose, as it minimizes product degradation and ensures a consistent flow.
Working Scene Characteristics of Methylcellulose Pneumatic Conveying Lines
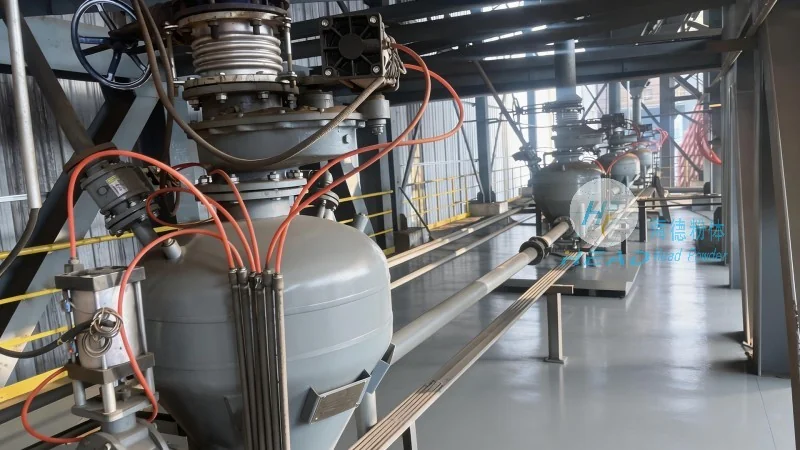
The application of air-driven pneumatic conveying lines for methylcellulose materials is characterized by several distinct features that enhance operational efficiency and product quality. First, the system's ability to handle fine powders without clogging or blockages is crucial, as methylcellulose can be sensitive to moisture and agglomeration. The design of the conveying line, including the use of smooth, corrosion-resistant pipes and appropriate air velocities, ensures that the material moves smoothly through the system. Additionally, the system's compactness and modularity allow for easy integration into existing production lines, reducing installation time and costs.
Advantages in Industrial Applications
For industries dealing with methylcellulose, the air-driven pneumatic conveying line provides several advantages over traditional methods such as belt conveyors or manual handling. These include improved hygiene, as the enclosed system prevents contamination from external sources. It also enhances safety by eliminating the need for manual handling of powders, reducing the risk of dust explosions or respiratory issues. Furthermore, the system's energy efficiency, particularly when optimized for air pressure and flow rates, contributes to lower operational costs over time.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
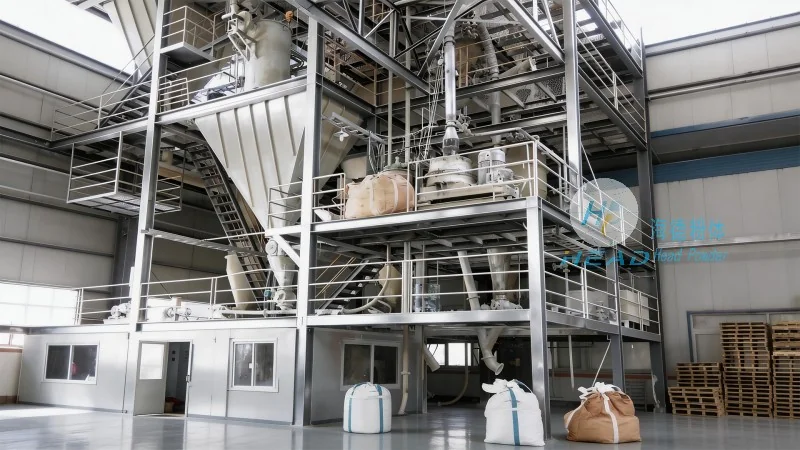
HeadPowder, a leading provider of material handling solutions, specializes in designing and manufacturing air-driven pneumatic conveying systems tailored to the needs of various industries. With a focus on innovation and quality, the company has established itself as a trusted partner for businesses requiring reliable and efficient material transport. HeadPowder's expertise lies in customizing systems to meet specific material characteristics, such as the unique properties of methylcellulose, ensuring optimal performance and longevity.
Location and Accessibility
HeadPowder Engineering Co., Ltd. is headquartered in Shandong, China, a region known for its robust industrial infrastructure and manufacturing capabilities. The company's location provides easy access to major transportation networks, facilitating the delivery of equipment and technical support to clients across the region and beyond. This strategic positioning enables HeadPowder to serve a wide range of industries, from pharmaceuticals and food processing to chemical manufacturing, with timely and effective solutions.




