Carbon black and coal powder are critical raw materials in various industrial applications, and efficient handling of these powders is essential for maintaining production efficiency and product quality. The pneumatic conveying equipment designed by Shandong HeadPowder Engineering Co., Ltd. offers a reliable solution for transporting these fine powders with precision and control. This equipment is engineered to handle the unique characteristics of carbon black and coal powder, ensuring minimal loss, low contamination, and consistent flow rates.
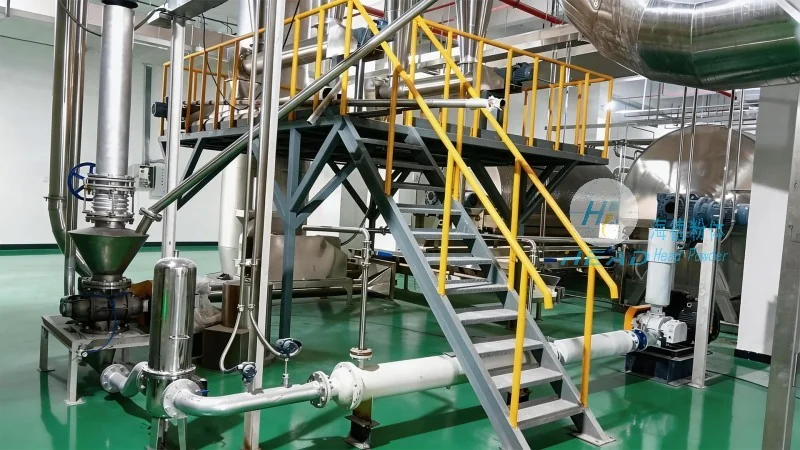
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling technology, specializes in developing advanced pneumatic conveying systems tailored to the demands of modern industrial processes. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses requiring efficient and safe material transport solutions. HeadPowder's products are designed to meet stringent industry standards, providing durability, energy efficiency, and user-friendly operation. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver cutting-edge solutions to global markets.
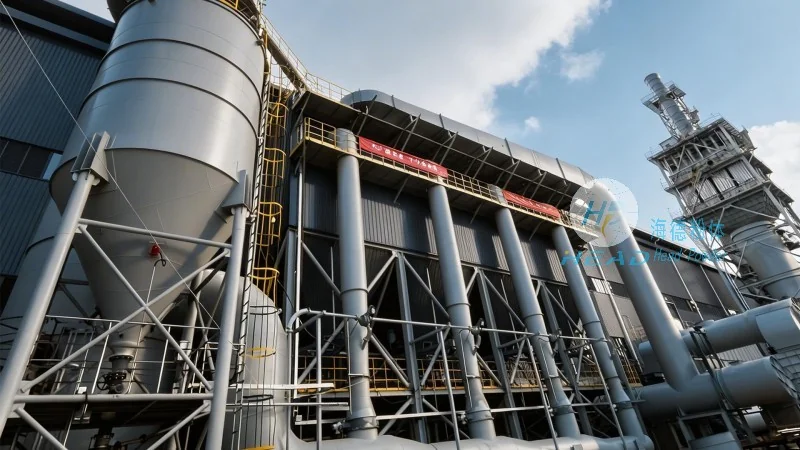
Key Features of the Pneumatic Conveying System
The carbon black coal powder pneumatic conveying equipment from HeadPowder is equipped with several key features that enhance its performance and usability. These include high-pressure air pumps that generate the necessary force to move the powders through the system, flexible hose or pipeline configurations that adapt to different layout requirements, and advanced control systems that allow for precise regulation of flow rates and pressure. The equipment is also designed with materials that are resistant to abrasion and corrosion, ensuring long-term reliability even when handling abrasive carbon black particles. Additionally, the system incorporates safety features such as pressure relief valves and overcurrent protection to prevent accidents and equipment damage.
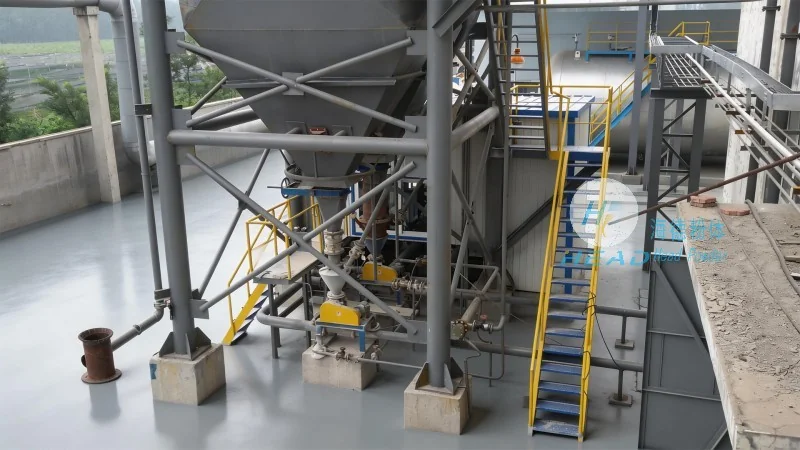
Operation Process of the Pneumatic Conveying Equipment
The operation of the carbon black coal powder pneumatic conveying system involves several steps that ensure smooth and efficient material transport. First, the carbon black or coal powder is fed into the hopper or storage silo, where it is held until needed. The system then activates the air pump, which draws air from the environment and compresses it to a high pressure. This pressurized air is then introduced into the conveying line, creating a flow that carries the powder particles through the system. The powder is transported from the source to the destination, such as a storage tank or processing unit, with minimal loss and maximum efficiency. The system continuously monitors pressure and flow rates, adjusting as needed to maintain optimal performance. Once the material reaches its destination, the air is released, and the powder is discharged into the receiving container. The entire process is automated, reducing the need for manual intervention and minimizing the risk of human error.
Working Principle of the Pneumatic Conveying System
The working principle of the carbon black coal powder pneumatic conveying equipment is based on the use of compressed air to transport the fine powders. The system operates by creating a pressure differential between the source and destination points. The high-pressure air creates a flow that entrains the powder particles, allowing them to be carried through the conveying line. The key components of the system include the air compressor, which generates the necessary pressure; the hopper or feeder, which supplies the powder; the conveying line, which transports the material; and the receiver or discharge unit, which collects the material at the end of the line. The air and powder mixture travels through the line at a velocity sufficient to overcome the gravitational forces and frictional resistance, ensuring that the powder is transported without clogging or segregation. The system also incorporates a filter or separator at the receiving end to remove any excess air and prevent contamination of the final product.
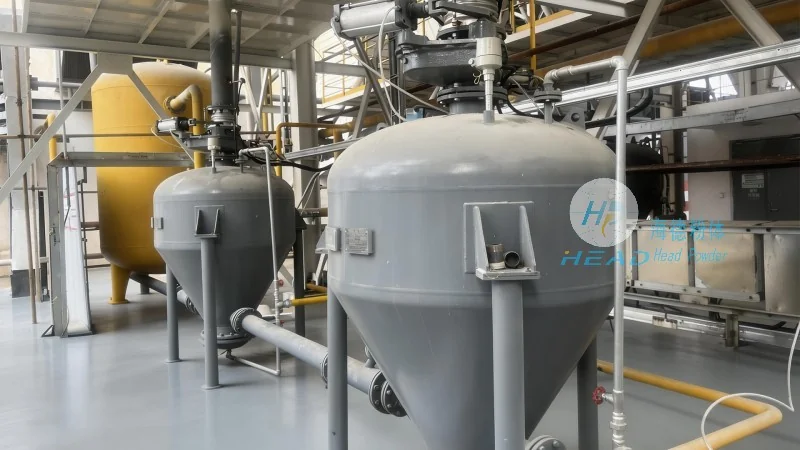
Benefits of Using Carbon Black Coal Powder Pneumatic Conveying Equipment
Implementing the carbon black coal powder pneumatic conveying equipment from HeadPowder offers numerous benefits for industrial operations. One of the primary advantages is the reduction in material loss and contamination, as the system minimizes direct contact between the powder and the environment. This leads to higher product purity and quality, which is crucial for applications where even small amounts of impurities can affect the final product. Additionally, the system enhances production efficiency by allowing for continuous and automated material transport, reducing downtime and increasing throughput. The energy efficiency of the system is another significant benefit, as it uses compressed air efficiently and minimizes energy waste. The equipment also improves workplace safety by eliminating the need for manual handling of powders, reducing the risk of dust explosions and respiratory issues. Furthermore, the system's modular design allows for easy integration into existing production lines, making it a flexible and cost-effective solution for businesses looking to upgrade their material handling capabilities.




