For industrial applications requiring efficient and reliable transport of activated carbon granules, the pneumatic conveying system offered by Shandong HeadPowder Engineering Co., Ltd. stands as a sophisticated solution. This equipment is designed to handle the unique challenges associated with transporting fine to medium-sized granular materials, ensuring minimal product degradation and optimal operational efficiency. The following sections outline the operational process and the underlying working principles of this advanced system.
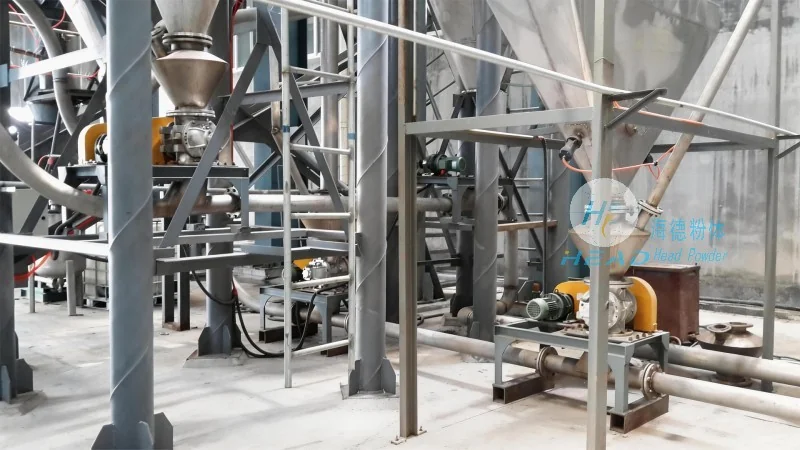
Overview of the Activated Carbon Granule Pneumatic Conveying System
The system is engineered to facilitate the seamless movement of activated carbon granules from a storage hopper or silo to processing units, such as reactors or filters, without the need for mechanical components like conveyor belts or buckets. By utilizing compressed air or gas as the conveying medium, the system achieves a dust-free, low-maintenance transport method that is particularly advantageous for handling materials that are prone to caking or agglomeration. HeadPowder, a leading manufacturer in this field, has optimized the design to meet the stringent requirements of various industrial sectors, including chemical processing, water treatment, and pharmaceutical manufacturing.
The Operational Process: Step-by-Step Execution
The operation of the activated carbon granule pneumatic conveying system follows a systematic sequence of steps that ensure consistent and efficient material transport. Initially, the activated carbon granules are stored in a hopper equipped with a feeding mechanism, such as a rotary valve or a screw feeder, which regulates the flow rate into the conveying line. The granules then enter the conveying pipe, where they are mixed with the conveying medium—typically compressed air or a combination of air and inert gas. As the mixture moves through the pipe, the air velocity is maintained at a level sufficient to keep the granules in suspension, preventing blockages and ensuring smooth flow. The conveying line may include components like bends, expansion joints, and filters to manage the air flow and protect the system from particulate buildup. Upon reaching the destination, the granules are separated from the air stream through a separator, such as a cyclone or a bag filter, and collected in a receiving hopper or container. The separated air is then discharged back into the system or vented to the atmosphere, depending on the system design and environmental regulations.
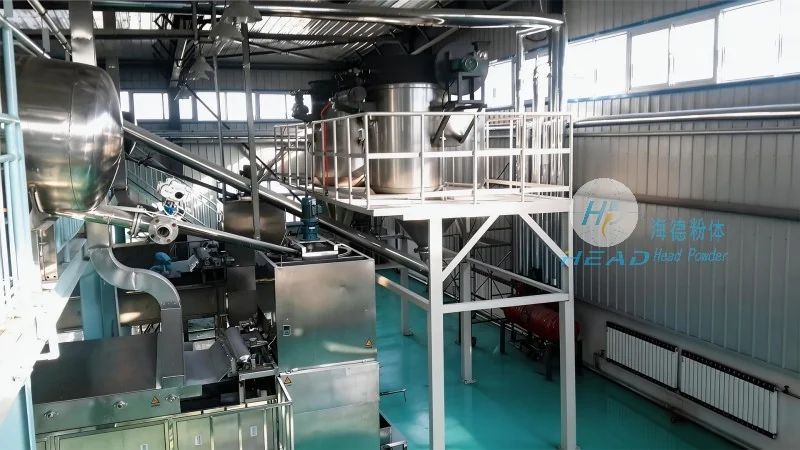
Working Principle: The Physics Behind Pneumatic Conveying
The core working principle of the activated carbon granule pneumatic conveying system is based on the fundamental physics of fluid dynamics and particle suspension. The system operates by creating a pressure differential between the inlet and outlet of the conveying line, which generates a flow of air or gas. The velocity of the conveying medium is critical; it must be high enough to overcome the gravitational force acting on the granules and to maintain them in a suspended state. This is achieved by calculating the appropriate air velocity based on the particle size, density, and flow rate of the activated carbon granules. The system utilizes either positive pressure (where air is forced into the conveying line) or negative pressure (where air is drawn out), with positive pressure being more common for transporting granules over longer distances or to multiple destinations. The design of the system, including the diameter of the conveying pipe, the angle of bends, and the placement of components, is carefully optimized to minimize energy consumption and maximize conveying efficiency. HeadPowder's engineering expertise ensures that the system is tailored to the specific characteristics of the activated carbon granules, such as their particle size distribution, moisture content, and flowability, to achieve optimal performance.
Key Features and Advantages of the System
The activated carbon granule pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. incorporates several key features that enhance its performance and reliability. These include: a) Adjustable feeding mechanisms that allow precise control over the material flow rate, b) High-efficiency separators that ensure minimal product loss and clean air discharge, c) Flexible conveying lines that can be configured for various layouts, including vertical and horizontal transport, d) Low maintenance requirements due to the absence of moving parts in the conveying line, and e) Energy-efficient operation through optimized air velocity and system design. The system's advantages extend beyond mere efficiency, as it provides a dust-free environment, reduces product contamination, and minimizes the risk of material degradation during transport. These benefits make it an ideal choice for industries where product quality and process integrity are paramount.
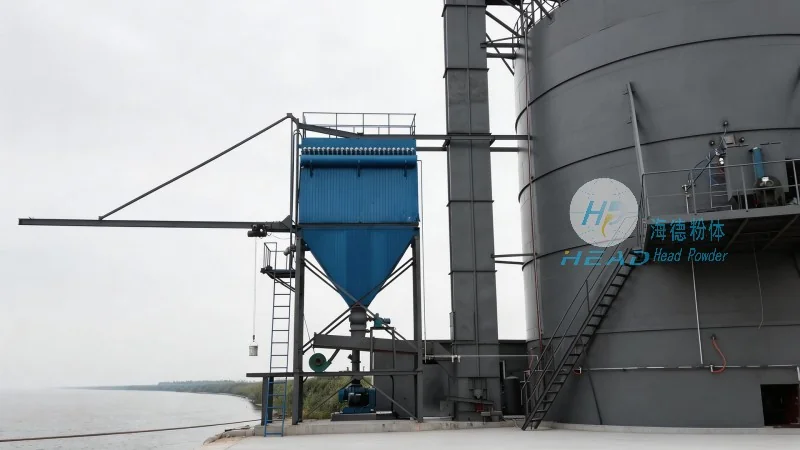
Application Scenarios and Industry Impact
The activated carbon granule pneumatic conveying system is widely used in various industrial applications where the transport of activated carbon granules is critical. In the chemical industry, it is employed in the production of activated carbon-based adsorbents, where the granules need to be transferred from storage to reactors for further processing. In water treatment facilities, the system is used to convey activated carbon for filtration and adsorption processes, ensuring clean and safe water supply. The pharmaceutical industry also benefits from this system, as it enables the handling of activated carbon granules in sterile and controlled environments, minimizing the risk of contamination. The system's adaptability and reliability have made it a preferred choice for manufacturers seeking to streamline their production processes and improve overall operational efficiency. By reducing downtime and maintenance costs, the system contributes to enhanced productivity and cost savings for businesses operating in these sectors.
Conclusion: The Role of HeadPowder in Advanced Material Handling
Shandong HeadPowder Engineering Co., Ltd. has established itself as a leading provider of pneumatic conveying systems for activated carbon granules, leveraging its expertise in engineering and manufacturing to deliver high-quality, reliable equipment. The operation process and working principles of the system, as outlined above, demonstrate the advanced technology and meticulous design that underpin its performance. By adhering to strict quality standards and customer-centric approaches, HeadPowder ensures that its systems meet the diverse needs of industrial clients while maintaining operational excellence. The continued development and optimization of such systems are crucial for industries that rely on efficient material handling, and HeadPowder remains at the forefront of innovation in this domain. With its commitment to excellence and customer satisfaction, the company continues to play a vital role in advancing the capabilities of material transport in various industrial applications.




