HeadPowder, a leading enterprise in the field of powder conveying technology, specializes in the design, manufacturing, and installation of advanced systems for handling shredded paper powder. Based in Shandong, China, the company has established itself as a trusted provider of efficient and reliable conveying solutions tailored to the unique demands of the paper recycling and waste management industries.
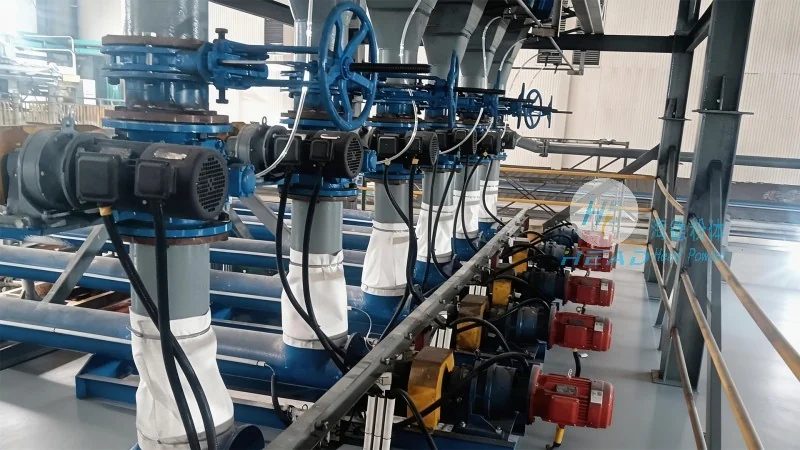
Overview of the Shredded Paper Powder Conveying Line
The shredded paper powder conveying line is a sophisticated system engineered to transport fine, dry shredded paper particles from collection points to processing or storage facilities. This line integrates multiple components, including feed hoppers, conveyor mechanisms, control panels, and dust collection systems, to ensure a seamless and efficient operation. The design prioritizes durability, low maintenance, and high throughput, making it suitable for both industrial and commercial applications.
Key Components and Their Functions
At the core of the conveying line are several critical components that work in harmony to achieve optimal performance. The feed hopper is responsible for receiving shredded paper powder and maintaining a consistent material level. It is equipped with a level sensor to prevent overfilling and ensure smooth feeding. The conveyor system, typically consisting of screw conveyors or pneumatic pipelines, transports the powder through the line. Screw conveyors are ideal for horizontal or slight incline transport, providing gentle handling that minimizes particle degradation. Pneumatic conveyors, on the other hand, use air pressure to move the powder, offering flexibility in routing and the ability to handle longer distances. The control panel integrates sensors and actuators, allowing for real-time monitoring and adjustment of the system's speed, pressure, and flow rate. This ensures that the conveying process remains stable and responsive to variations in material feed.
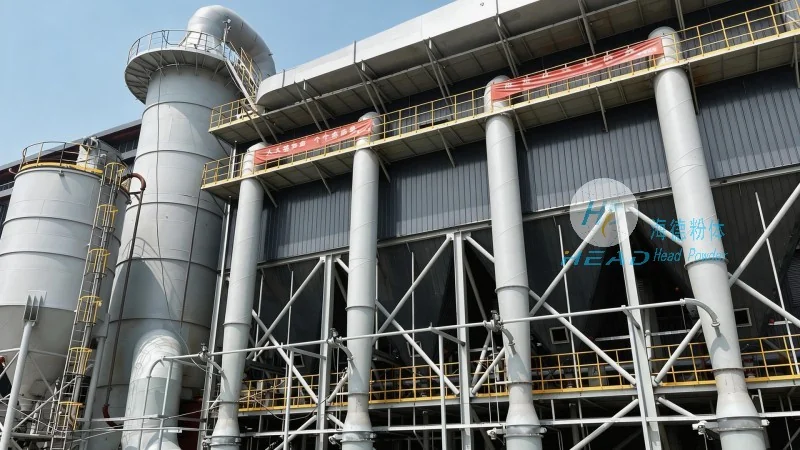
Operation Process: Step-by-Step Workflow
The operation of the shredded paper powder conveying line follows a systematic workflow that ensures efficient material handling. The process begins with the loading of shredded paper into the feed hopper. As the material accumulates, the level sensor triggers the conveyor to start. The conveyor then transports the powder to the next stage of the system, such as a storage silo or a processing unit. During transport, the system continuously monitors the flow rate and pressure to maintain optimal performance. If any abnormalities are detected, the control panel activates alarms or adjusts the conveyor speed to prevent blockages or overloads. The system also incorporates a dust collection system to capture airborne particles, ensuring a clean and safe working environment. This integrated approach minimizes downtime and maximizes productivity.
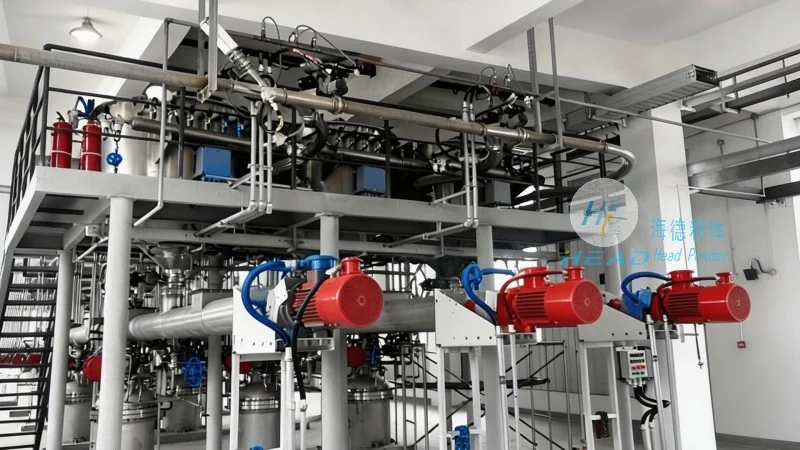
Working Principle: How the System Operates
The working principle of the shredded paper powder conveying line is based on the principles of mechanical and pneumatic transport, depending on the specific design of the system. For screw conveyors, the operation relies on the rotation of a helical screw within a trough. As the screw rotates, it pushes the material forward, creating a continuous flow. The speed of the screw and the angle of the trough determine the conveying capacity and the distance the material can travel. For pneumatic conveyors, the system uses compressed air to create a pressure differential that propels the powder through the pipeline. The air flow is controlled by a blower or compressor, and the system may include cyclone separators or filters to separate the powder from the air and return the air to the system for reuse. The control panel coordinates all these functions, ensuring that the system operates in a synchronized manner. This combination of mechanical and pneumatic elements allows the line to handle the delicate nature of shredded paper powder without causing damage or degradation.
Advantages and Applications
The shredded paper powder conveying line offers several advantages that make it a preferred choice for industries dealing with shredded paper. Its ability to handle fine, dry powders with minimal degradation ensures that the material remains in optimal condition for processing. The system's low maintenance requirements and high reliability reduce operational costs and downtime. Additionally, the integrated dust collection system enhances safety and compliance with environmental regulations. The line is widely used in paper recycling facilities, where it transports shredded paper from collection bins to processing machines. It is also applicable in waste management plants, where it helps in the efficient transfer of shredded paper to storage or disposal areas. The flexibility of the system allows it to be customized to meet the specific needs of different applications, making it a versatile solution for various industrial settings.




