This article aims to provide a comprehensive understanding of nitrogen-protected material conveying lines, focusing on their design principles and the role they play in industrial applications. By exploring the core components and operational mechanisms, we can better appreciate how these systems ensure the integrity and quality of materials during transportation.
Understanding the Core Concept of Nitrogen-Protected Material Conveying Lines
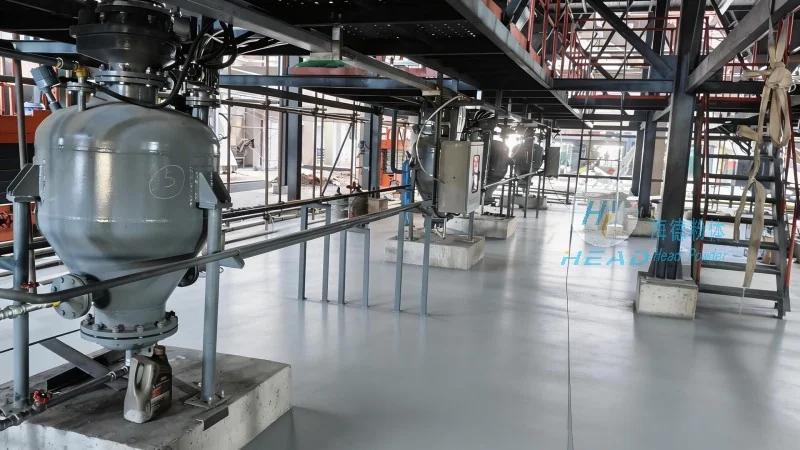
A nitrogen-protected material conveying line is a specialized system designed to transport bulk materials, such as powders or granules, in an inert gas environment. The primary purpose of this design is to prevent oxidation, moisture absorption, or contamination of the material during the conveying process. This is particularly crucial for materials that are sensitive to air exposure, including pharmaceuticals, food products, and certain chemicals. The system typically incorporates a sealed pipeline, a nitrogen gas supply, and a control system to maintain a stable inert atmosphere throughout the entire conveying operation.
The Key Design Principles Behind Nitrogen-Protected Conveying Systems
The design of a nitrogen-protected material conveying line is guided by several critical principles to ensure optimal performance and material protection. First, the system must maintain a consistent positive pressure within the conveying pipeline to prevent the ingress of ambient air. This is achieved through the continuous supply of nitrogen gas, which displaces oxygen and moisture from the material and the pipeline. Second, the selection of appropriate materials for the pipeline and components is essential to avoid chemical reactions or corrosion with the conveyed material. For instance, stainless steel or specialized plastics are commonly used to handle corrosive or abrasive materials. Third, the control system plays a vital role in monitoring and regulating the nitrogen flow rate, pressure, and temperature to maintain the desired inert environment. Advanced sensors and feedback mechanisms help in real-time adjustments, ensuring the system operates within safe and efficient parameters.
Components and Operational Mechanisms of the Conveying Line
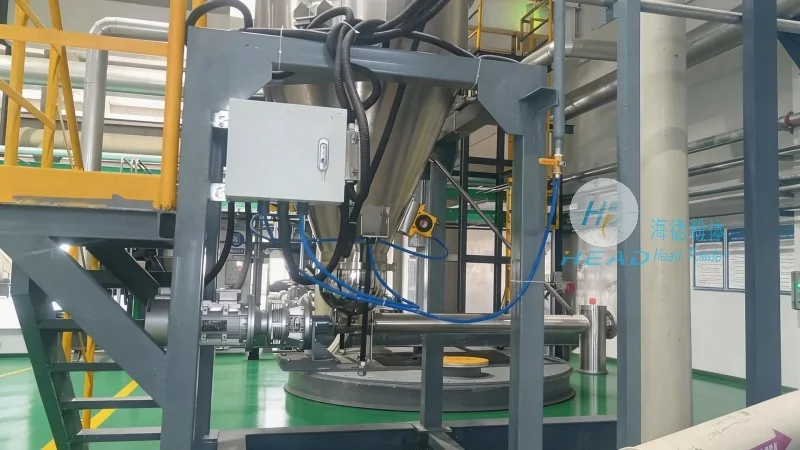
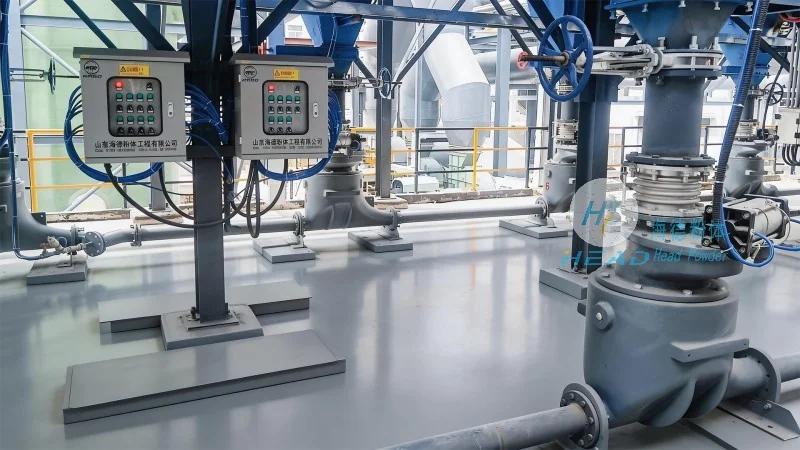
The nitrogen-protected material conveying line consists of several key components that work in harmony to achieve the desired results. The main components include a hopper or feeder for material loading, a conveyor (such as a screw or pneumatic conveyor) to transport the material, a nitrogen gas inlet and distribution system, and a control panel for system management. The material is typically fed into the hopper, where it is then conveyed through the pipeline under the pressure of the nitrogen gas. The gas acts as a carrier, moving the material while maintaining an inert atmosphere. The system may also include filters and separators to remove any fines or contaminants from the material, ensuring a clean and consistent product flow. The control panel allows operators to adjust the conveying speed, gas pressure, and other parameters as needed, providing flexibility and adaptability to different material types and processing requirements.
Applications and Benefits of Nitrogen-Protected Conveying Systems
Nitrogen-protected material conveying lines are widely used in various industries where material integrity is paramount. In the pharmaceutical industry, for example, these systems are essential for transporting active pharmaceutical ingredients (APIs) and excipients to prevent degradation or contamination. In the food industry, they are used for conveying ingredients like flour, sugar, or spices to maintain freshness and quality. The chemical industry also benefits from these systems when handling sensitive chemicals that are prone to oxidation or reaction with air. The primary benefits of using such a system include improved product quality, extended shelf life, reduced waste due to material degradation, and enhanced safety by minimizing the risk of fire or explosion in environments where flammable materials are present. Additionally, the sealed design helps in maintaining a controlled environment, which is crucial for compliance with industry regulations and standards.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design, development, and production of advanced material handling systems. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner in the industry, providing customized solutions tailored to the specific needs of clients. The company's headquarters is located in Shandong, China, where it leverages its expertise and state-of-the-art facilities to deliver high-performance nitrogen-protected material conveying lines and other related equipment. HeadPowder's team of engineers and technicians brings years of experience in material science and mechanical engineering, ensuring that each product meets the highest standards of performance and reliability. The company adheres to international quality management systems and continuously invests in research and development to stay at the forefront of technological advancements in material handling solutions.




