Recirculating coke powder pneumatic conveying systems are specialized industrial equipment designed to transport coke powder efficiently and safely. These systems are widely used in the chemical, metallurgical, and power generation industries, where the reliable handling of fine powders is critical for process efficiency and product quality. The primary function of such systems is to move coke powder from a storage or processing point to a destination, often with the capability to recirculate material to ensure consistent flow and prevent material degradation. Understanding the design principles behind these systems is essential for optimizing performance and ensuring long-term operational reliability.
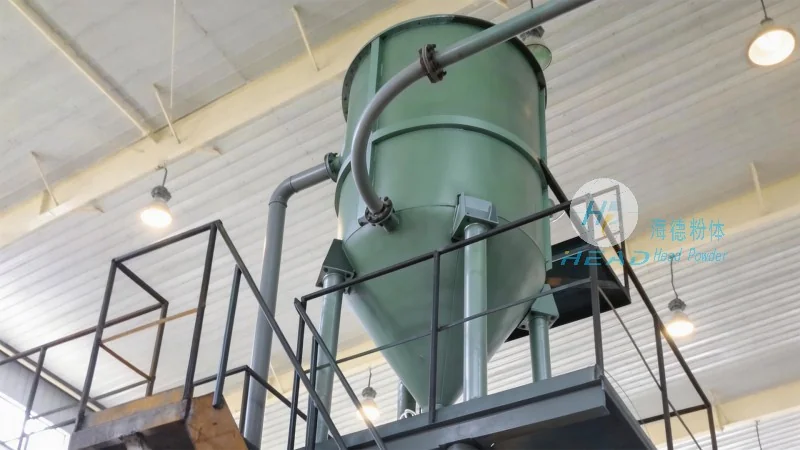
Introduction to Recirculating Coke Powder Pneumatic Conveying Systems
A recirculating coke powder pneumatic conveying system is a closed-loop system that uses compressed air or other gas to transport coke powder. Unlike traditional pneumatic conveying systems that may discharge material directly, recirculating systems incorporate a return loop to capture and re-introduce material that may have escaped or been lost during the conveying process. This design minimizes material loss, reduces dust emissions, and maintains a consistent material flow rate. The system typically consists of a hopper, a conveyor line, a receiver, and a recirculation mechanism, all working in tandem to ensure efficient material handling.
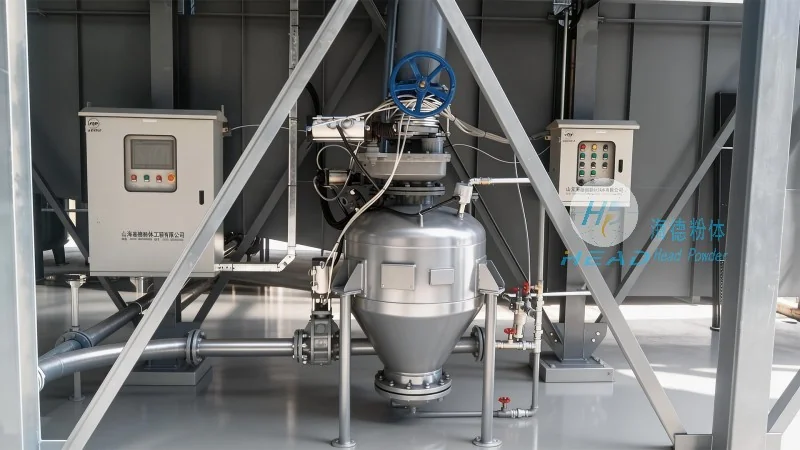
Key Design Principles of the System
The design of a recirculating coke powder pneumatic conveying system is governed by several critical principles to ensure optimal performance. First, the system must maintain a stable pressure and flow rate to prevent material segregation and ensure uniform particle distribution. This is achieved through the use of appropriate air velocities and pressure differentials. Second, the system incorporates a recirculation loop that captures excess material, often using a cyclone separator or a return duct, to maintain a consistent material inventory. Third, the design considers the physical properties of coke powder, such as particle size, density, and moisture content, to select the right air velocity and pressure for efficient transport. Additionally, the system is engineered to minimize pressure drop and energy consumption, making it cost-effective and environmentally friendly.
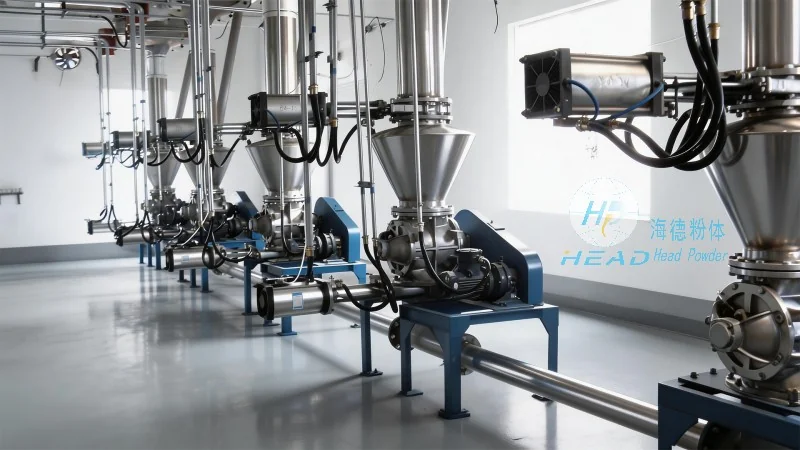
Components and Operational Mechanism
The core components of a recirculating coke powder pneumatic conveying system include a material hopper, a conveying pipeline, a receiver vessel, a compressor or blower, a recirculation unit, and a control system. The operation begins with coke powder being fed into the hopper from a storage silo. The compressor then generates compressed air, which is introduced into the conveying pipeline. As the air flows through the pipeline, it picks up the coke powder and transports it to the receiver. The receiver is designed to separate the powder from the air, typically using a cyclone or a bag filter. The separated powder is then collected in the receiver, while the air is either vented or recirculated back to the system. The recirculation unit captures any material that may have escaped and returns it to the hopper, ensuring a closed-loop operation. The control system monitors parameters such as pressure, flow rate, and material level, adjusting the system as needed to maintain optimal performance.
Advantages and Applications
Recirculating coke powder pneumatic conveying systems offer several advantages over traditional methods of material handling. These include reduced material loss, lower dust emissions, improved process control, and enhanced safety. The closed-loop design minimizes the risk of material contamination and environmental pollution, making it suitable for applications where material purity is critical. Additionally, the system can handle a wide range of particle sizes and moisture contents, making it versatile for various industrial processes. Common applications include the transport of coke powder in steel mills, chemical plants, and power generation facilities, where it is used as a fuel or raw material. The system's ability to maintain consistent material flow and prevent clogging makes it ideal for continuous production processes.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of industrial material handling equipment, including recirculating coke powder pneumatic conveying systems. The company is headquartered in Shandong, China, and has a strong reputation for delivering high-quality, reliable equipment tailored to the specific needs of its clients. HeadPowder's team of engineers and technicians has extensive experience in designing and manufacturing pneumatic conveying systems, ensuring that each product meets the highest standards of performance and durability. The company focuses on innovation and customer satisfaction, providing comprehensive solutions that enhance operational efficiency and reduce costs for its clients. With a commitment to quality and service, HeadPowder has established itself as a trusted partner in the industrial material handling industry.




