For industrial applications dealing with sodium bicarbonate, efficient and reliable powder handling is crucial. A specialized piece of equipment designed for this purpose is the sodium bicarbonate powder conveyor. This article explores what this equipment is and delves into its design principles, highlighting how it meets the demands of modern industrial processes.
About HeadPowder Engineering
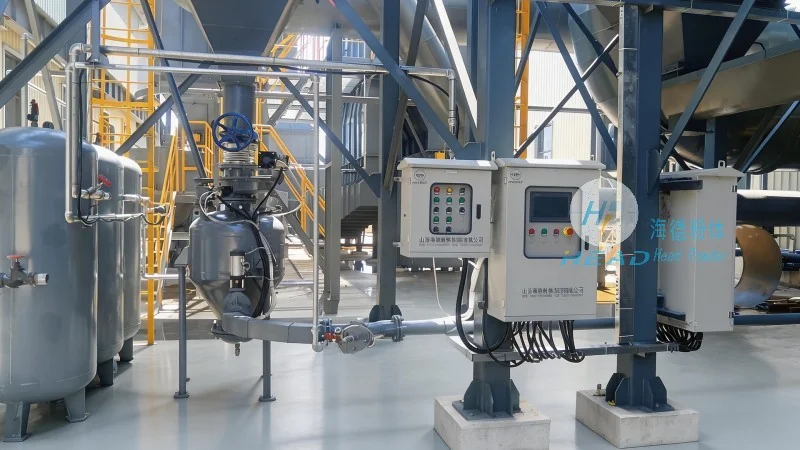
HeadPowder, the brand under Shandong HeadPowder Engineering Co., Ltd., specializes in engineering solutions for powder handling systems. With a focus on precision and durability, HeadPowder provides equipment tailored to the unique needs of industries that work with sodium bicarbonate and other fine powders. The company is headquartered in Shandong, China, and has built a reputation for delivering high-quality, customized conveyor systems that enhance operational efficiency and safety.
Design Principles of Sodium Bicarbonate Powder Conveyors
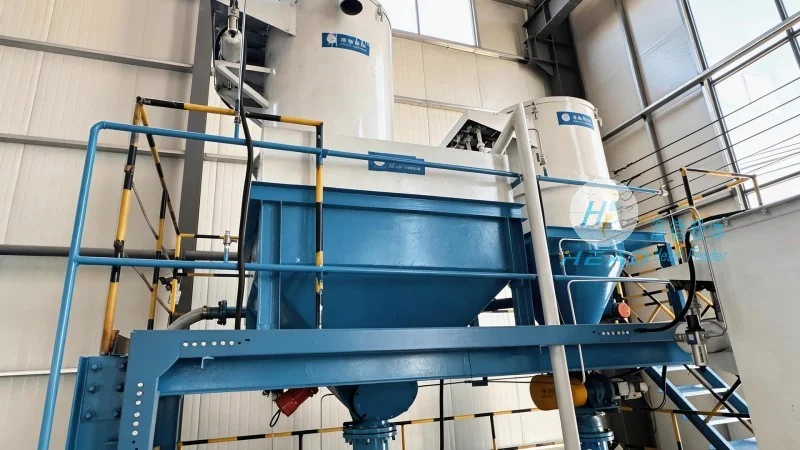
The design of a sodium bicarbonate powder conveyor is centered on several key principles to ensure optimal performance. First, the equipment must handle the physical properties of sodium bicarbonate, such as its flowability and potential for caking. Engineers design the conveyor with features like adjustable feed mechanisms and anti-caking systems to maintain consistent material flow. Second, the conveyor’s structure is built for durability, as it operates in environments where fine powders are handled regularly. Materials like stainless steel and corrosion-resistant components are commonly used to withstand the chemical and mechanical stresses associated with sodium bicarbonate processing. Third, the system is engineered for efficiency, minimizing energy consumption while maximizing throughput. This is achieved through optimized belt or screw designs, variable speed drives, and integrated control systems that allow for real-time monitoring and adjustment.
Key Features and Benefits
HeadPowder’s sodium bicarbonate powder conveyors are equipped with several features that enhance their functionality. These include adjustable speed controls, which allow operators to modulate the flow rate based on production requirements. The conveyors also feature easy-to-clean designs, reducing downtime for maintenance and ensuring compliance with hygiene standards. Additionally, the systems are designed with safety in mind, incorporating features like emergency stop buttons and overload protection to prevent accidents and equipment damage. The benefits of using such a conveyor include improved process efficiency, reduced material waste, and enhanced safety for operators.
Conclusion
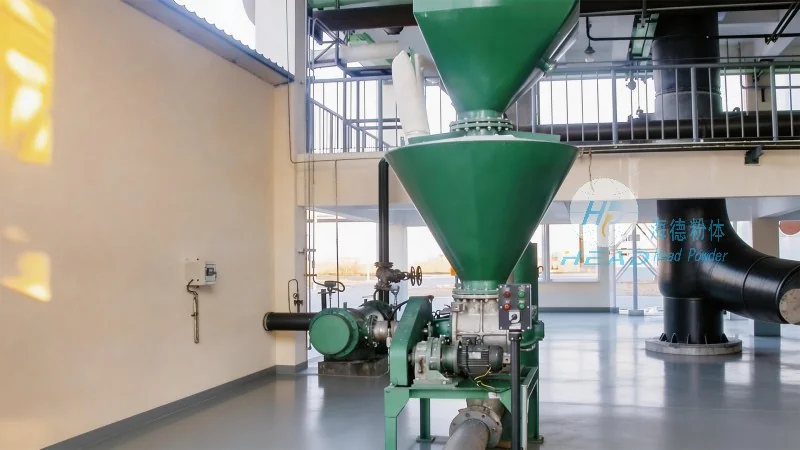
Sodium bicarbonate powder conveyors are essential equipment for industries that rely on the consistent and safe handling of this fine powder. By understanding the design principles behind these systems, businesses can make informed decisions about their material handling solutions. HeadPowder Engineering, with its expertise in powder handling technology, offers reliable and efficient conveyors that meet the specific needs of sodium bicarbonate processing, ensuring optimal performance and long-term operational success.




