When it comes to efficiently transporting small gravel and similar materials in industrial or construction settings, specialized equipment is essential. A small gravel material handling system is a tailored solution designed to move these materials from one location to another with precision and reliability. Understanding what this system entails and its underlying design principles is crucial for anyone involved in material handling operations.
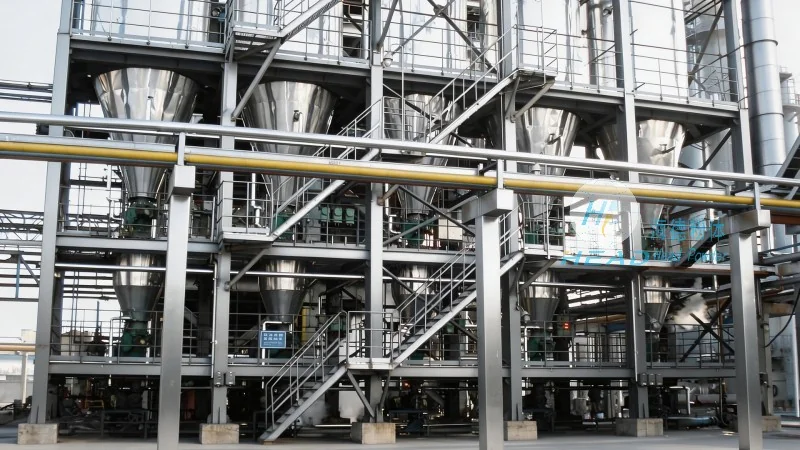
Introduction to Small Gravel Material Handling Systems
A small gravel material handling system is a comprehensive setup that includes various components such as conveyors, feeders, and control mechanisms. These systems are specifically engineered to handle small, irregularly shaped materials like gravel, crushed stone, or similar bulk materials. The primary goal is to ensure smooth and efficient material flow, minimizing downtime and maximizing productivity in applications like construction sites, mining operations, or recycling facilities.
Key Components of a Small Gravel Material Handling System
The effectiveness of a small gravel material handling system largely depends on its key components. Each part plays a vital role in the overall operation. For instance, conveyors are often used to transport the material over long distances, while feeders regulate the flow rate to prevent overloading or bottlenecks. Control systems, including sensors and automation devices, ensure that the system operates safely and efficiently, adapting to changes in material volume or process requirements.
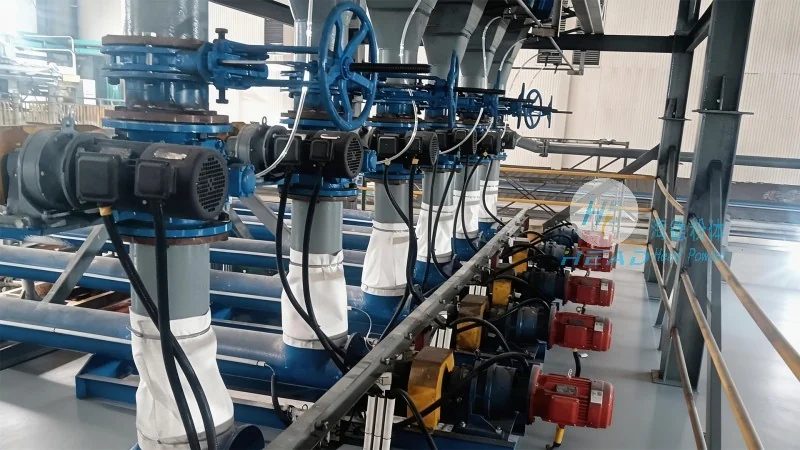
Design Principles for Optimal Performance
The design of a small gravel material handling system follows several fundamental principles aimed at achieving optimal performance. First, the system must be robust and durable to withstand the abrasive nature of small gravel, which can cause wear and tear on equipment. Second, it should be flexible enough to accommodate different material sizes and types, allowing for adaptability in various applications. Third, energy efficiency is a critical consideration, as minimizing power consumption reduces operational costs and environmental impact. Finally, safety is paramount, with features like emergency stop buttons and protective guards to prevent accidents and ensure compliance with industrial safety standards.
Application Scenarios and Benefits
Small gravel material handling systems are widely used in various industries where bulk material transport is necessary. In construction, they help move gravel for road base or landscaping projects. In mining, they assist in transporting crushed ore or rock. The benefits of such systems include increased operational efficiency, reduced labor costs, and improved safety for workers. By automating the material handling process, these systems also minimize human error and enhance overall productivity.
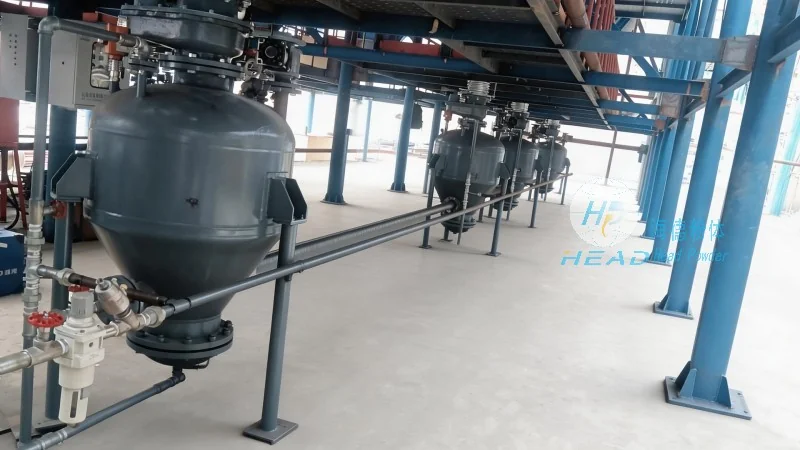
HeadPowder Engineering's Expertise in Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in providing high-quality material handling systems tailored to meet diverse industrial needs. With years of experience in the field, HeadPowder understands the unique challenges of handling small gravel and has developed innovative solutions that combine durability, efficiency, and safety. The company's commitment to using advanced technology and quality materials ensures that their systems deliver reliable performance in demanding environments.
Conclusion: Choosing the Right Material Handling System
Selecting the appropriate small gravel material handling system requires careful consideration of operational needs, material characteristics, and budget constraints. By understanding the design principles and components of such systems, as well as the expertise of manufacturers like HeadPowder, businesses can make informed decisions that enhance their material handling capabilities. Ultimately, a well-designed and well-executed material handling system not only improves efficiency but also contributes to long-term operational success.




