Clay coal powder material handling systems are specialized industrial solutions designed to transport and manage clay coal powder efficiently. These systems are crucial in various industrial applications, particularly in the mining, power generation, and chemical processing sectors, where the safe and reliable movement of fine, abrasive, and potentially explosive materials is essential. Understanding the components and design principles of such systems is vital for optimizing operational efficiency and ensuring compliance with safety standards.
Defining the Clay Coal Powder Material Handling System
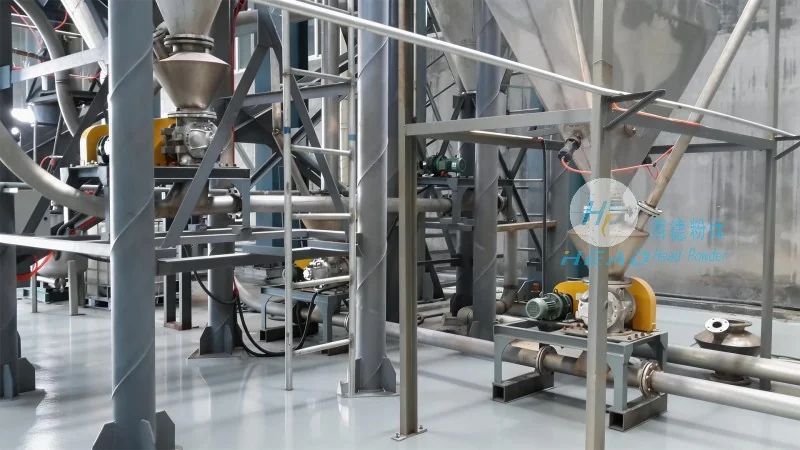
A clay coal powder material handling system encompasses a range of equipment and processes tailored to handle clay coal powder, a type of coal characterized by its fine particle size and high moisture content. The system typically includes feeders, conveyors, storage silos, and control mechanisms that work in tandem to transport the material from its source to processing or storage locations. The primary goal of these systems is to minimize material loss, prevent dust generation, and maintain consistent flow rates, which are critical for downstream processes like combustion or further processing.
Key Design Principles for Efficient Material Handling
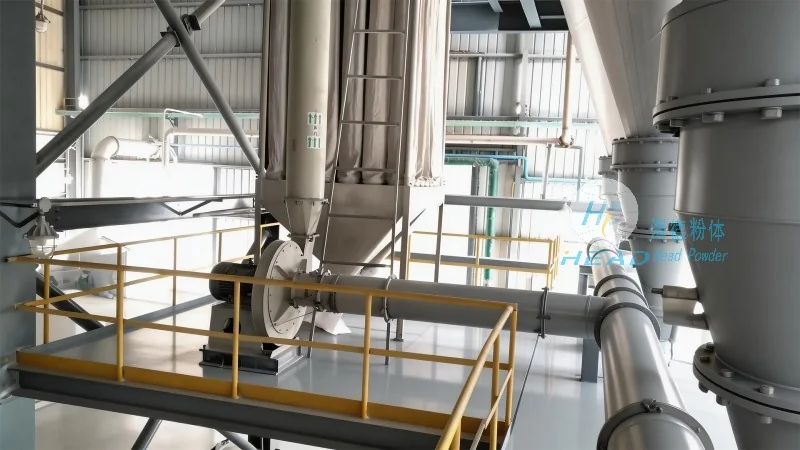
The design of a clay coal powder material handling system is guided by several fundamental principles aimed at maximizing performance, safety, and durability. One of the most critical principles is the prevention of material buildup and blockages, which can occur due to the cohesive nature of clay coal powder. Engineers employ anti-stick coatings, vibration mechanisms, and appropriate material flow angles to ensure smooth material movement. Another key principle is the management of dust and air quality, as clay coal powder is often fine and can create hazardous dust clouds. The system incorporates dust collection and filtration systems to maintain a safe working environment and comply with environmental regulations.
Core Components and Their Functions
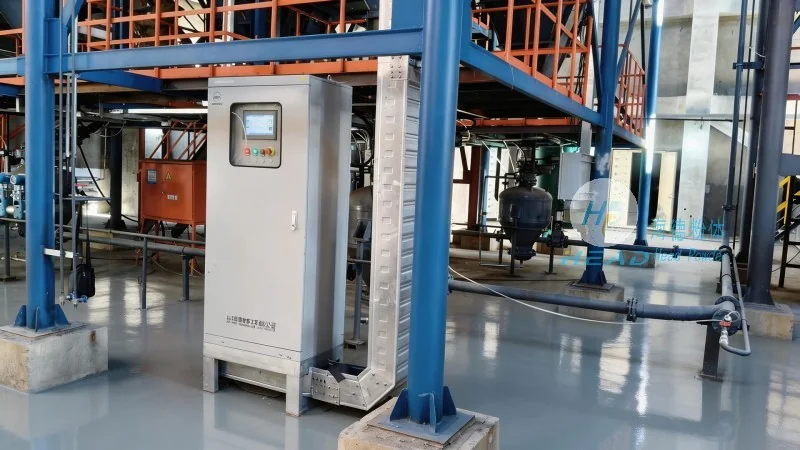
The effectiveness of a clay coal powder material handling system relies on its integrated components, each serving a specific function to ensure optimal operation. Feeders, such as rotary or vibratory feeders, are used to regulate the flow of clay coal powder from the source, ensuring a consistent feed rate to downstream equipment. Conveyors, including pneumatic or mechanical types, transport the material over long distances with minimal loss. Storage silos are designed to hold large quantities of the material, with features like agitators to prevent caking and maintain flowability. Control systems, often integrated with sensors and automation, monitor parameters like pressure, flow rate, and temperature, allowing for real-time adjustments to maintain system efficiency and safety.
Technological Advancements and Material Handling Solutions
Modern clay coal powder material handling systems leverage advanced technologies to enhance performance and reliability. For instance, the use of high-capacity pneumatic conveying systems allows for the transport of fine powders over extended distances without the need for mechanical components that could cause wear or blockages. Additionally, the integration of sensors and IoT (Internet of Things) technologies enables predictive maintenance, reducing downtime and maintenance costs. These advancements ensure that the system operates efficiently while adhering to stringent safety and environmental standards.
Application in Industrial Sectors
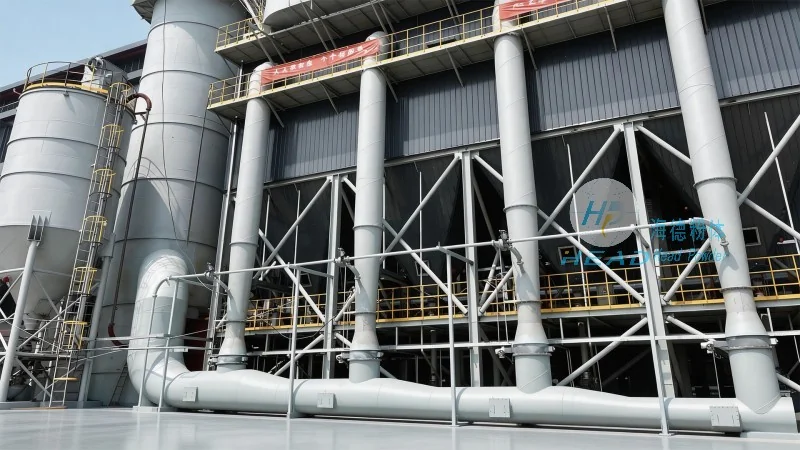
Clay coal powder material handling systems find extensive applications in various industrial sectors. In the power generation industry, these systems are used to feed coal into boilers, where the consistent supply of fine coal powder is essential for efficient combustion and power production. In the chemical processing industry, the systems help transport coal to reactors for further processing, ensuring a stable supply of raw material. The mining industry also utilizes these systems for transporting coal from mines to processing facilities, improving overall operational efficiency.
Ensuring Safety and Compliance
Given the potential hazards associated with clay coal powder, such as dust explosions and material handling risks, safety is a paramount consideration in system design. Engineers incorporate features like explosion-proof designs, dust suppression systems, and emergency shutdown mechanisms to mitigate risks. Additionally, the system adheres to international safety standards and environmental regulations, ensuring that it operates in a safe and sustainable manner. This focus on safety not only protects personnel but also maintains the system's operational integrity over time.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing clay coal powder material handling systems tailored to meet the unique needs of industrial clients. With a strong commitment to innovation and quality, the company leverages advanced engineering principles and cutting-edge technologies to deliver reliable and efficient systems. HeadPowder's expertise in material handling ensures that clients receive solutions that enhance operational efficiency, reduce costs, and comply with industry standards. The company's focus on customer satisfaction and long-term partnerships has established it as a trusted name in the material handling industry.




