

Desulfurization Sodium Bicarbonate Material Handling System Equipment: What It Is and Its Design Pri
Desulfurization processes in modern industrial applications often require specialized equipment to handle sodium bicarbonate, a key reagent used in flue gas desulfurization. The desulfurization sodium bicarbonate material handling system equipment is a critical component designed to efficiently transport and manage this material within industrial facilities. This equipment ensures the safe and effective operation of desulfurization systems, which are vital for reducing sulfur dioxide emissions and improving air quality.
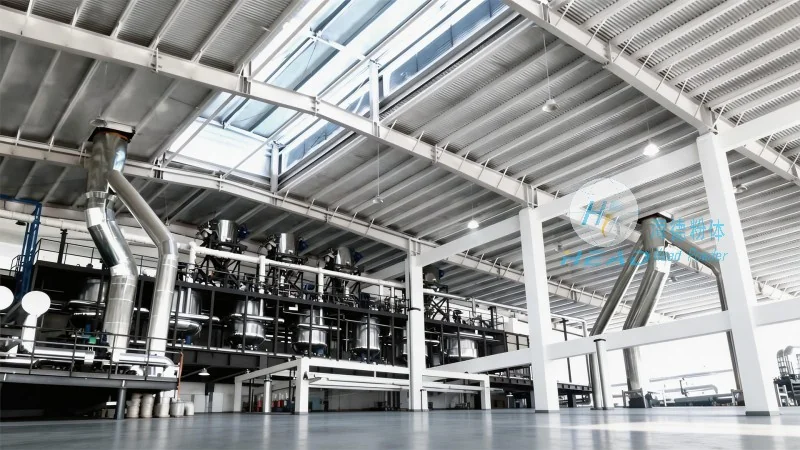
Understanding the Core Components of the Material Handling System
The desulfurization sodium bicarbonate material handling system typically consists of several interconnected components that work together to facilitate material transport. These components may include hoppers, conveyors, storage silos, and feeding mechanisms. Each part plays a specific role in the overall system, ensuring that sodium bicarbonate is moved from storage to the point of use in a controlled and efficient manner. The system is engineered to handle the unique properties of sodium bicarbonate, such as its granular or powder form, and to maintain the material's integrity during transport.
Design Principles for Efficient Material Handling
The design of the desulfurization sodium bicarbonate material handling system is guided by several key principles aimed at optimizing performance and reliability. One of the primary principles is the minimization of material degradation during transport. This is achieved through the use of appropriate conveyor types, such as belt conveyors or screw conveyors, which are selected based on the material's characteristics and the system's operational requirements. Additionally, the system is designed to ensure uniform flow and prevent blockages, which can lead to system inefficiencies or safety hazards. The integration of sensors and control systems further enhances the system's ability to monitor and adjust material flow in real-time, ensuring consistent operation.
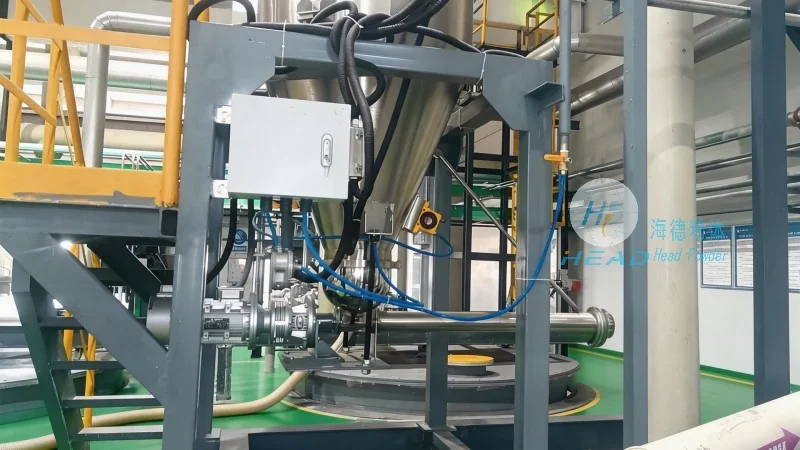
Application in Flue Gas Desulfurization
In the context of flue gas desulfurization, the desulfurization sodium bicarbonate material handling system is integral to the overall process. Sodium bicarbonate is used as an absorbent in wet desulfurization processes, where it reacts with sulfur dioxide to form calcium carbonate or other byproducts. The material handling system ensures that sodium bicarbonate is delivered to the desulfurization reactor at the correct rate and in the right form, which directly impacts the efficiency of the sulfur dioxide removal process. Proper material handling also contributes to the longevity of the desulfurization equipment by preventing wear and tear caused by uneven or abrasive material flow.
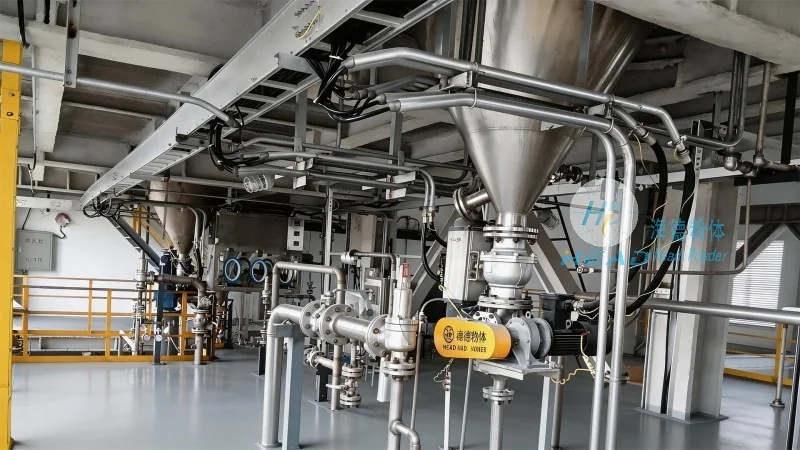
Key Features and Advantages of the System
The desulfurization sodium bicarbonate material handling system offers several advantages that make it a preferred choice for industrial applications. These include high capacity and reliability, which are essential for continuous operation in demanding environments. The system is also designed for easy maintenance and cleaning, reducing downtime and operational costs. Furthermore, the use of durable materials and robust construction ensures that the equipment can withstand the corrosive and abrasive conditions often encountered in desulfurization processes. The integration of safety features, such as emergency stop mechanisms and material flow monitoring, further enhances the system's safety and operational reliability.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of specialized industrial equipment, including desulfurization sodium bicarbonate material handling systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in the chemical and environmental industries. HeadPowder's facilities are located in Shandong, China, where the company leverages advanced manufacturing technologies and a skilled workforce to produce high-performance equipment tailored to the specific needs of its clients. The company's products are designed to meet international standards and are backed by comprehensive technical support and after-sales services, ensuring that customers receive reliable and efficient solutions for their material handling requirements.