HeadPowder, a leading provider of industrial material handling solutions, specializes in advanced pneumatic conveying systems. Based in Shandong, China, the company offers innovative technologies for efficient material transport, including silo pump systems designed for diverse industrial applications. This article explores the working principle and key characteristics of silo pump material pneumatic conveying, highlighting how these systems enhance operational efficiency and reliability in material handling processes.
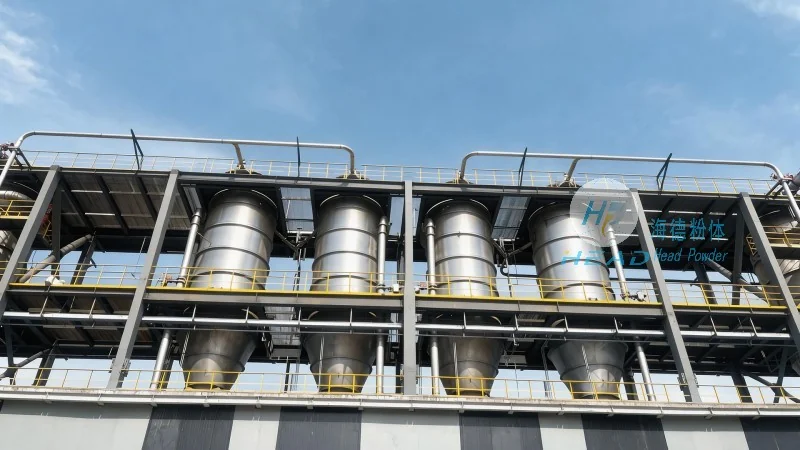
Company Introduction
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier of industrial material handling equipment. With a focus on research and development, the company delivers high-quality solutions tailored to meet the specific needs of various industries. HeadPowder's expertise lies in designing and manufacturing advanced pneumatic conveying systems, including silo pumps, that ensure safe, efficient, and reliable material transport. The company's commitment to innovation and customer satisfaction has established it as a trusted partner in the material handling sector.
Working Principle of Silo Pump Material Pneumatic Conveying
The silo pump material pneumatic conveying system operates on the principle of air-assisted material transport. The process begins with the loading of bulk materials into the silo pump hopper. Once the hopper is filled, the system uses compressed air to create a low-pressure environment inside the pump. This pressure differential draws the material from the hopper into the pump chamber. As the pump rotates or moves, the material is mixed with the air stream, forming a slurry-like mixture. The air and material mixture is then forced through the conveying pipeline to the destination silo or processing unit. The system typically includes a control panel that regulates air pressure, flow rate, and material feed, ensuring precise and controlled transport. The entire process is automated, minimizing human intervention and maximizing operational efficiency.
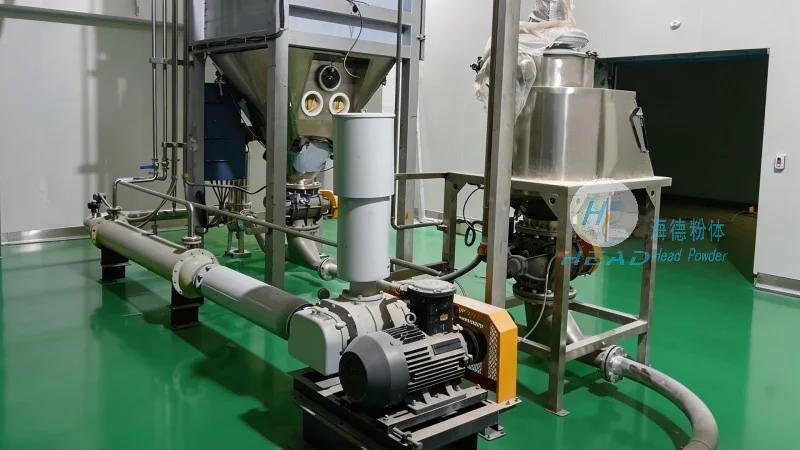
Key Characteristics of Silo Pump Material Pneumatic Conveying
Silo pump material pneumatic conveying systems offer several distinct advantages that make them ideal for industrial applications. Firstly, they provide high conveying efficiency, capable of transporting large volumes of materials over long distances with minimal energy consumption. The system's flexibility allows for the handling of various material types, including powders, granules, and bulk solids, without the need for additional equipment like conveyors or elevators. Secondly, the system is highly reliable and durable, with components designed to withstand the rigors of continuous operation. The use of compressed air reduces wear and tear on mechanical parts, extending the lifespan of the equipment. Additionally, silo pump systems are safe and environmentally friendly, as they eliminate the need for manual handling of materials, reducing the risk of accidents and minimizing dust emissions. The automated control system ensures consistent performance, with real-time monitoring of pressure, flow, and material levels, allowing for quick adjustments and maintenance. These characteristics make silo pump material pneumatic conveying a preferred choice for industries such as chemical, food, pharmaceutical, and mining, where material transport efficiency and safety are paramount.
Applications and Benefits
The versatility of silo pump material pneumatic conveying systems makes them suitable for a wide range of applications. In the chemical industry, these systems are used to transport raw materials and finished products, ensuring seamless integration into production lines. The food and pharmaceutical sectors benefit from the system's ability to handle sensitive materials without contamination, maintaining product quality and safety standards. The mining industry utilizes silo pumps to transport ore and other bulk materials from storage silos to processing facilities, improving operational flow and reducing downtime. The primary benefits of using silo pump systems include increased productivity, reduced labor costs, improved material handling safety, and enhanced environmental compliance. By automating the material transport process, companies can achieve higher throughput, lower operational costs, and better overall operational performance. The reliability of the system also minimizes the risk of material loss or spillage, contributing to cost savings and improved efficiency.
Conclusion
HeadPowder's silo pump material pneumatic conveying systems represent a cutting-edge solution for industrial material handling. By leveraging advanced pneumatic technology, these systems provide efficient, reliable, and safe transport of bulk materials. The working principle, which combines compressed air with mechanical movement, ensures consistent performance and minimal maintenance. The key characteristics, including high efficiency, flexibility, and durability, make silo pump systems an ideal choice for various industrial applications. With a commitment to quality and innovation, Shandong HeadPowder Engineering Co., Ltd. continues to deliver solutions that meet the evolving needs of the material handling industry. The adoption of silo pump material pneumatic conveying not only enhances operational efficiency but also contributes to cost savings and improved safety in industrial processes.




