Shandong HeadPowder Engineering Co., Ltd., a specialized provider of material handling solutions, focuses on air-driven transport technologies for fine coal powder materials. The company is headquartered in Shandong, China, and delivers efficient systems tailored to industrial material transport needs.
Working Principle of Air-Driven Transport for Fine Coal Powder Materials
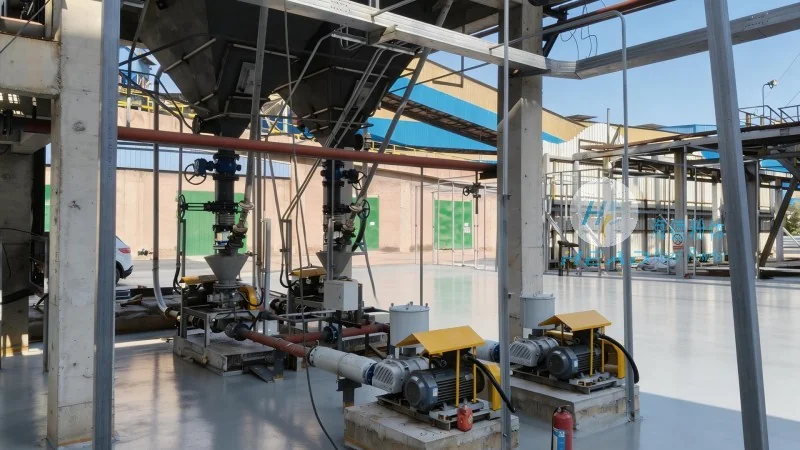
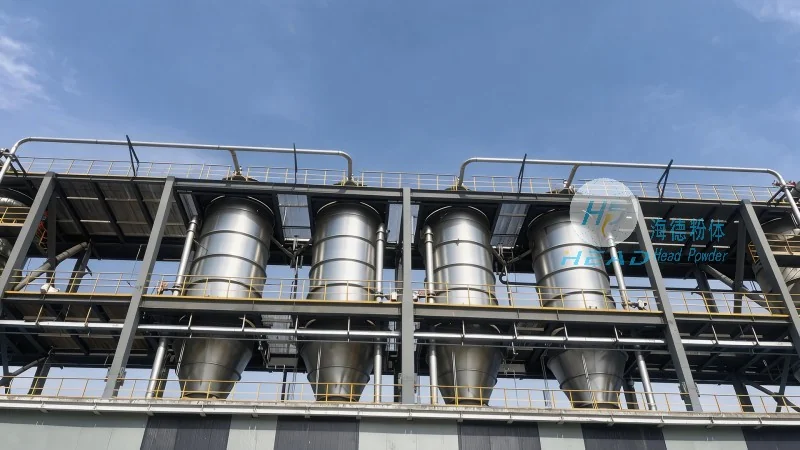
The air-driven transport system operates by utilizing a pneumatic mechanism to move fine coal powder particles through a pipeline. The process initiates with the material being fed into a hopper or feeder, where it is then introduced into the transport line. As pressurized or suction air flows through the pipeline, it creates a flow that carries the powder particles along. This method relies on the interaction between the air flow and the particles, ensuring stable and continuous transport without the need for mechanical components like belts or buckets. The system can be configured as a pressure system, where air is supplied to the pipeline to push the material, or as a suction system, where air is drawn to pull the material. Both configurations are designed to handle fine powders effectively, maintaining particle integrity and preventing blockages.
Key Characteristics of Air-Driven Transport for Fine Coal Powder Materials
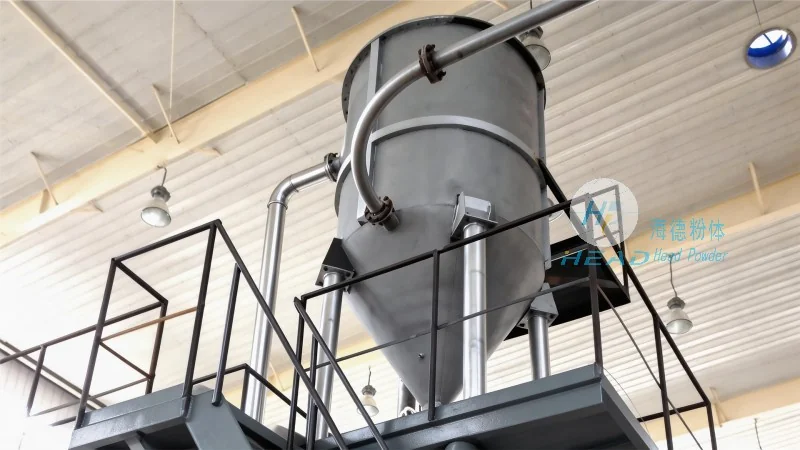
One of the primary advantages of this air-driven transport system is its high efficiency in material handling. The pneumatic mechanism allows for rapid and continuous transport of fine coal powder, reducing downtime and increasing production throughput. Additionally, the system requires minimal maintenance due to the absence of moving parts, which are common sources of wear and tear in traditional mechanical transport systems. This leads to lower operational costs and longer equipment lifespan. The flexibility of the pipeline layout is another significant characteristic, as the system can be adapted to various industrial setups, including vertical, horizontal, or combined vertical-horizontal transport. This adaptability makes it suitable for a wide range of applications, from small-scale processing to large-scale industrial operations. Furthermore, the transport process is inherently dust-free, which is critical for maintaining a safe working environment and complying with environmental regulations. The ability to adjust transport speed according to process requirements ensures optimal performance, allowing for precise control over material flow rates. This control is essential for maintaining consistent product quality and meeting specific industrial standards.
Applications and Benefits in Industrial Settings
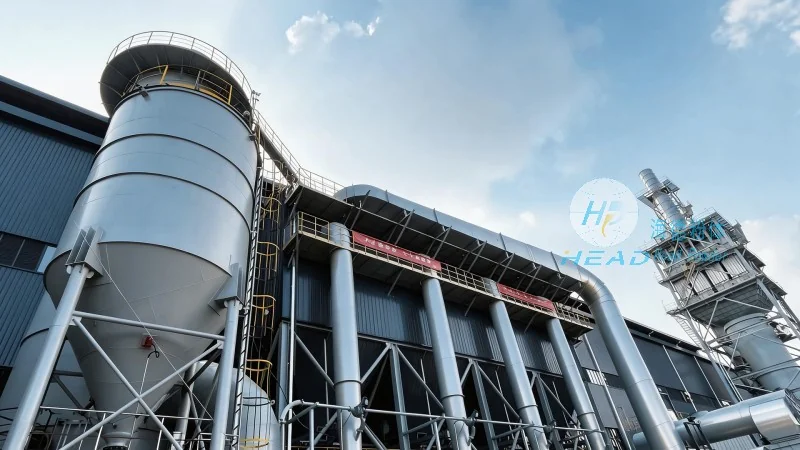
The air-driven transport system for fine coal powder materials is widely used in various industrial sectors, including power generation, cement production, and chemical processing. In power plants, it is used to transport coal from storage to boilers, ensuring a steady supply of fuel. In cement factories, it facilitates the transport of raw materials and finished products, improving overall production efficiency. The benefits of this system extend beyond efficiency and maintenance, as it also contributes to improved safety and environmental compliance. The dust-free operation reduces the risk of respiratory issues among workers and minimizes the impact on the environment. Moreover, the system's ability to handle fine powders without agglomeration ensures that the material remains in a consistent state, which is crucial for downstream processing steps. Overall, the air-driven transport system offers a reliable and cost-effective solution for handling fine coal powder materials, meeting the demands of modern industrial operations.




