HeadPowder, a leading provider of industrial material handling solutions, specializes in designing and manufacturing efficient pneumatic conveying systems tailored for large-scale bulk material transport. The tonne bag pneumatic conveying line is a critical component in modern logistics and processing facilities, enabling the safe and reliable movement of bulk materials from storage to processing or packaging areas. This article explores the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in various industrial applications.
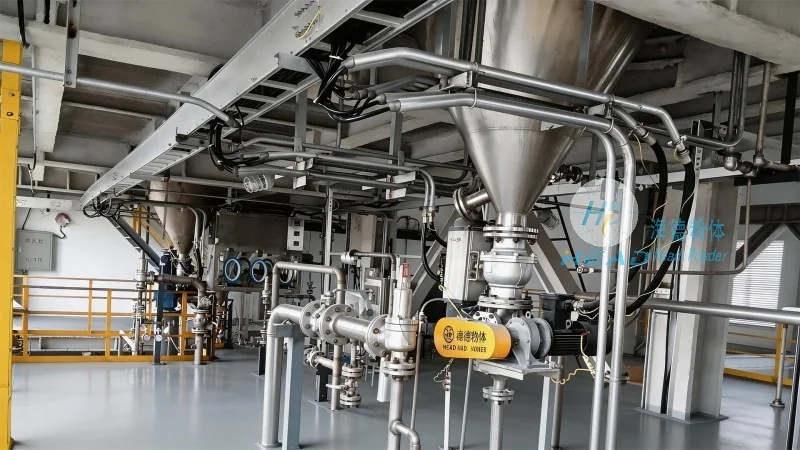
Principle of Tonne Bag Pneumatic Conveying
The core principle of a tonne bag pneumatic conveying line is the use of compressed air or gas to create a flow that transports bulk materials through a pipeline. Unlike mechanical conveying systems that rely on belts, buckets, or screws, pneumatic systems utilize air pressure to move materials, which is particularly advantageous for handling powders, granules, and other free-flowing or semi-free-flowing bulk solids. The process typically involves several key components: a hopper or storage container to hold the tonne bag, a feeder to control the material flow, a conveying line (often made of stainless steel or other corrosion-resistant materials), and a receiver or discharge point where the material is deposited. The system operates by introducing air into the conveying line, creating a low-pressure zone that draws material from the hopper into the pipeline. As the air and material mixture travels through the line, the material is propelled forward by the air flow, reaching the destination point efficiently. The design of the system, including the air velocity, pipe diameter, and system layout, is crucial for ensuring optimal performance and minimizing material degradation or blockages.
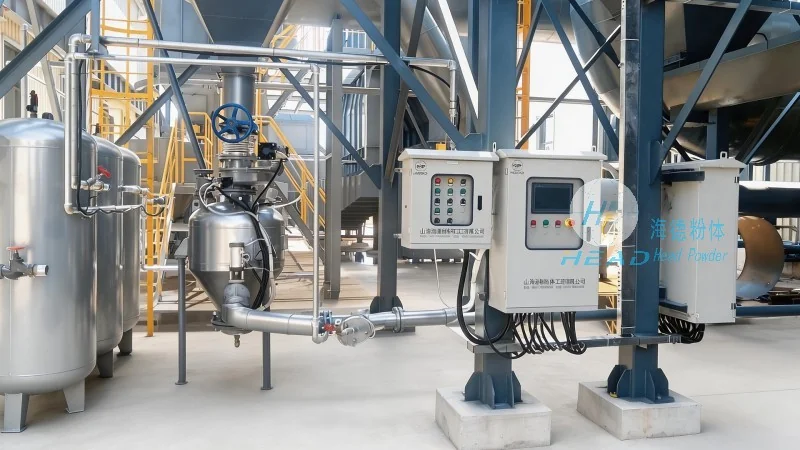
Key Working Scene Characteristics
The tonne bag pneumatic conveying line is characterized by several distinct working scene features that enhance its suitability for specific industrial environments. First, its ability to handle large volumes of material in a continuous or semi-continuous manner makes it ideal for high-throughput operations, such as in mining, cement, and chemical industries where large quantities of bulk solids need to be transported over short or medium distances. Second, the system’s flexibility in terms of layout allows for integration into existing facilities without major structural modifications, as the conveying line can be installed horizontally, vertically, or at an angle, adapting to the spatial constraints of the working environment. Third, the enclosed nature of the system helps maintain material integrity and prevents contamination, which is vital for products that require strict quality control, such as food, pharmaceuticals, or fine chemicals. Additionally, the system’s low maintenance requirements and energy efficiency contribute to its operational advantages, reducing downtime and operational costs for industrial facilities. The working scene characteristics also include the system’s ability to handle a wide range of material types, from fine powders to coarse granules, and its adaptability to different tonne bag sizes and material densities, ensuring versatility across various industrial applications.
Applications and Operational Advantages
HeadPowder’s tonne bag pneumatic conveying lines are widely used in diverse industrial sectors, including mining, cement production, chemical processing, food and beverage, and pharmaceuticals. In mining operations, these systems efficiently transport ore from storage silos to processing plants, ensuring a steady supply of raw materials. In the cement industry, they facilitate the movement of raw materials and finished products between storage and production lines, improving production efficiency. In chemical processing, the systems handle various chemicals and powders, maintaining safety and compliance with industry regulations. The operational advantages of these systems include high material throughput, minimal material degradation, and reduced labor costs compared to manual handling methods. Furthermore, the enclosed design of the system minimizes dust emissions, contributing to a safer working environment and compliance with environmental regulations. The reliability of the system, with its robust components and advanced control systems, ensures consistent performance and reduces the risk of downtime, which is critical for maintaining production schedules and meeting customer demands.
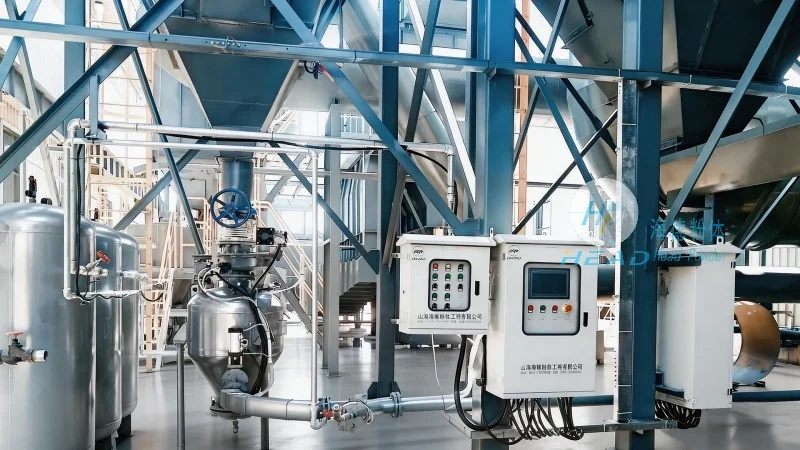
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted manufacturer of tonne bag pneumatic conveying lines, providing customized solutions that meet the unique needs of industrial clients. With a focus on innovation and quality, the company designs systems that combine efficiency, reliability, and safety, ensuring optimal performance in various working scenarios. The principles and characteristics of tonne bag pneumatic conveying lines, as outlined in this article, highlight their importance in modern industrial material handling, offering a cost-effective and efficient solution for bulk material transport. By leveraging advanced engineering and manufacturing techniques, HeadPowder continues to deliver high-performance pneumatic conveying systems that enhance operational efficiency and support the growth of industrial facilities worldwide.




