For industries that require high-purity material handling, such as pharmaceuticals, food processing, and fine chemicals, maintaining a clean and dust-free environment is paramount. The small bag dust-free feeding station with pneumatic conveying line offers an efficient solution to handle bulk materials while preserving product integrity and operational safety. This system is designed to minimize dust generation and contamination, ensuring compliance with stringent industry standards.
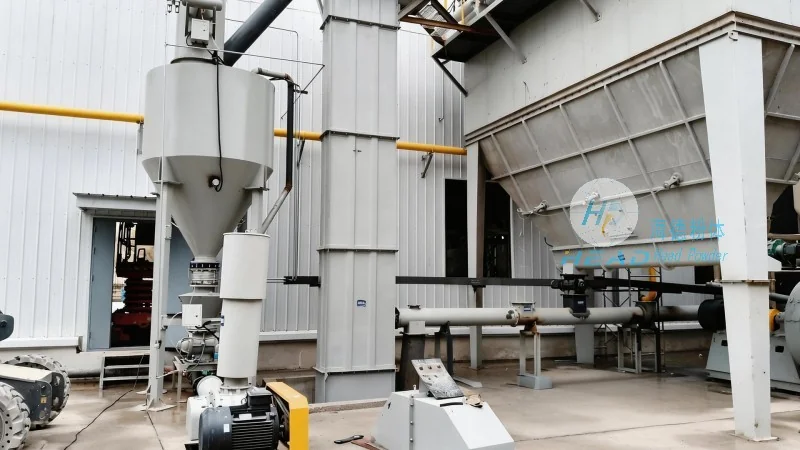
Company Overview: HeadPowder Engineering
HeadPowder Engineering, a leading provider of material handling solutions, specializes in developing advanced pneumatic conveying systems tailored to diverse industrial needs. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the field. Based in Shandong, China, HeadPowder Engineering leverages its expertise to deliver reliable and efficient equipment that meets the highest operational requirements.
Principle of Pneumatic Conveying
The core of the small bag dust-free feeding station is the pneumatic conveying technology, which utilizes air to transport bulk materials from storage bags to processing equipment. The system operates by creating a pressure differential between the feeding station and the destination point. When the storage bag is opened, material is drawn into the conveying line through a hopper and an airlock mechanism. The airlock ensures a controlled flow of material, preventing backflow and maintaining a consistent feed rate. The conveying air is filtered and cleaned to eliminate dust particles, ensuring that the material remains free from contamination throughout the process.
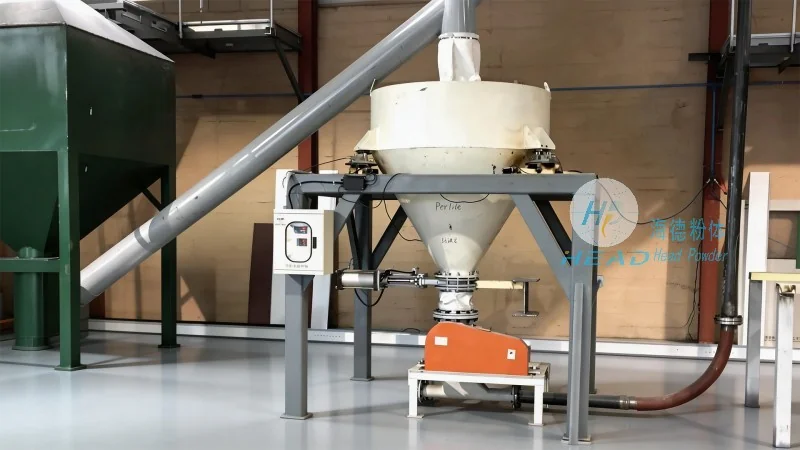
Key Features of the Dust-Free Feeding Station
One of the standout features of this system is its dust-free design. The feeding station incorporates sealed hoppers and airlock valves that prevent dust from escaping into the environment. This not only enhances workplace safety but also protects the material from external contaminants. Additionally, the system is equipped with advanced filtration systems that capture any airborne particles, ensuring that the exhaust air is clean and compliant with environmental regulations. The compact design of the feeding station makes it suitable for installation in confined spaces, optimizing factory layouts.
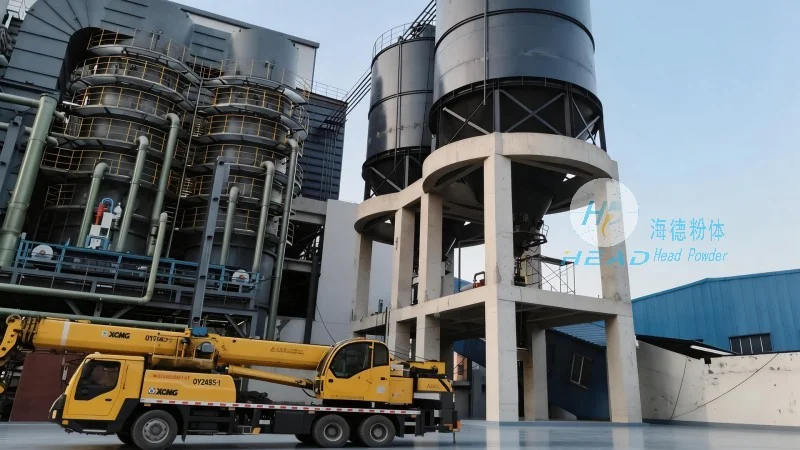
Working Scene Characteristics
The small bag dust-free feeding station is particularly well-suited for applications where material purity and process efficiency are critical. In pharmaceutical manufacturing, for example, the system ensures that active pharmaceutical ingredients (APIs) are handled without contamination, maintaining the quality of final products. In food processing, the dust-free design prevents cross-contamination between different product lines, meeting stringent food safety standards. The system’s ability to handle various materials, including powders, granules, and fine particles, makes it versatile for different industrial applications.
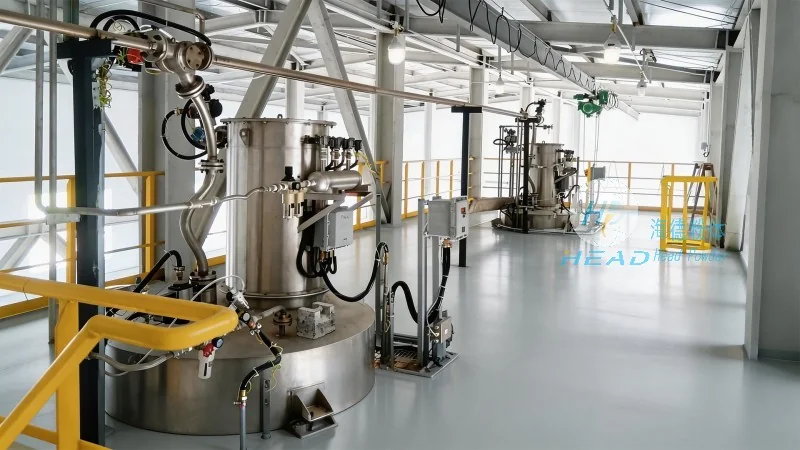
Efficiency and Operational Benefits
Implementing a pneumatic conveying line with a dust-free feeding station offers several operational advantages. The system reduces material handling time compared to traditional methods, such as manual bagging or bucket conveyors. By automating the feeding process, it minimizes human error and labor costs. The consistent feed rate ensures that processing equipment operates at optimal efficiency, reducing downtime and increasing overall productivity. Furthermore, the sealed design reduces the need for frequent cleaning and maintenance, lowering operational costs over the long term.
Application Examples
HeadPowder Engineering has successfully implemented this system in various industries. In a pharmaceutical plant, the small bag dust-free feeding station was used to handle active ingredients, ensuring that the final drug products met purity standards. In a food processing facility, the system was integrated to transport flour and other dry ingredients, maintaining food safety and preventing dust accumulation. These real-world applications demonstrate the system’s reliability and effectiveness in diverse operational environments.




