Intelligent tonne bag loading stations with integrated material conveying systems have revolutionized the way bulk materials are handled in industrial settings. These advanced systems are engineered to efficiently transfer materials from large tonne bags into processing equipment or storage facilities, offering significant improvements in operational efficiency, safety, and cost-effectiveness. The core functionality of such a system revolves around automating the material transfer process, minimizing manual labor, and ensuring consistent material flow rates, which are critical for maintaining production quality and throughput.
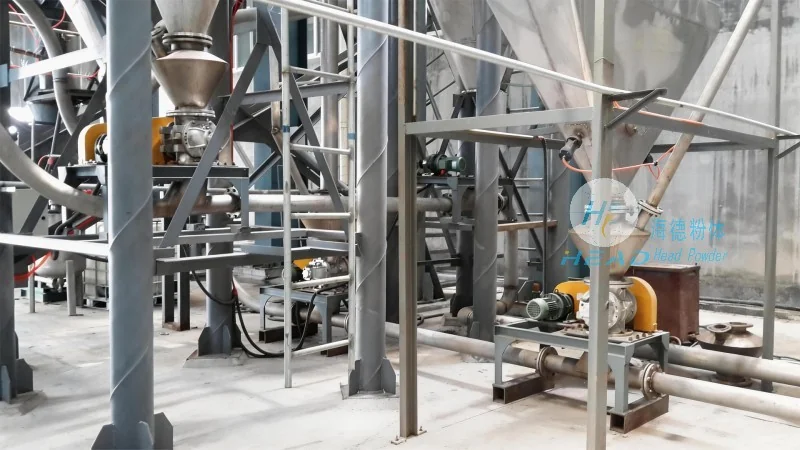
System Principle: Comprehensive Automation and Control
The intelligent tonne bag loading station material conveying system operates on a principle of comprehensive automation, integrating mechanical, electrical, and control technologies to manage the entire material handling process. The system typically includes a hopper or feeding chute that receives material from the tonne bag, followed by a discharge mechanism such as a valve or gate to control the flow of material. A conveyor system, often a belt or screw conveyor, then transports the material to the target location, such as a mixer, crusher, or storage silo. Advanced control systems, equipped with sensors and programmable logic controllers (PLCs), monitor and regulate the entire process. These systems can detect bag weight, material level, and conveyor status, adjusting flow rates and operational parameters in real-time. This level of automation ensures precise control over material transfer, reduces the risk of overfilling or underfilling, and enhances overall system reliability. Additionally, safety features like emergency stop buttons, overload protection, and interlocks are integrated to comply with industrial safety standards and prevent accidents during operation.
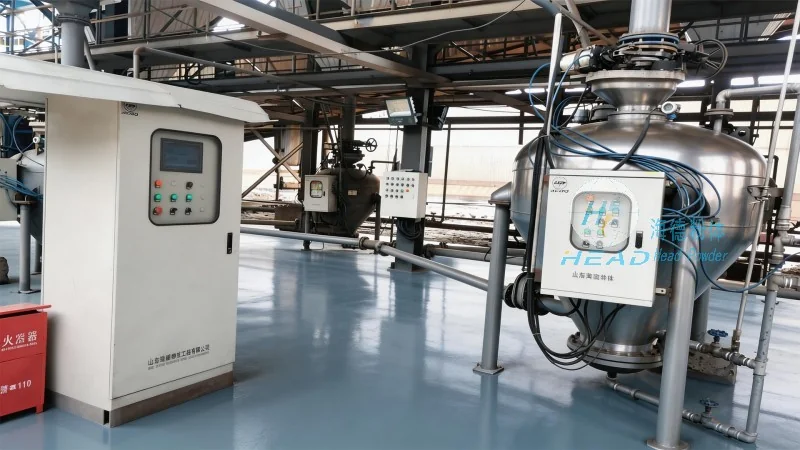
Working Scene Characteristics: Tailored for Industrial Applications
The working scene characteristics of these systems are designed to accommodate diverse industrial applications, particularly in sectors like mining, chemicals, food processing, and construction. The systems are built to handle high-volume material flows, with throughput capabilities that can range from several tons per hour to over 100 tons per hour, depending on the specific configuration. Their durability and robust construction allow them to operate in harsh industrial environments, withstanding dust, moisture, and heavy-duty conditions. The stations are typically installed in feed points of production lines, where bulk materials need to be efficiently transferred into processing equipment. Key characteristics include adaptability to different material types, such as powders, granules, or bulk solids, and the ability to handle varying bag sizes and materials. The integration of automated bag handling, including bag placement, opening, and emptying, further enhances operational efficiency, especially in high-demand production scenarios. These systems are also designed for easy maintenance and serviceability, with accessible components and modular designs that allow for quick repairs and upgrades, minimizing downtime and maximizing productivity.
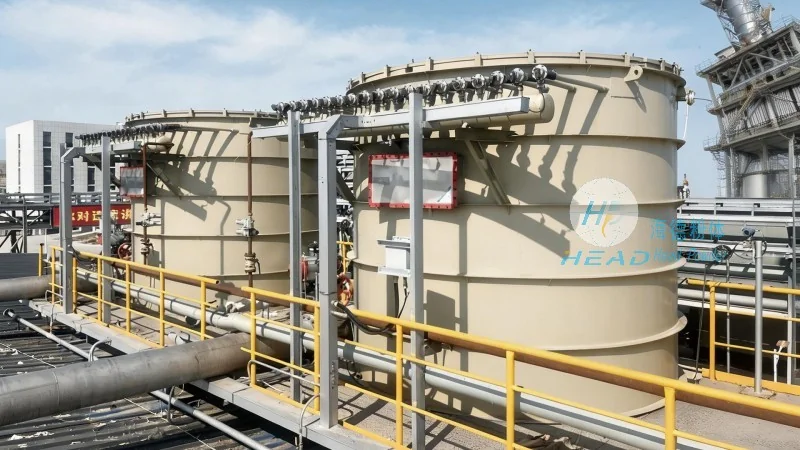
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of intelligent tonne bag loading stations and material conveying systems, serving clients globally with innovative industrial solutions. HeadPowder specializes in developing customized material handling systems that meet the unique requirements of various industries, focusing on enhancing operational efficiency, reducing labor costs, and improving workplace safety. The company's product line includes a range of tonne bag loading stations equipped with advanced material conveying technologies, tailored to handle different material types and production scales. HeadPowder's systems are engineered with high-quality components and rigorous testing to ensure reliability and performance in demanding industrial environments. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including installation, training, and maintenance services. HeadPowder is headquartered in Shandong, China, leveraging its local manufacturing capabilities and technical expertise to deliver cutting-edge material handling solutions that meet international standards and client expectations. Through continuous innovation and adherence to quality standards, HeadPowder has established itself as a trusted partner in the bulk material processing industry, providing reliable and efficient solutions for its clients.




