HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer based in Shandong, China. The company specializes in the design, development, and production of advanced conveying systems for various granular materials, including quartz sand. With a strong focus on engineering excellence and customer satisfaction, HeadPowder delivers reliable and efficient solutions tailored to industrial needs.
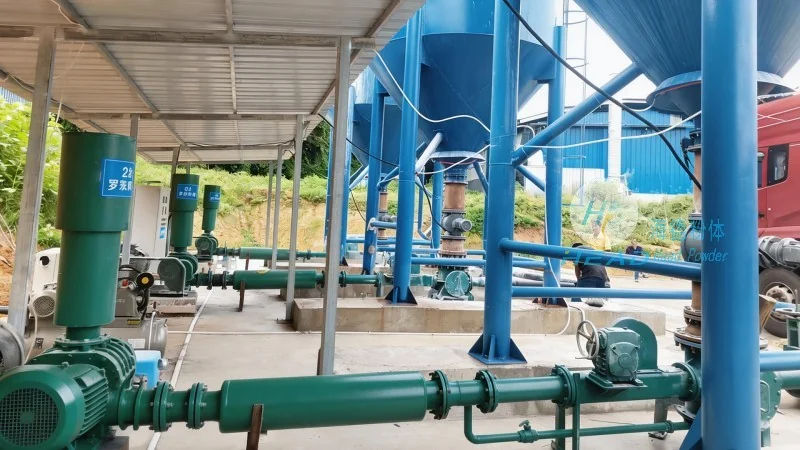
Overview of the Quartz Sand Granular Material Conveying System
The quartz sand granular material conveying system is a sophisticated piece of industrial equipment engineered to transport quartz sand efficiently and safely. This system integrates multiple components, including hoppers, conveyors, control panels, and safety mechanisms, to ensure seamless material handling. Its design prioritizes durability, low maintenance, and high throughput, making it suitable for applications in mining, construction, and manufacturing industries.
Operation Process of the Conveying System
The operation of the quartz sand conveying system begins with the loading of quartz sand into the hopper. The hopper is equipped with a feeding mechanism that regulates the flow of material into the conveyor. Once the material is in the hopper, the system's control panel activates the conveyor motor, initiating the material transport. The conveyor, typically a belt or screw type depending on the system design, moves the quartz sand from the hopper to the discharge point. During operation, the control panel continuously monitors parameters such as speed, pressure, and temperature to ensure optimal performance. If any abnormal conditions are detected, the system automatically shuts down or alerts the operator, preventing potential damage or material loss. The discharge process is controlled by a valve or gate at the end of the conveyor, allowing precise control over the output rate. The entire operation is designed to be user-friendly, with clear indicators and simple controls for easy operation.
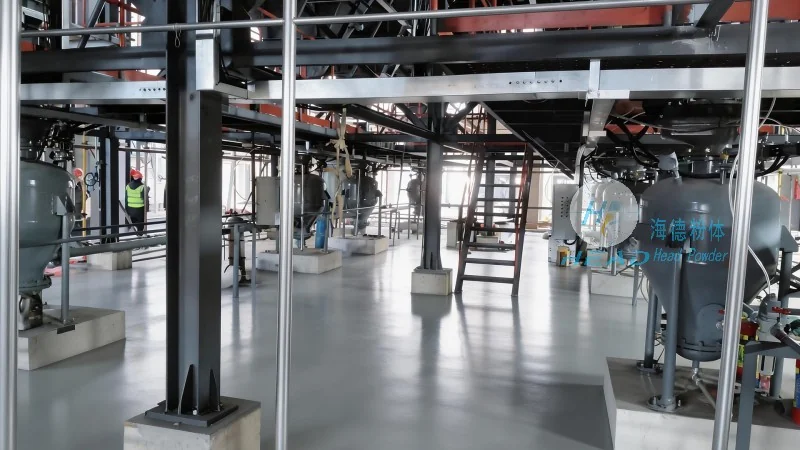
Working Principle of the Conveying System
The working principle of the quartz sand conveying system revolves around the mechanical transfer of material through a series of components. The system's core is the conveyor, which can be either a belt conveyor or a screw conveyor, depending on the specific application requirements. In a belt conveyor system, the quartz sand is placed on a moving belt, which transports it along the conveyor path. The belt is driven by a motor connected to a gearbox, which adjusts the speed and torque as needed. The hopper, positioned above the conveyor, provides a storage area for the quartz sand, ensuring a constant supply of material. The control panel manages the entire operation by sending signals to the motor and other components. Sensors are integrated into the system to monitor the material level in the hopper and the conveyor's operational status. These sensors provide real-time data to the control system, enabling automatic adjustments to maintain consistent performance. The safety mechanisms, such as emergency stop buttons and overload protection, are designed to protect both the equipment and the operators from potential hazards. The entire system operates on the principle of continuous motion, ensuring that the quartz sand is moved efficiently from the loading point to the discharge point without interruption.
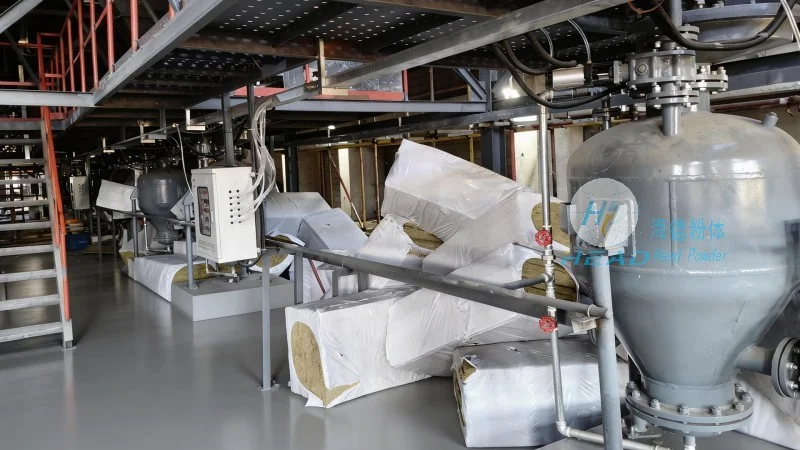
Key Components and Their Functions
The quartz sand conveying system consists of several key components, each playing a crucial role in the overall operation. The hopper serves as the material storage and feeding unit, with a design that minimizes material buildup and ensures smooth flow. The conveyor, whether belt or screw, is the primary transport mechanism, responsible for moving the quartz sand from the hopper to the discharge point. The control panel acts as the system's brain, coordinating all operations and monitoring critical parameters. Safety features, including emergency stop buttons and overload sensors, are integrated to prevent accidents and equipment damage. Regular maintenance of these components is essential to ensure the system's longevity and performance.
Benefits and Applications
The quartz sand granular material conveying system offers numerous benefits, including high efficiency, low energy consumption, and minimal material loss. Its design allows for precise control over the material flow, making it ideal for applications where consistency is critical. The system is widely used in industries such as mining, where quartz sand is a key raw material for glass production, and construction, where it is used in concrete and other building materials. The system's reliability and durability make it a preferred choice for businesses looking to streamline their material handling processes and improve overall productivity.




