Continuous bulk material feeding and conveying systems are essential in modern industrial processes, particularly for handling and transporting powders and granules efficiently. These systems are designed to provide a seamless, uninterrupted flow of bulk materials from a storage or processing point to the next stage of production. The core function of such systems is to ensure that material is delivered continuously, minimizing downtime and maximizing operational efficiency.
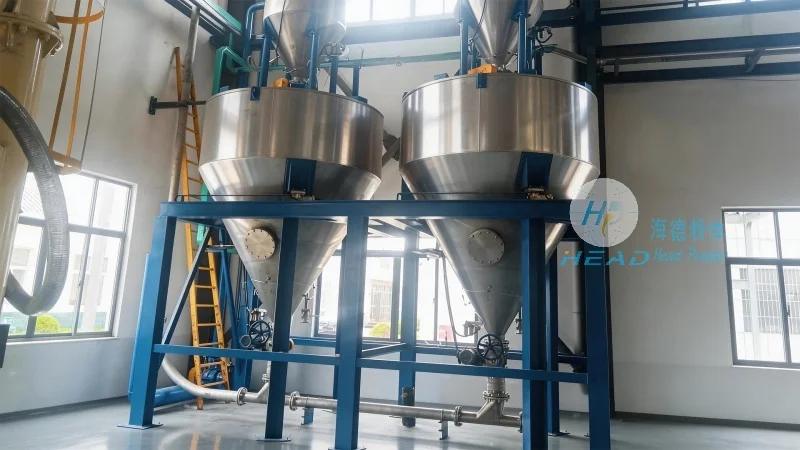
Key Components and Design Principles of Continuous Bulk Material Feeding Systems
The design of a continuous bulk material feeding system involves several critical components that work in harmony to achieve reliable and consistent material transfer. At the heart of the system is the feeding mechanism, which may include screw conveyors, vibratory feeders, or rotary valves, depending on the material characteristics and process requirements. These components are engineered to handle various types of powders, from fine powders to bulkier granules, ensuring minimal material degradation and consistent flow rates.
Control systems play a vital role in maintaining the stability of the feeding process. Modern continuous feeding systems often incorporate advanced control technologies, such as variable frequency drives (VFDs) and sensors, to adjust the feeding rate in real-time based on process conditions. This dynamic adjustment helps maintain a stable material level in silos or hoppers, preventing overfilling or underfilling, which can lead to process inefficiencies or equipment damage.
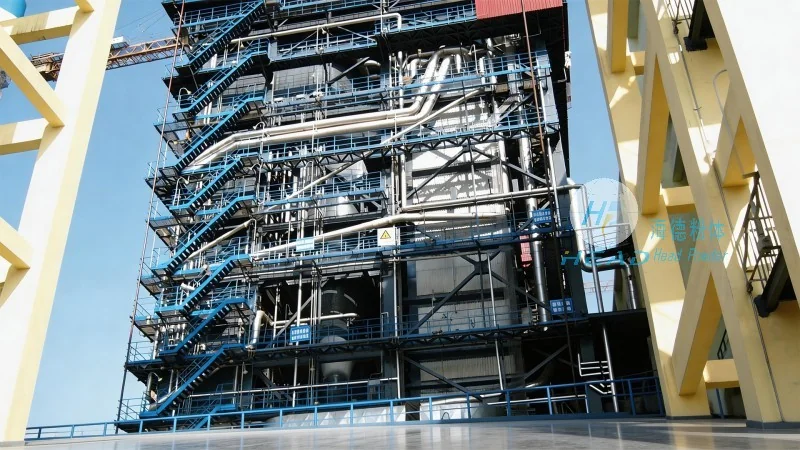
How Continuous Conveying Systems Ensure Efficient Material Transport
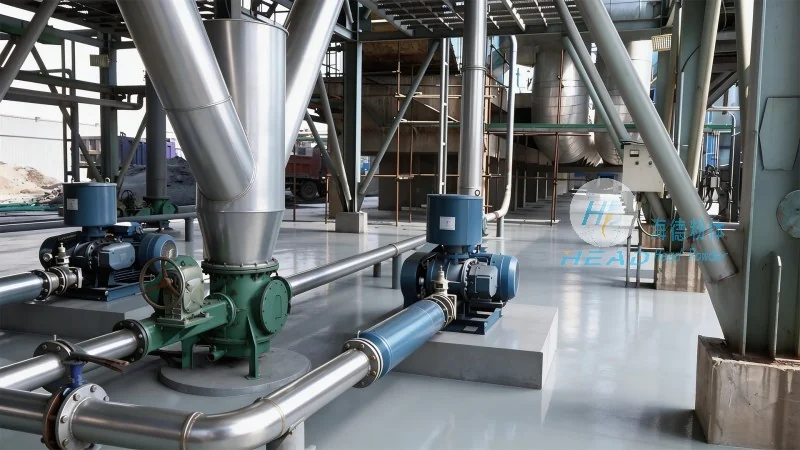
Once the material is fed into the system, it is transferred through a conveying section. Common types of conveying systems include pneumatic conveying (air-assisted) and mechanical conveying (e.g., belt conveyors, bucket elevators). The choice of conveying method depends on factors like material properties, distance to be covered, and environmental considerations. Pneumatic systems are ideal for fine powders and dusty materials, while mechanical systems are more suitable for bulkier or heavier materials.
The design of the conveying section focuses on minimizing material degradation and ensuring a smooth, continuous flow. For example, in pneumatic conveying, the use of low-pressure or high-pressure systems can be optimized based on the material's flowability and the required distance. Mechanical conveyors, such as belt or chain conveyors, are designed with appropriate incline angles and speed settings to prevent material buildup or slippage.
Applications and Benefits of Continuous Bulk Material Handling Systems
Continuous bulk material feeding and conveying systems are widely used across various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, for instance, these systems are crucial for handling active pharmaceutical ingredients (APIs) and ensuring precise dosing. The ability to maintain a consistent flow rate and minimize contamination is critical in such applications.
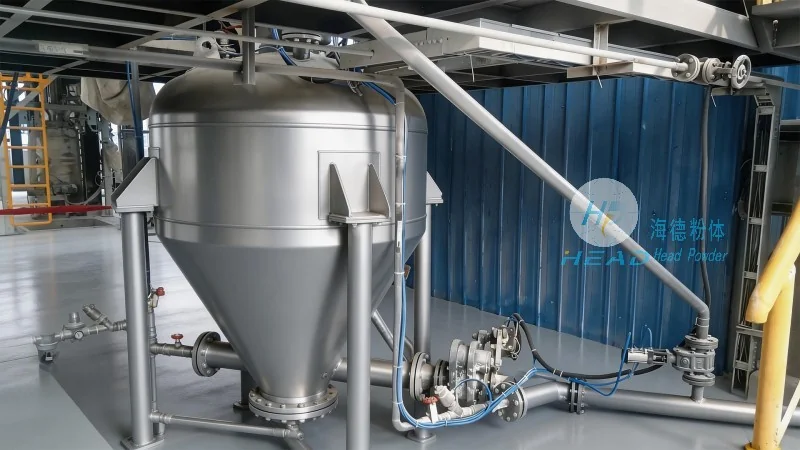
In the food processing sector, continuous feeding systems are used to handle ingredients like flour, sugar, and spices, ensuring a uniform blend and preventing cross-contamination. The design of these systems often incorporates sanitary features, such as stainless steel construction and easy-to-clean components, to meet regulatory standards.
For chemical manufacturers, continuous conveying systems help in transporting raw materials and finished products efficiently, reducing labor costs and improving safety by minimizing manual handling of hazardous materials. The ability to handle a wide range of materials, from dry powders to wet slurries, makes these systems versatile and valuable in chemical processing plants.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of continuous bulk material feeding and conveying systems. With its headquarters in Shandong, China, the company has established itself as a trusted partner in the industrial material handling sector. HeadPowder specializes in designing and manufacturing customized solutions tailored to the specific needs of its clients, ensuring optimal performance and reliability.
The company's expertise lies in understanding the unique challenges of different industries and developing innovative solutions that address these challenges. By leveraging advanced engineering techniques and rigorous quality control processes, HeadPowder delivers systems that meet or exceed industry standards. Its commitment to customer satisfaction and continuous improvement has made it a preferred choice for businesses seeking reliable and efficient bulk material handling solutions.
HeadPowder's products are designed to be durable, efficient, and easy to maintain, ensuring long-term operational performance. The company's team of experienced engineers and technicians provides comprehensive support, from system design and installation to after-sales service and maintenance. This comprehensive approach ensures that clients receive not just a product, but a complete solution that enhances their operational efficiency and productivity.




