Understanding the multi-functional powder handling system equipment is crucial for industries that rely on efficient and reliable material transport. This equipment plays a vital role in various sectors, including pharmaceuticals, food processing, and chemical manufacturing, by providing a versatile solution for moving bulk powders. The design principles behind such systems are centered on optimizing performance, ensuring safety, and enhancing operational efficiency.
Introduction to Multi-functional Powder Handling Systems
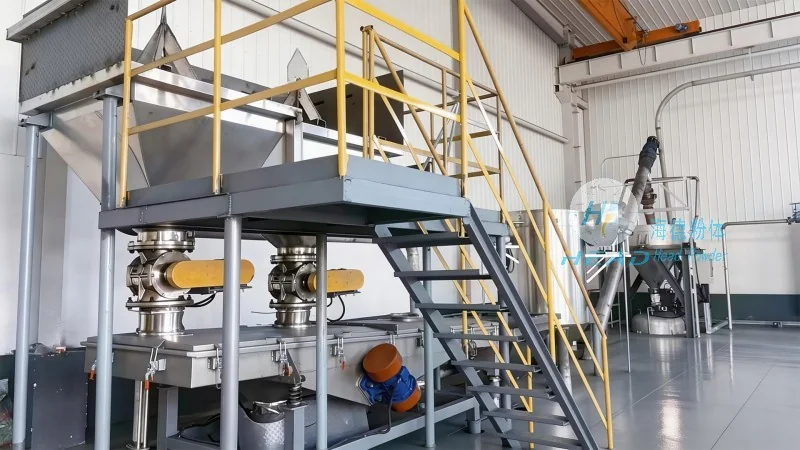
A multi-functional powder handling system is a sophisticated piece of machinery engineered to handle, transport, and manage bulk powders in diverse industrial applications. Unlike traditional systems that may be limited to specific powder types or operational conditions, these advanced systems offer flexibility and adaptability. The equipment typically integrates multiple components, such as feeders, conveyors, and control systems, to achieve seamless material flow. This versatility makes it an essential asset for businesses seeking to streamline their production processes and improve overall productivity.
HeadPowder: A Leading Provider of Powder Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a prominent manufacturer specializing in the design and production of high-quality powder handling equipment. With years of industry experience, HeadPowder has established itself as a trusted partner for companies worldwide. The company's commitment to innovation and customer satisfaction has enabled it to develop cutting-edge solutions that meet the evolving needs of modern industries. By leveraging advanced engineering techniques and rigorous quality control measures, HeadPowder ensures that its products deliver superior performance and durability.
Design Principles of Multi-functional Powder Handling Systems
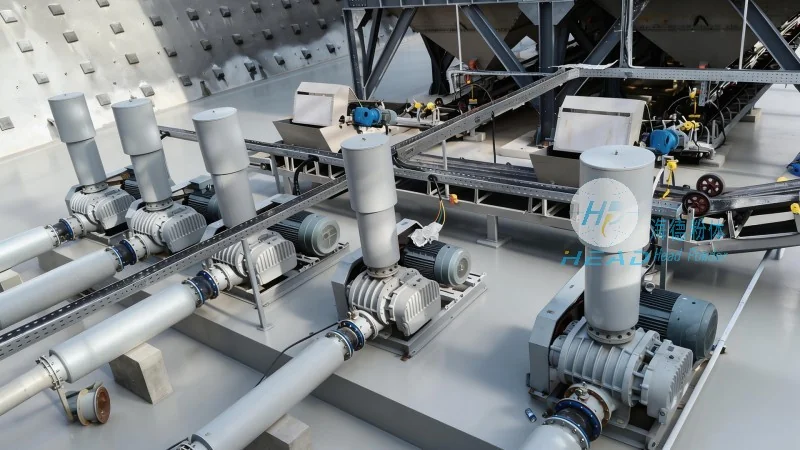
The design of a multi-functional powder handling system is guided by several key principles aimed at optimizing functionality and reliability. One of the primary considerations is the selection of appropriate materials for construction. Components such as hoppers, chutes, and conveyors are often made from corrosion-resistant materials like stainless steel to prevent contamination and ensure longevity. The system's design also focuses on minimizing material degradation and segregation during transport. This is achieved through the use of gentle handling mechanisms, such as pneumatic conveying or screw conveyors, which reduce the risk of particle breakage and ensure uniform flow.
Another critical design principle is the integration of advanced control systems. Modern powder handling systems are equipped with sophisticated sensors and automation technologies that monitor and regulate the flow of materials in real-time. These systems can detect variations in powder density, temperature, or flow rate, allowing for immediate adjustments to maintain optimal performance. The control systems also enhance safety by implementing emergency shut-off mechanisms and preventing overloading, which are essential for protecting both personnel and equipment.
Key Features and Functional Components
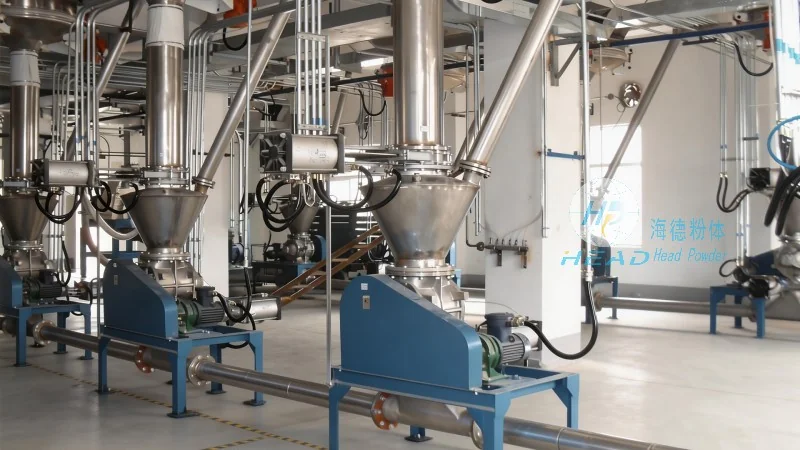
Multi-functional powder handling systems typically include several key components that work in concert to achieve efficient material transport. The primary components are the hopper, which serves as the storage container for bulk powders, and the feeder, which regulates the flow of material from the hopper to the conveyor system. The conveyor system, which may be pneumatic or mechanical, is responsible for transporting the powder to the desired destination. In addition to these core components, the system may incorporate additional features such as dust collection systems, which help maintain a clean and safe working environment, and level sensors, which monitor the powder level in the hopper and trigger refilling when necessary.
Advantages of Using Multi-functional Powder Handling Systems
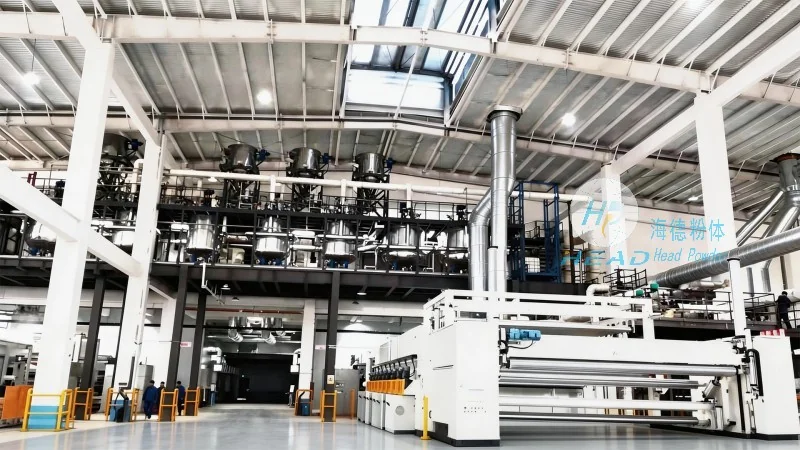
Implementing a multi-functional powder handling system offers numerous advantages for industrial operations. One of the most significant benefits is improved operational efficiency. By automating the material transport process, businesses can reduce labor costs and minimize downtime caused by manual handling. The versatility of these systems also allows for the handling of various powder types, from fine powders to bulk materials, without the need for extensive modifications. This flexibility enables companies to adapt to changing production demands and expand their product lines with ease. Furthermore, the advanced control systems and safety features of modern powder handling equipment contribute to a safer working environment, reducing the risk of accidents and improving overall workplace safety.
Conclusion
In conclusion, the multi-functional powder handling system equipment is a vital asset for industries that require efficient and reliable bulk powder transport. The design principles behind these systems prioritize performance, safety, and adaptability, ensuring that they can meet the diverse needs of modern manufacturing processes. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in providing high-quality solutions that enhance operational efficiency and support business growth. By investing in advanced powder handling systems, industries can achieve greater productivity, reduce costs, and maintain a competitive edge in their respective markets.




