Plunger flow powder conveyors are specialized pneumatic systems designed for efficient and reliable transport of bulk powders. These systems are widely used in industries such as chemical, food, and pharmaceutical manufacturing, where the handling of fine or cohesive powders requires precise control and minimal dust generation. The technology behind plunger flow systems offers significant advantages over traditional pneumatic conveying methods, making them a preferred choice for applications demanding high throughput and product integrity.
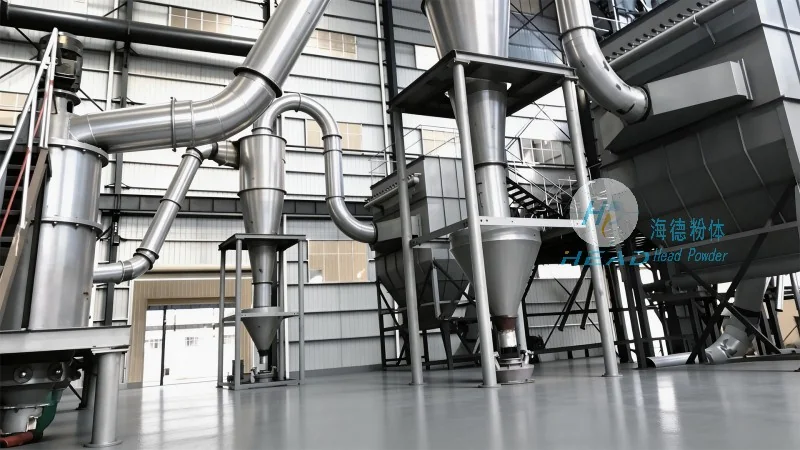
What is a Plunger Flow Powder Conveyor?
A plunger flow powder conveyor, also known as a plunger-type pneumatic conveyor, is a type of air-driven system that uses a reciprocating plunger to push bulk materials through a sealed pipeline. Unlike other pneumatic conveying methods that rely on air velocity to move particles, the plunger flow system employs a piston-like mechanism to create a "plug" or "slug" of material that travels through the pipe. This approach ensures that the powder moves in a controlled manner, reducing the risk of segregation and maintaining the integrity of the material being transported.
Key Design Principles of Plunger Flow Systems
The effectiveness of a plunger flow powder conveyor is determined by several critical design principles. First, the system must incorporate a robust air supply unit capable of delivering consistent pressure and volume to drive the plunger. This unit typically includes a compressor, air filter, and regulator to ensure stable operation. Second, the plunger itself is engineered to provide smooth, linear motion with minimal friction, which is essential for maintaining the integrity of the material and preventing wear on the system components. Third, the sealing mechanism between the plunger and the pipe is crucial; it must be leak-proof to prevent dust leakage and maintain the pressure within the system. Additionally, the control valves and sensors are integrated to regulate the plunger's movement and monitor the system's performance, ensuring optimal operation under varying load conditions.
How the Plunger Flow Mechanism Works
The operation of a plunger flow system involves a sequence of steps that ensure efficient material transport. Initially, the plunger is retracted from the pipe, creating a vacuum or low-pressure zone that draws the powder from the hopper into the pipe. Once the plunger is fully retracted, it is driven forward by the compressed air, pushing the accumulated powder forward as a compact plug. The plunger then returns to its original position, creating another vacuum to draw more material from the source. This cycle repeats continuously, maintaining a steady flow of material through the system. The key advantage of this mechanism is that it minimizes the interaction between the powder and the air, reducing the risk of dust dispersion and ensuring that the material remains in a solid state during transport.
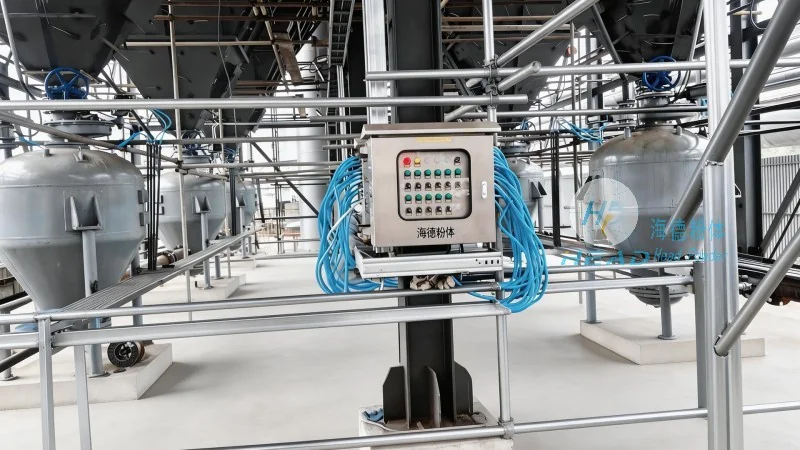
Applications and Benefits in Powder Handling
Plunger flow powder conveyors are particularly well-suited for applications involving cohesive or fine powders that are prone to dusting or segregation. In the chemical industry, they are used to transport raw materials such as cement, limestone, and chemicals to processing units. In the food industry, they handle ingredients like flour, sugar, and spices, maintaining product purity and preventing contamination. The pharmaceutical sector also benefits from these systems, as they can transport active pharmaceutical ingredients (APIs) and excipients with minimal risk of cross-contamination. The primary benefits of plunger flow systems include high conveying efficiency, low energy consumption, reduced dust generation, and the ability to handle a wide range of powder characteristics without the need for extensive modifications to the system.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of advanced powder handling equipment, headquartered in Shandong, China. With a strong focus on innovation and customer satisfaction, the company specializes in designing and manufacturing plunger flow powder conveyors tailored to the specific needs of various industries. HeadPowder's team of engineers and technicians leverages years of experience to develop reliable, efficient, and cost-effective solutions that meet international standards. The company's commitment to quality is evident in its rigorous testing protocols and adherence to industry best practices, ensuring that each product delivers optimal performance and longevity. HeadPowder serves clients globally, providing comprehensive support from initial consultation to after-sales service, helping businesses enhance their material handling processes and improve overall operational efficiency.




