HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced material handling systems tailored for lithium hydroxide applications. This article delves into the core principles and operational characteristics of such systems, highlighting their efficiency and adaptability in industrial settings.
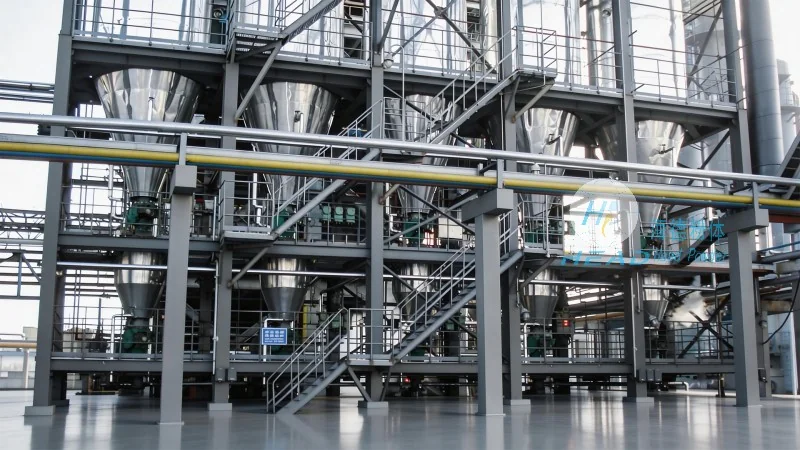
Principle of Lithium Hydroxide Material Handling Systems
The lithium hydroxide material handling system operates on a combination of mechanical and hydraulic principles to ensure safe and efficient transport of the material. At its core, the system utilizes a series of conveyor mechanisms, such as belt conveyors or screw conveyors, which are engineered to handle the specific physical properties of lithium hydroxide. These materials, known for their hygroscopic nature and potential reactivity under certain conditions, require specialized equipment to maintain integrity during transport. The system incorporates features like sealed containers, temperature-controlled environments, and anti-static measures to prevent material degradation or safety hazards. Additionally, the control system employs advanced sensors and automation technologies to monitor parameters like flow rate, temperature, and pressure in real-time, ensuring optimal performance and minimizing operational risks.
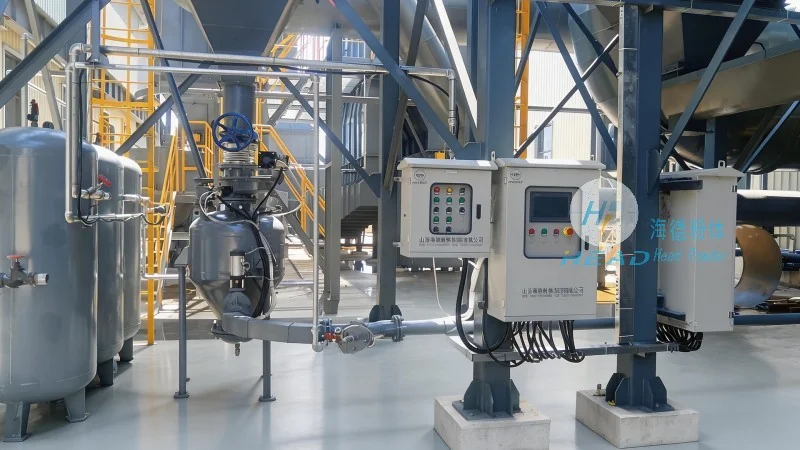
Working Scene Characteristics of the Equipment
The working scene characteristics of the lithium hydroxide material handling system are tailored to meet the demands of various industrial applications. In battery manufacturing facilities, for instance, the system is designed to integrate seamlessly with production lines, enabling continuous material flow from storage to processing stages. The equipment is typically installed in controlled environments, such as cleanrooms or specialized processing areas, where dust and moisture are strictly regulated. This ensures that the lithium hydroxide remains in a stable state, preventing premature reactions or contamination. The system's modular design allows for easy integration with existing infrastructure, reducing installation time and costs. Furthermore, the equipment is built to withstand the rigorous demands of high-volume production, with features like high-capacity conveyors and durable components that can handle continuous operation over extended periods. The operational flexibility of the system also allows it to adapt to different production scales, from small-scale laboratory applications to large-scale industrial manufacturing. This adaptability makes the system suitable for a wide range of industries, including battery production, chemical processing, and research facilities.
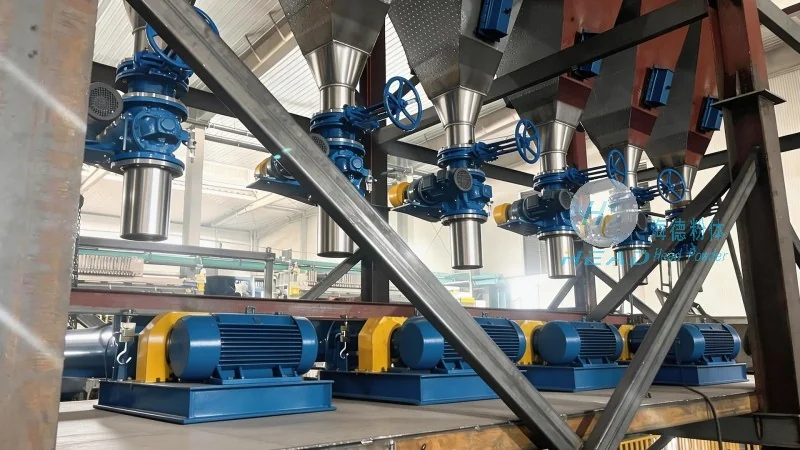
Key Features and Advantages in Practical Applications
Practical applications of the lithium hydroxide material handling system demonstrate significant advantages in terms of efficiency, safety, and cost-effectiveness. The system's ability to maintain material integrity during transport is crucial in industries where quality control is paramount. By preventing exposure to air or moisture, the equipment ensures that the lithium hydroxide remains in its optimal chemical state, which is essential for downstream processes like battery electrode production. The automated control system enhances operational efficiency by reducing the need for manual intervention, thereby minimizing human error and increasing production throughput. Safety features, such as emergency stop mechanisms and overfill protection, are integrated into the design to mitigate risks associated with handling potentially hazardous materials. The system's durability and low maintenance requirements also contribute to long-term cost savings, as it can operate reliably for extended periods with minimal downtime. Overall, the lithium hydroxide material handling system from HeadPowder provides a robust solution for industries requiring precise and safe material transport, aligning with the highest standards of industrial performance and safety.




