HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for coal ash materials. These systems represent a sophisticated approach to material handling, offering efficient, dust-free, and reliable solutions for industrial applications. The core principle of pneumatic conveying involves the use of air or gas to transport bulk materials through a pipeline network, eliminating the need for traditional mechanical conveying methods such as belts or buckets.
The Fundamental Principle of Pneumatic Conveying
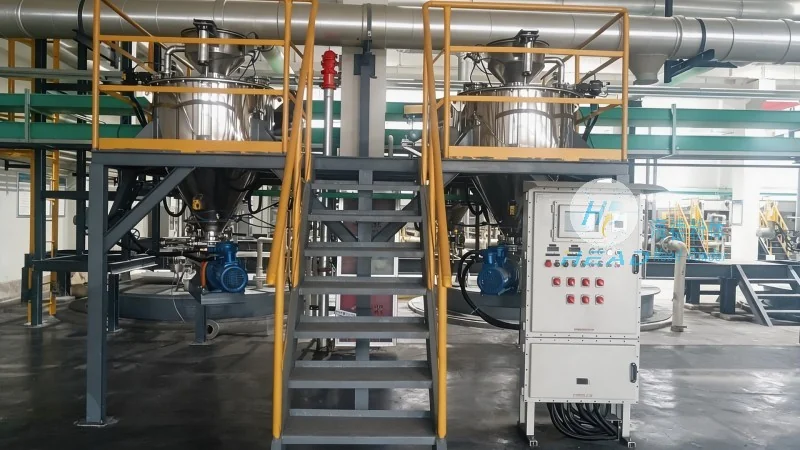
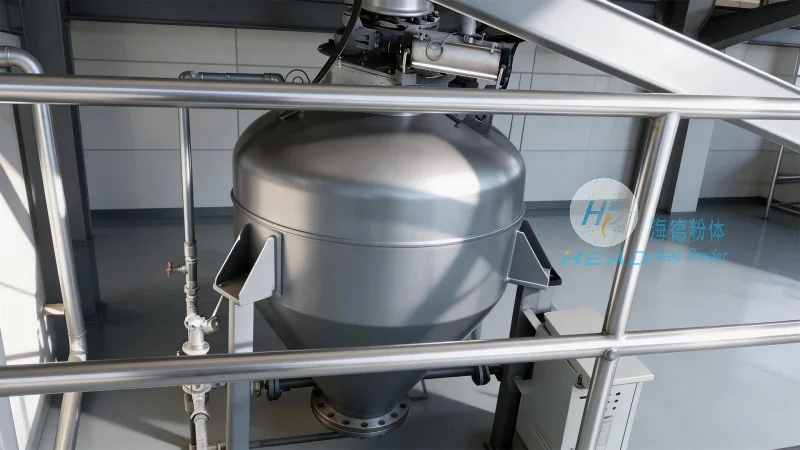
The operation of a coal ash pneumatic conveying system is grounded in the physics of fluid dynamics and material transport. At its essence, the system uses a pressure or vacuum source to create a flow of air within a pipeline. This airflow generates sufficient velocity to entrain the coal ash particles, lifting them from the source and transporting them to the destination. The system typically consists of several key components, including a material feed hopper, a conveyor line, a separation or filtration unit, and a discharge point. The feed hopper ensures a consistent supply of coal ash, while the conveyor line, often equipped with special fittings like bends and expansions, facilitates the smooth movement of the material. The separation unit is crucial for removing excess air and fine particles, ensuring the material is delivered in a clean and controlled manner. This principle allows for the efficient transfer of coal ash from its point of origin to processing or storage facilities, minimizing downtime and operational costs.
Key Working Scene Characteristics of Coal Ash Pneumatic Conveying Systems
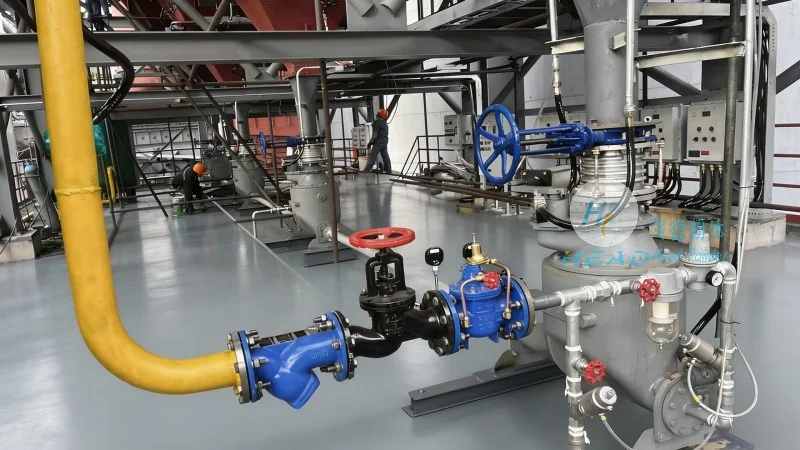
The application of coal ash pneumatic conveying systems is characterized by several distinct working scene features that make them ideal for specific industrial environments. First, these systems are designed to handle the unique properties of coal ash, which can vary in particle size, moisture content, and density. The flexible design of pneumatic conveying allows for adjustments to accommodate different material characteristics, ensuring optimal performance. Second, the systems are highly effective in environments where dust control is critical. Unlike mechanical conveying methods, which can generate significant airborne dust, pneumatic conveying operates within a sealed system, reducing the risk of contamination and improving workplace safety. Third, the systems offer scalability and adaptability, making them suitable for both small-scale and large-scale industrial operations. Whether used in power plants for transporting ash from boilers to storage silos or in construction material processing facilities for handling ash as a raw material, the systems can be customized to meet the specific needs of the application. Additionally, the systems provide energy efficiency benefits, as they often require less power compared to traditional mechanical conveying systems, leading to lower operational costs over time.
Company Overview: HeadPowder Engineering
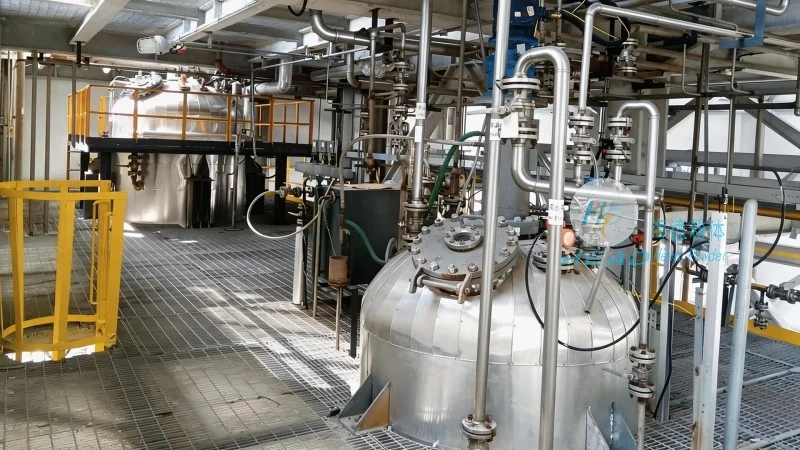
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable company dedicated to providing innovative engineering solutions for material handling and processing. With a strong focus on pneumatic conveying systems, the company leverages advanced technology and expertise to deliver high-quality, reliable systems for coal ash and other bulk materials. The company's commitment to customer satisfaction and operational excellence is reflected in its comprehensive approach to system design, installation, and maintenance. By combining state-of-the-art equipment with professional engineering services, HeadPowder ensures that its clients receive tailored solutions that meet their specific operational requirements. The company's presence in Shandong, China, positions it to serve a wide range of industrial sectors, including power generation, construction, and waste management, with a deep understanding of regional industry needs and standards.




