HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. This article focuses on the operation process and working principle of sintered ash pneumatic conveying equipment, a critical component in industrial material handling for efficient ash transport from sintering processes.
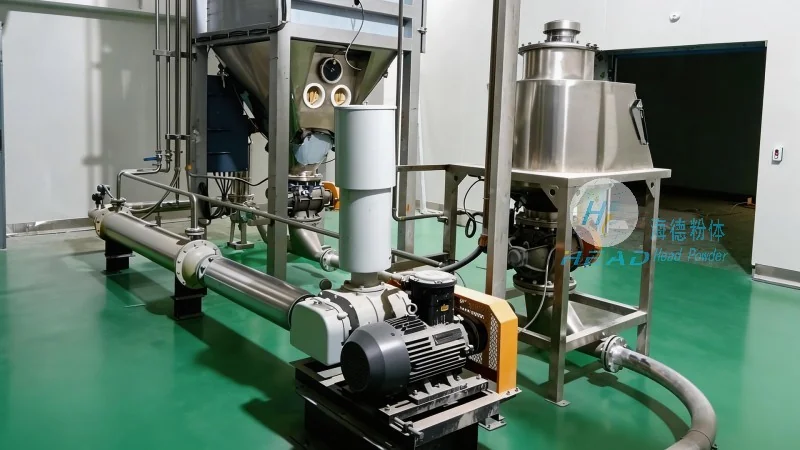
Overview of Sintered Ash Pneumatic Conveying Equipment
Sintered ash, a byproduct of sintering operations in metallurgical and chemical industries, requires specialized handling due to its characteristics such as high temperature, abrasive nature, and potential for dust generation. The sintered ash pneumatic conveying equipment developed by Shandong HeadPowder Engineering Co., Ltd. addresses these challenges through a robust and efficient system that ensures safe and reliable transport of the material from the sintering plant to storage or processing facilities.
Key Components of the Pneumatic Conveying System
The sintered ash pneumatic conveying system typically consists of several key components that work in tandem to achieve effective material transport. These components include the ash hopper, which serves as the material storage and feeding unit; the rotary valve, responsible for controlling the flow of ash from the hopper to the conveying line; the air compressor or blower, which generates the necessary air pressure to move the material; the conveying pipeline, which transports the ash and air mixture; and the dust collector or filter system, which captures any airborne particles to ensure environmental compliance and operational safety.
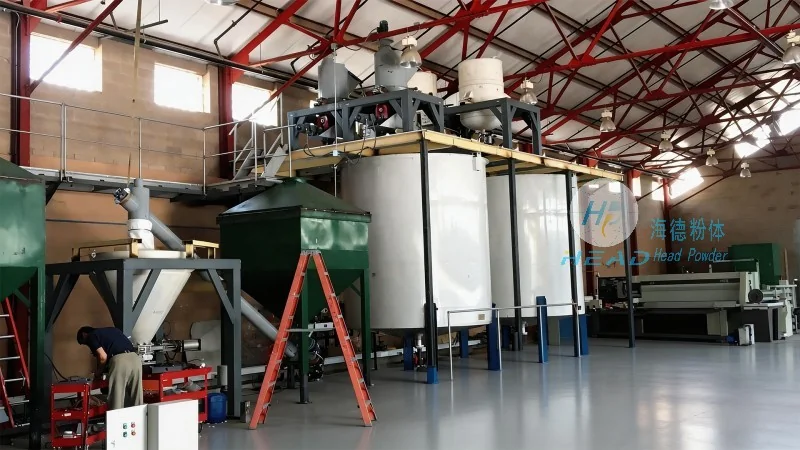
Operation Process of the Sintered Ash Pneumatic Conveying Equipment
The operation process of the sintered ash pneumatic conveying equipment begins with the loading of sintered ash into the ash hopper. The rotary valve then regulates the discharge of ash into the conveying pipeline, ensuring a consistent flow rate. Simultaneously, the air compressor or blower starts operating, generating a high-pressure air stream that travels through the pipeline. As the ash is introduced into the pipeline, it is entrained by the air stream and carried to the destination point, such as a storage silo or processing unit. The system is designed to maintain optimal air-to-material ratios to prevent blockages and ensure smooth transport. At the receiving end, the ash is separated from the air stream using a separator or cyclone, and the air is then filtered and discharged through the dust collector, minimizing environmental impact.
Working Principle of the Pneumatic Conveying System
The working principle of the sintered ash pneumatic conveying equipment is based on the principle of pneumatic transport, where solid particles are suspended and transported by a moving gas stream. The system operates under positive pressure, meaning the air pressure inside the pipeline is higher than the ambient pressure. This positive pressure ensures that the ash particles are continuously carried along the pipeline without settling or clogging. The air compressor or blower provides the necessary pressure and flow rate to maintain the transport conditions. The rotary valve controls the feeding rate of the ash, while the air flow rate is adjusted to match the material flow, ensuring efficient and stable operation. The separator at the end of the pipeline uses centrifugal force to separate the ash from the air, allowing the ash to be collected and the air to be filtered and released.
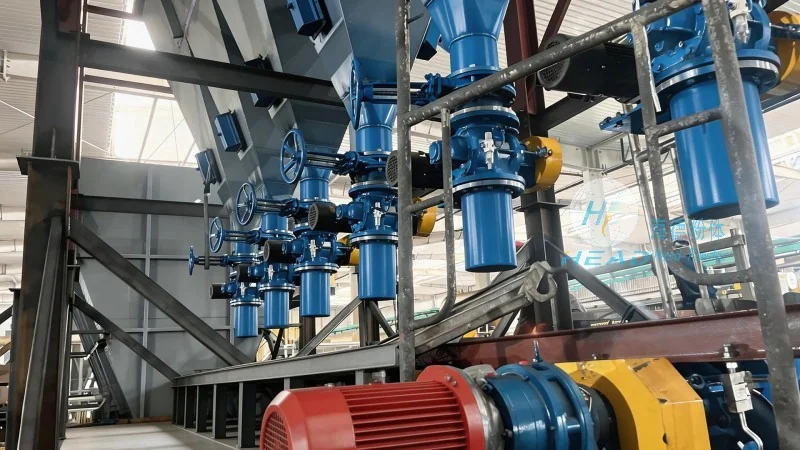
Advantages and Applications
The sintered ash pneumatic conveying equipment offers several advantages over traditional conveying methods, such as belt conveyors or bucket elevators. These advantages include reduced labor costs, minimized material handling time, and improved safety due to enclosed systems that prevent dust exposure. The equipment is particularly suitable for applications where the ash is hot or abrasive, as the pneumatic system can handle these conditions without damage to the components. Industries that benefit from this technology include steel mills, power plants, and chemical manufacturing facilities, where sintered ash is a byproduct that needs to be transported efficiently and safely.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides high-quality sintered ash pneumatic conveying equipment that combines advanced engineering with robust construction to meet the demanding requirements of industrial material handling. The operation process and working principle of this equipment ensure efficient, reliable, and safe transport of sintered ash, contributing to improved operational efficiency and environmental compliance in various industrial applications. With its headquarters in Shandong, China, HeadPowder continues to innovate and deliver solutions that enhance the performance of pneumatic conveying systems for its clients worldwide.




