Understanding the operation process and working principle of cement pneumatic conveying lines is crucial for optimizing material handling efficiency in industrial settings. These systems are designed to transport bulk materials like cement, powders, and granules through a pipeline using air or gas as the conveying medium. The technology offers a flexible and efficient solution for moving materials over short to medium distances, often with minimal maintenance requirements. This article delves into the key aspects of how cement pneumatic conveying lines function, from their fundamental working principles to the step-by-step operation process, providing insights into their practical application and benefits.
Introduction to Cement Pneumatic Conveying Lines
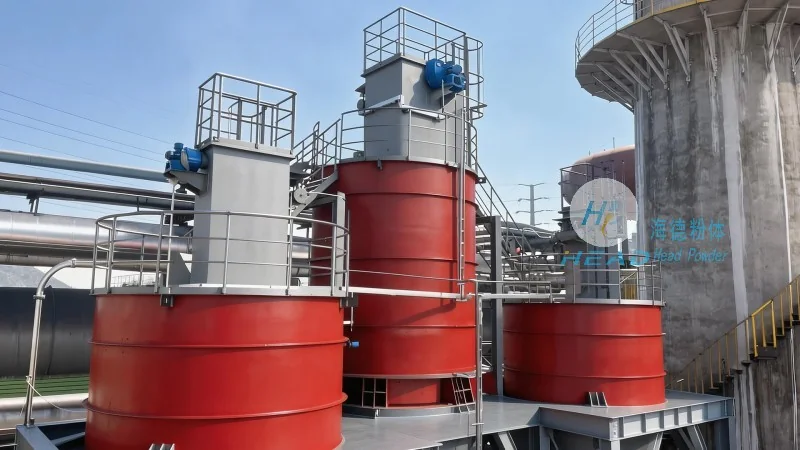
Cement pneumatic conveying lines are industrial systems used to transport bulk materials, particularly cement, through a pipeline network using air or gas as the driving force. Unlike traditional mechanical conveyors, these systems rely on the movement of air to create a flow of material, making them suitable for applications where space is limited or where the material needs to be transferred over varying distances. The design of these lines typically includes components such as a hopper, a blower or compressor, a pipeline system, and a discharge point, all working in tandem to ensure efficient material transport. The technology is widely adopted in cement plants, construction sites, and other industrial facilities due to its ability to handle high volumes of material while maintaining low operational costs.
Working Principle of Cement Pneumatic Conveying Lines
The core working principle of cement pneumatic conveying lines revolves around the creation of a gas-solid flow within the pipeline. There are two primary types of systems: positive pressure and negative pressure (or vacuum) systems. In a positive pressure system, a blower or compressor generates high-pressure air that is introduced into the pipeline, pushing the material forward. The air and material mix together, forming a dense phase or dilute phase flow depending on the system design and operating conditions. In a negative pressure system, a vacuum is created at the discharge end, drawing the material and air into the pipeline from the hopper. The choice between positive and negative pressure depends on factors such as the distance to be covered, the material properties, and the desired flow rate.
During operation, the material is first fed into the hopper from the source. The hopper is equipped with a feeder, which may be a rotary valve or a screw feeder, to control the flow rate of the material. Simultaneously, the blower or compressor starts operating, providing the necessary air pressure or vacuum. The air is then introduced into the pipeline, either at the inlet (for positive pressure) or at the discharge end (for negative pressure), initiating the conveying process. The material particles are entrained by the air stream and transported through the pipeline to the discharge point. At the discharge end, the air and material are separated, often using a cyclone separator or a filter, and the material is collected in a storage bin or directly to the end user.
Step-by-Step Operation Process of Cement Pneumatic Conveying Lines
The operation of a cement pneumatic conveying line involves several key steps that ensure smooth and efficient material transport. The process begins with the preparation of the system, which includes checking the integrity of the pipeline, ensuring the blower or compressor is functioning correctly, and verifying that the hopper is filled with the appropriate amount of material. Once the system is ready, the following steps are typically executed:
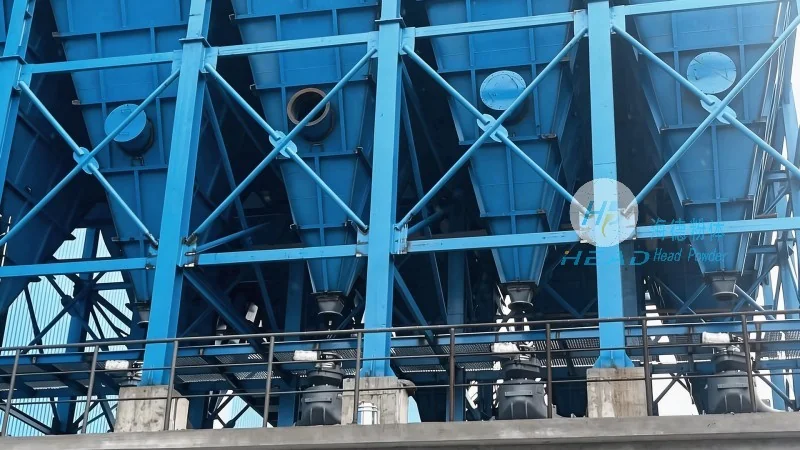
1. **Material Loading**: The cement is loaded into the hopper from the storage silo or bulk container. The hopper is designed to hold a sufficient quantity of material to sustain the conveying operation for an extended period, minimizing the need for frequent refills.
2. **Air Supply Activation**: The blower or compressor is activated, and the air flow is adjusted to the required pressure or vacuum level. The air flow rate is controlled to match the material feed rate, ensuring that the material is fully entrained and transported without clogging or excessive air consumption.
3. **Conveying Initiation**: The feeder mechanism in the hopper starts to discharge the material into the pipeline. The air stream, introduced at the inlet (for positive pressure) or the discharge end (for negative pressure), picks up the material particles and propels them forward. The material travels through the pipeline at a controlled velocity, maintaining a stable flow.
4. **Material Transport and Separation**: The material continues to be transported through the pipeline until it reaches the discharge point. At the discharge end, a separator is used to separate the material from the air. This separation is critical to prevent dust emissions and to ensure that the material is delivered in a dry and clean state. The separated material is then collected in a receiving bin or transferred to the next stage of the process.
5. **System Shutdown and Maintenance**: After the conveying operation is complete, the system is shut down by first stopping the air supply and then the material feeder. The pipeline is then purged to remove any remaining material, preventing blockages and ensuring the system is ready for the next cycle. Regular maintenance, such as checking for leaks, cleaning the separator, and inspecting the feeder, is essential to maintain the efficiency and longevity of the system.
Key Components and Their Roles in Cement Pneumatic Conveying Lines
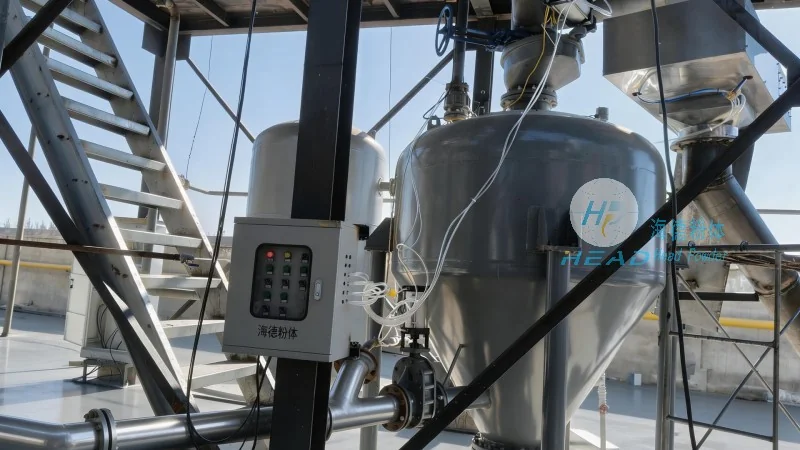
The effectiveness of a cement pneumatic conveying line depends on the proper functioning of several key components. Each component plays a critical role in the overall operation and efficiency of the system. The main components include:
1. **Hopper**: The hopper serves as the material storage and feeding unit. It is typically made of stainless steel or other corrosion-resistant materials to handle the abrasive nature of cement. The hopper is equipped with a feeder, such as a rotary valve or a screw feeder, which controls the flow rate of the material into the pipeline. The design of the hopper, including its shape and the position of the feeder, affects the flow characteristics and the uniformity of the material discharge.
2. **Blower or Compressor**: This component provides the necessary air pressure or vacuum to drive the material through the pipeline. The choice of equipment depends on the system type (positive or negative pressure) and the required flow rate. High-pressure blowers are used in positive pressure systems, while vacuum pumps are used in negative pressure systems. The blower or compressor must be capable of delivering the required air volume and pressure to maintain a stable material flow.
3. **Pipeline System**: The pipeline is the main conduit for transporting the material and air. It is typically made of stainless steel or PVC, depending on the material being conveyed and the operating conditions. The pipeline is designed with appropriate bends and elbows to accommodate the layout of the facility, and it is equipped with pressure relief valves to prevent over-pressurization. The diameter and length of the pipeline are critical factors that affect the conveying efficiency and the required air pressure.
4. **Discharge and Separation System**: The discharge end of the pipeline is equipped with a separator, such as a cyclone or a bag filter, to separate the material from the air. The separator is designed to capture the material particles while allowing the air to escape. The collected material is then transferred to a storage bin or directly to the end user. The efficiency of the separator is crucial to minimize dust emissions and to ensure that the material is delivered in a clean state.
Advantages and Applications of Cement Pneumatic Conveying Lines
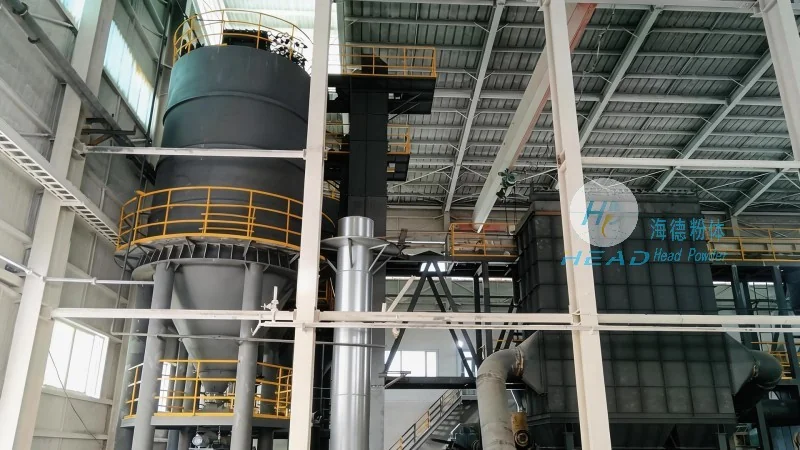
Cement pneumatic conveying lines offer several advantages over traditional mechanical conveyors, making them a preferred choice in many industrial applications. The key advantages include:
1. **Flexibility in Layout**: The pipeline system can be easily configured to follow the layout of the facility, allowing for material transport over varying distances and in different directions. This flexibility is particularly useful in plants with complex layouts or where space is limited.
2. **Low Maintenance Requirements**: Compared to mechanical conveyors, pneumatic conveying systems have fewer moving parts, reducing the need for regular maintenance and minimizing downtime. The components are also less prone to wear and tear, resulting in lower maintenance costs over the system's lifespan.
3. **Efficient Material Handling**: The systems can handle high volumes of material at a consistent flow rate, ensuring that production processes are not interrupted. The ability to transport material over longer distances without the need for intermediate transfer points also improves overall efficiency.




