Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in pneumatic conveying systems, particularly for bone powder applications. The company is located in Shandong, China, and has extensive experience in designing and manufacturing equipment tailored to the unique requirements of bone powder handling.
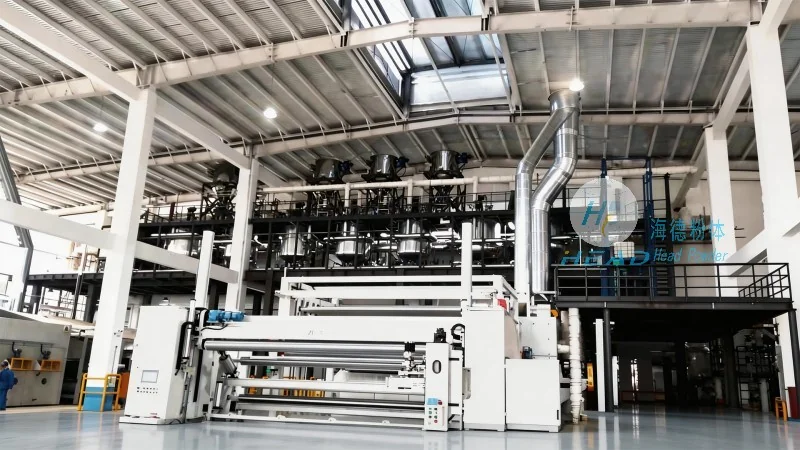
Overview of the Bone Powder Pneumatic Conveying System
The bone powder pneumatic conveying system is a closed-loop system designed to transport bone powder from the storage silo to the processing or packaging area. It operates by using compressed air or vacuum to move the powder through a network of pipes and components. This method offers a hygienic, dust-free, and efficient way to handle bone powder, which is critical for maintaining product quality and safety in food and animal feed industries.
Key Components and Their Functions
The system consists of several key components, each playing a vital role in the conveying process. The main components include the hopper or storage silo, which holds the bone powder; the feeder, which controls the flow rate of the powder into the conveying line; the pipeline, which transports the powder; and the receiver, which collects the material at the destination. Additionally, the system may include a filter system to remove dust and a pressure regulator to maintain consistent air pressure.
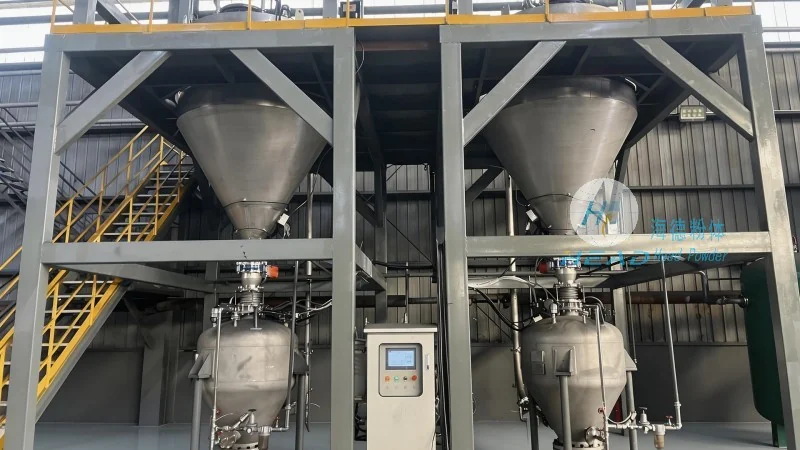
Operation Process: Step-by-Step
The operation process of the bone powder pneumatic conveying system begins with the loading of bone powder into the hopper. The feeder then regulates the amount of powder released into the conveying line. Compressed air is introduced into the pipeline, creating a flow that lifts and transports the powder particles. The air flow is controlled to ensure a consistent and stable conveying rate, preventing blockages or uneven flow. The powder is then delivered to the receiver, where it is collected and prepared for further processing or packaging.
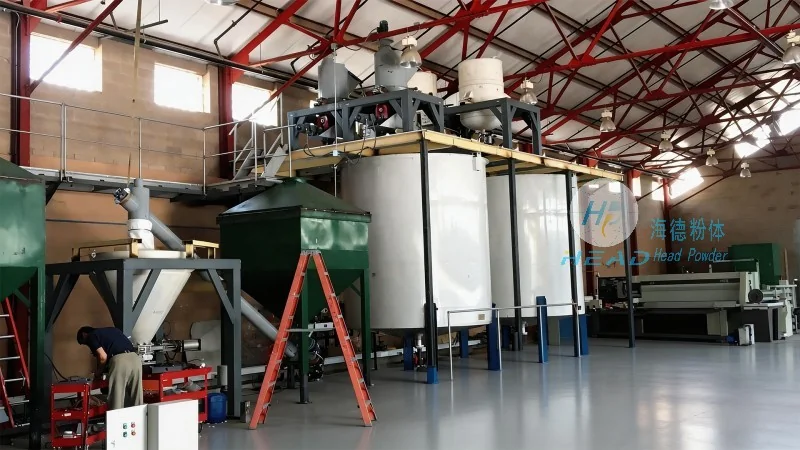
Working Principle: How It Works
The working principle of the pneumatic conveying system relies on the principles of fluid dynamics and particle transport. When compressed air is introduced into the pipeline, it creates a low-pressure zone that draws the bone powder particles into the air stream. The air and powder form a suspension, which moves through the pipeline at a controlled velocity. The system can operate under either positive pressure (where air is forced into the system) or negative pressure (where air is drawn out), depending on the specific application and layout. The design of the system ensures that the powder is transported without degradation, maintaining its quality and characteristics.
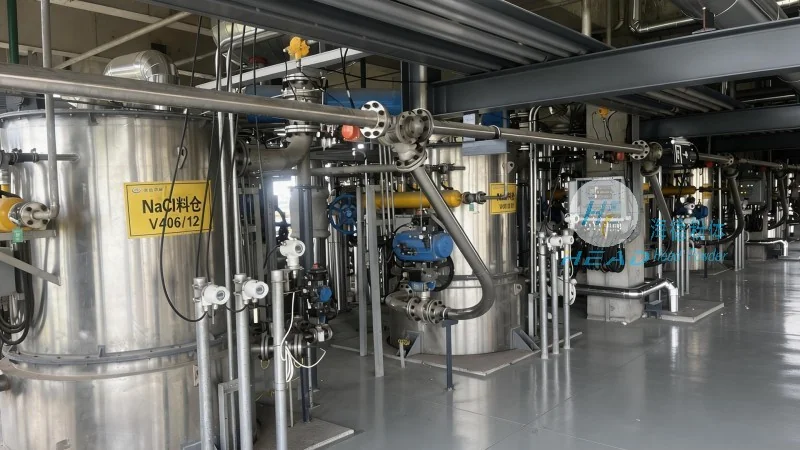
Advantages of the Bone Powder Pneumatic Conveying System
This system offers several advantages for bone powder handling. It provides a dust-free and hygienic method of transport, which is crucial for food and pharmaceutical applications. The enclosed system prevents contamination and reduces the risk of cross-contamination. Additionally, the pneumatic conveying system can handle varying particle sizes and moisture content, making it versatile for different bone powder types. The system's design allows for easy integration into existing production lines, minimizing downtime and maintenance costs. Furthermore, the system can be customized to meet specific production requirements, ensuring optimal performance and efficiency.
Maintenance and After-Sales Service
Regular maintenance is essential to ensure the optimal performance of the pneumatic conveying system. This includes checking the air compressor, cleaning the filters, and inspecting the pipeline for blockages. The company provides comprehensive after-sales service, including technical support and spare parts supply, to ensure the system operates efficiently throughout its lifespan. Proper maintenance helps to extend the life of the equipment and reduce the risk of breakdowns, ensuring consistent production output.




