HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for efficient dust handling. These systems are critical in various industrial sectors, offering a reliable method to transport powders and fine particulates over long distances with minimal environmental impact.
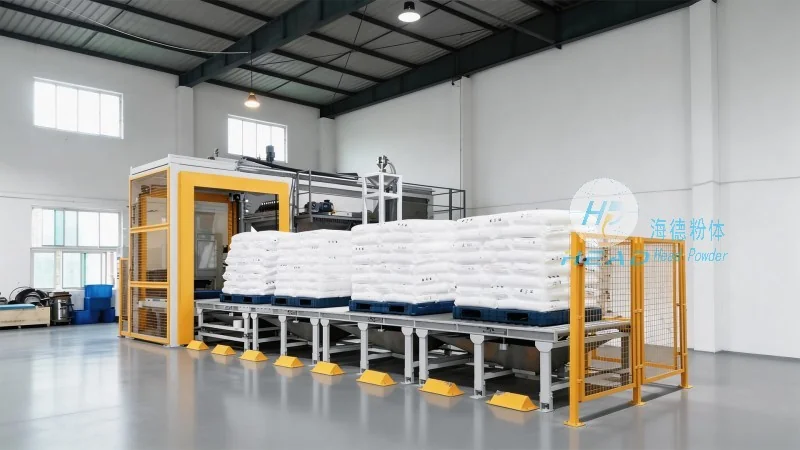
Pneumatic Conveying System Types: A Comprehensive Overview
At HeadPowder, we recognize that the choice of pneumatic conveying system depends on the specific characteristics of the material being handled, the distance of transport, and the operational environment. Our expertise lies in three primary system types, each with distinct advantages and applications:
- Positive Pressure Systems: These systems utilize a positive pressure air stream to push material through a pipeline. They are ideal for applications requiring high material velocity, such as transporting abrasive or sticky powders. The positive pressure also helps in maintaining a clean and controlled environment, preventing dust leakage.
- Negative Pressure (Vacuum) Systems: In contrast, negative pressure systems use a vacuum to draw material into the system. This approach is suitable for handling materials that are sensitive to air exposure or for applications where the material source is located at a higher elevation. The vacuum system is particularly effective for collecting dust from multiple points and transporting it to a central collection point.
- Mixed-Pressure Systems: Combining elements of both positive and negative pressure, mixed-pressure systems offer flexibility. They can start with a vacuum to draw material from a source and then switch to positive pressure to push it through the pipeline, optimizing energy use and system efficiency. This hybrid approach is often used in complex conveying networks where varying material properties and distances are involved.
Practical Applications in Industrial Settings
HeadPowder's pneumatic conveying solutions are widely adopted across industries, demonstrating their versatility and reliability. For instance, in the pharmaceutical industry, where product purity is paramount, our systems ensure that powders are transported without contamination or degradation. The negative pressure systems are particularly favored here to maintain a sterile environment.
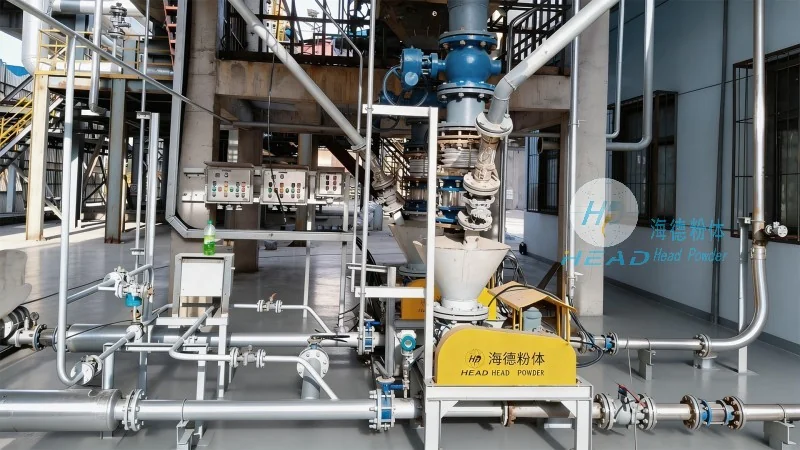
In the food processing sector, our equipment is designed to handle sensitive ingredients like flour, sugar, and spices, adhering to strict hygiene standards. The positive pressure systems are often preferred for these applications to prevent cross-contamination and maintain product quality.
In the chemical and petrochemical industries, our systems are engineered to handle corrosive or hazardous materials. The robust construction and material selection ensure safety and compliance with regulatory standards. The ability to transport these materials in a closed system minimizes the risk of exposure to personnel and the environment.
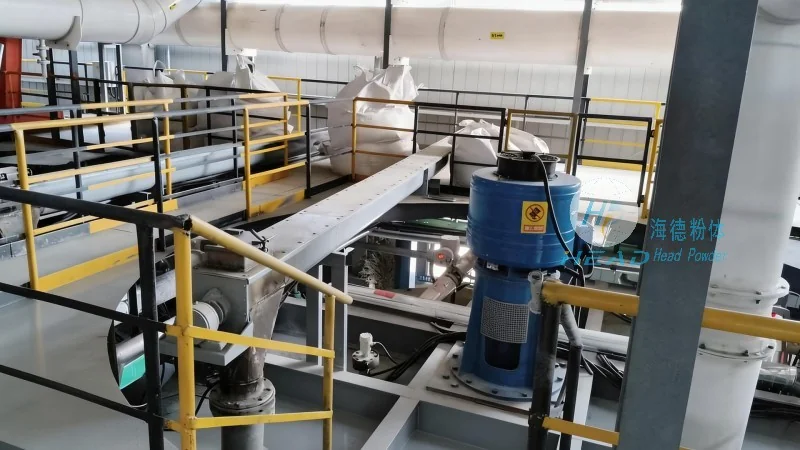
In the cement and construction materials industry, large volumes of bulk materials like cement, fly ash, and sand are efficiently conveyed using our systems. The positive pressure systems are commonly used here due to their high capacity and ability to handle large quantities of material over long distances.
Key Advantages and Technical Considerations
Implementing a pneumatic conveying system from HeadPowder offers several advantages, including reduced labor costs, minimized material loss, and improved workplace safety. Unlike traditional belt or bucket elevators, these systems operate in a closed loop, preventing dust emissions and ensuring compliance with environmental regulations.
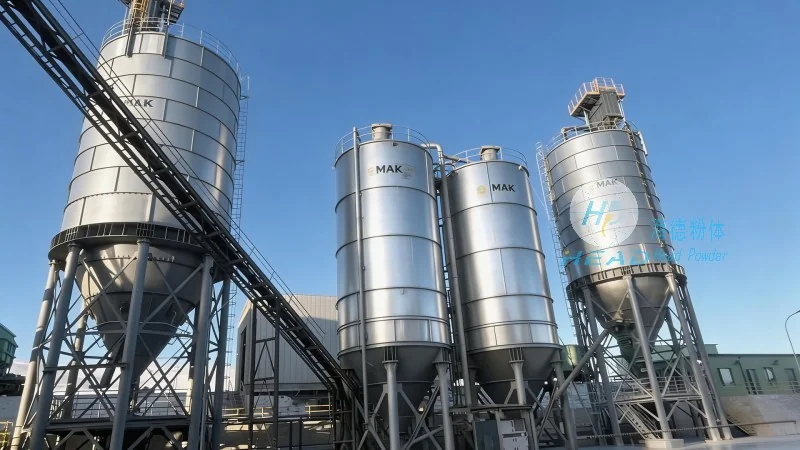
Technical considerations include the selection of appropriate air velocities, pipeline diameter, and system pressure. Our engineering team at HeadPowder conducts thorough analyses of material properties, such as particle size, density, and flowability, to design a system that meets the specific requirements of each client. This tailored approach ensures optimal performance and longevity of the equipment.
Furthermore, our systems are equipped with advanced control mechanisms that allow for real-time monitoring and adjustment, enhancing operational efficiency. The integration of sensors and automation technology enables precise control over the conveying process, reducing downtime and maintenance costs.




