What is a Cereal Material Handling System? What are its Design Principles?
Release time:2026-09-15 21:01:17
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For manufacturers in the cereal industry, efficient material handling is crucial to maintaining production efficiency and product quality. A cereal material handling system is a specialized setup designed to transport, store, and manage cereal products from raw materials to finished goods. This system integrates various components such as conveyors, elevators, and storage silos to ensure smooth workflow and minimize downtime. Understanding the core components and design principles of such a system is essential for optimizing operations and meeting industry standards.
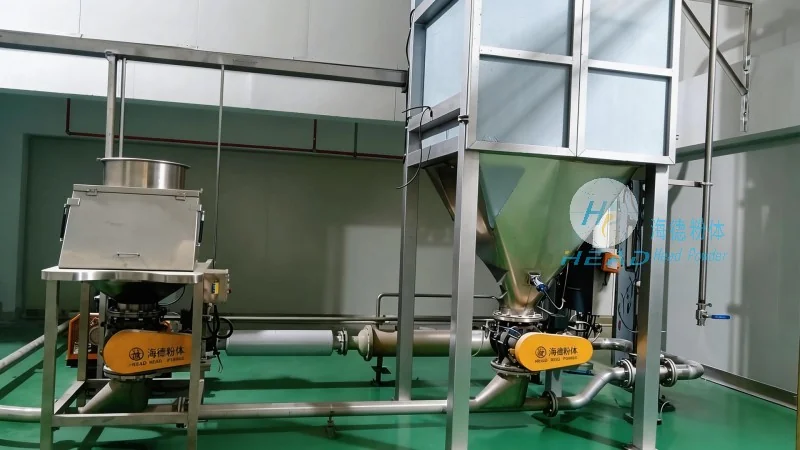
Key Components of a Cereal Material Handling System
The effectiveness of a cereal material handling system largely depends on its integrated components. These components work in tandem to ensure seamless material flow. The primary components include:
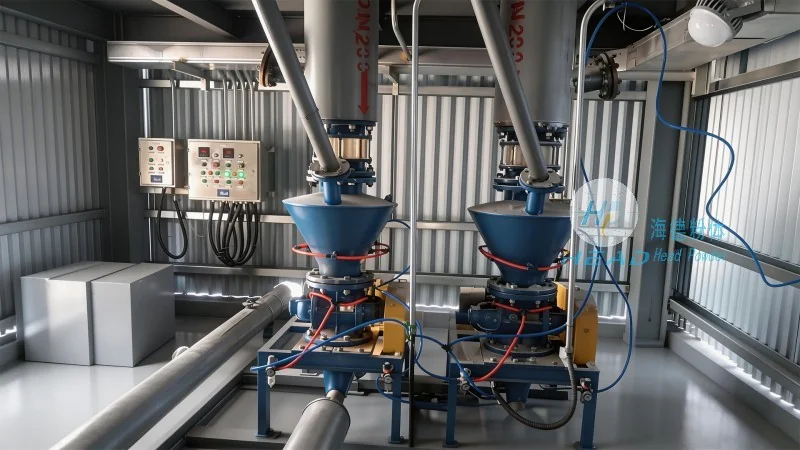
- Conveyors: These are the backbone of the system, responsible for transporting bulk cereal products over short or long distances. Common types include belt conveyors, screw conveyors, and bucket elevators, each suited for different product characteristics and operational needs.
- Elevators: Elevators are used to lift and move cereal materials vertically, often connecting different levels of a production facility. They help in reducing the need for manual labor and ensuring consistent material flow from storage to processing areas.
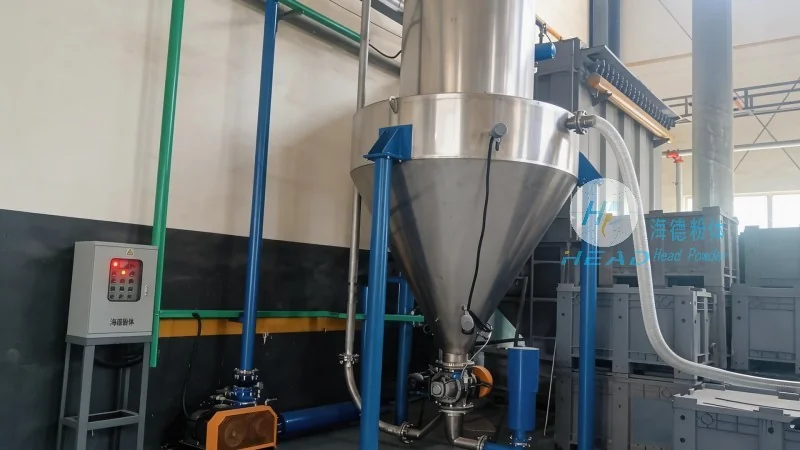
- Storage Silos: Large storage silos are used to store raw cereal ingredients or finished products. These silos are designed to maintain product quality by controlling temperature, humidity, and air circulation. They also facilitate easy access for loading and unloading operations.
- Feeding and Dosing Equipment: This equipment is used to control the flow of cereal materials into processing machines or packaging lines. Precise dosing ensures consistent product quality and prevents overloading or underloading of equipment.
Design Principles for Optimal Performance
The design of a cereal material handling system follows several key principles to ensure efficiency, safety, and durability. These principles are tailored to the unique characteristics of cereal products, which can be delicate, abrasive, or prone to dust generation. The main design principles include:
- Material Compatibility: The system components must be made of materials that are compatible with cereal products. For instance, stainless steel is often preferred for its resistance to corrosion and ease of cleaning, which is critical for maintaining hygiene standards in food processing.
- Flow Optimization: The system is designed to minimize material degradation and breakage during transport. This involves selecting appropriate conveyor speeds, angles, and materials to prevent product damage. Proper flow design also reduces the risk of clogging and ensures consistent throughput.
- Hygiene and Sanitation: Given that cereal products are food items, the material handling system must adhere to strict hygiene standards. Components are designed for easy cleaning and maintenance, with smooth surfaces and minimal crevices where dust or debris can accumulate.
- Energy Efficiency: Modern cereal material handling systems are designed to be energy-efficient. This includes using variable speed drives to adjust conveyor speeds based on production demands, reducing energy consumption during low-load periods.
- Scalability and Flexibility: The system is designed to be scalable, allowing manufacturers to expand their operations as needed. Flexible components enable easy integration of new equipment or modifications to the system without major overhauls.
Role of Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in designing and supplying high-quality cereal material handling systems. With years of experience in the industry, the company understands the unique challenges faced by cereal manufacturers and provides tailored solutions to meet their specific needs. The company’s expertise lies in integrating advanced technology with practical design to deliver systems that are efficient, reliable, and cost-effective. HeadPowder’s systems are built to withstand the demands of continuous operation, ensuring long-term performance and minimal maintenance.
Conclusion
A well-designed cereal material handling system is a critical asset for any cereal manufacturer. It not only improves operational efficiency but also ensures product quality and safety. By adhering to key design principles and utilizing high-quality components, manufacturers can achieve optimal performance and stay competitive in the market. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in providing reliable and efficient material handling solutions for the cereal industry.




