Gray calcium material handling systems are specialized equipment used in industrial settings to transport and manage gray calcium materials efficiently. These systems are crucial for optimizing material flow in production processes, ensuring smooth operations and minimizing downtime. Understanding the components and design principles of such systems is essential for industries dealing with calcium-based materials, particularly those requiring precise handling and consistent quality control.
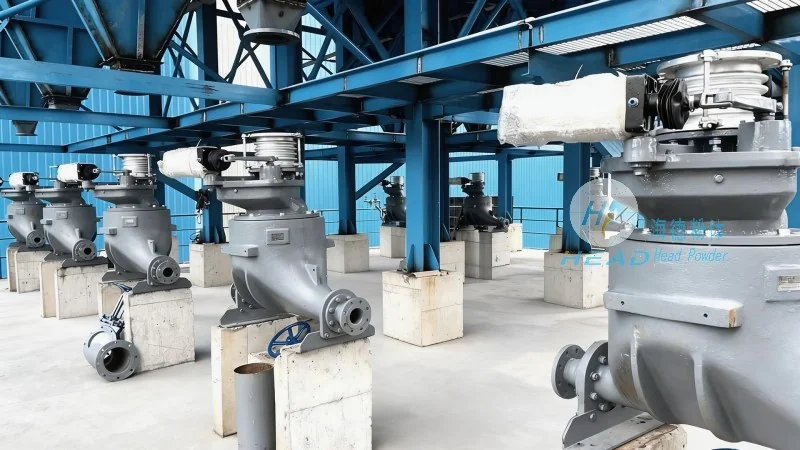
Understanding the Core Components of Gray Calcium Material Handling Systems
At the heart of a gray calcium material handling system are several key components that work in tandem to achieve efficient material transport. The primary elements include feeders, conveyors, storage silos, and control systems. Feeders are responsible for uniformly feeding the material into the system, ensuring a steady flow that prevents blockages or uneven distribution. Conveyors, such as belt or screw conveyors, then transport the material through the system, often elevating or moving it horizontally to reach different processing stages. Storage silos are used to store large quantities of gray calcium, providing a buffer for production needs and maintaining material quality by protecting it from environmental factors like moisture or contamination. Control systems, typically integrated with sensors and automation technology, monitor the entire process, adjusting parameters in real-time to maintain optimal performance and safety.
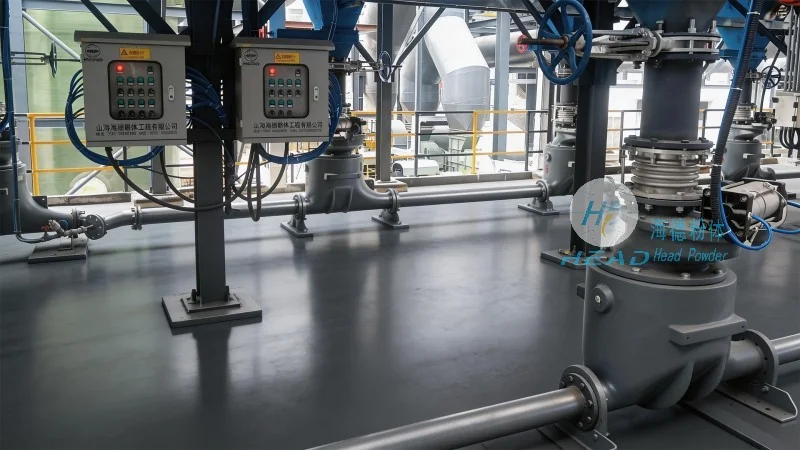
Design Principles for Efficient Gray Calcium Material Handling
The design of a gray calcium material handling system is guided by several critical principles aimed at maximizing efficiency, safety, and durability. One of the fundamental principles is material compatibility, ensuring that all components are constructed from materials that can withstand the chemical and physical properties of gray calcium, such as its abrasive nature and potential moisture content. This involves selecting materials like stainless steel or specialized alloys for conveyor belts and hopper linings to prevent wear and tear. Another key principle is scalability, allowing the system to be adjusted or expanded to accommodate varying production volumes. This flexibility is achieved through modular designs that can be easily reconfigured without major overhauls. Additionally, energy efficiency is a critical consideration, with systems incorporating features like variable speed drives to reduce energy consumption while maintaining performance. Safety is also paramount, with design elements including emergency stop mechanisms, overload protection, and proper ventilation to minimize risks associated with handling potentially dusty or hazardous materials.
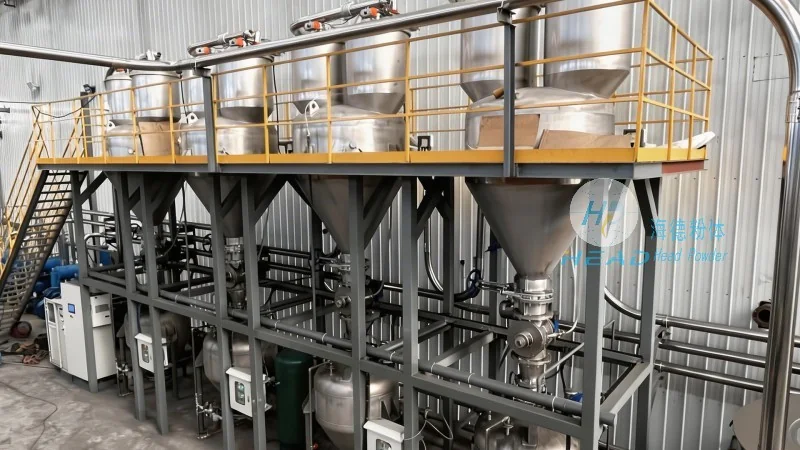
HeadPowder's Expertise in Gray Calcium Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing high-quality gray calcium material handling systems tailored to the unique needs of industrial clients. With years of experience in the industry, HeadPowder has developed a deep understanding of the challenges associated with handling gray calcium, including its handling characteristics and the specific requirements of various applications. The company's approach focuses on providing customized solutions that address the individual needs of each client, whether it's for small-scale operations or large-scale production facilities. HeadPowder's systems are engineered to meet international standards for safety and performance, ensuring reliability and longevity. The company's team of engineers and technicians work closely with clients to assess their specific requirements, from material characteristics to production volumes, and develop tailored solutions that optimize material flow and reduce operational costs. By leveraging advanced technology and rigorous quality control processes, HeadPowder delivers systems that not only meet but exceed industry expectations, helping clients enhance their productivity and maintain a competitive edge in the market.




