

What is a Calcined Lime Material Handling System Equipment? What Are Its Design Principles?
Calcined lime, also known as quicklime, is a vital industrial material utilized across diverse sectors including construction, chemical processing, and environmental remediation. The efficient transportation and handling of this material necessitates specialized equipment and systems to ensure safety, efficiency, and adherence to operational standards. This article explores the core components of a calcined lime material handling system, examining its design principles and the technology that enables seamless material flow.
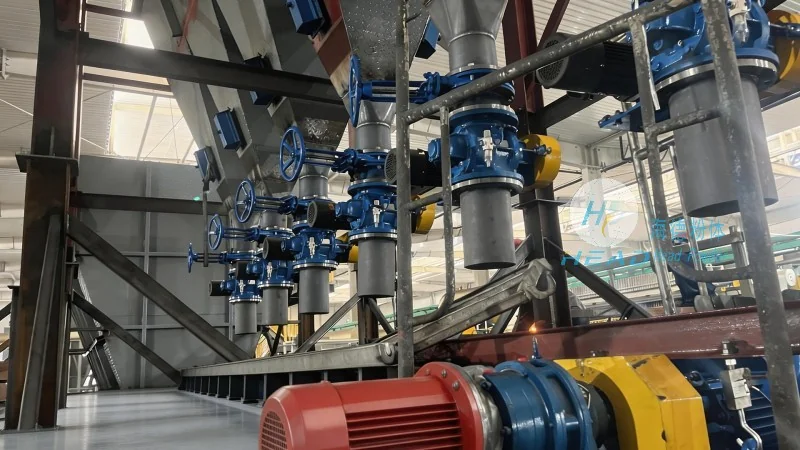
Key Equipment in a Calcined Lime Material Handling System
The calcined lime material handling system typically comprises several critical components engineered to manage the material from storage to processing. These components are designed to address the unique properties of calcined lime, such as its high reactivity and propensity to generate heat during handling. The primary equipment includes:
- Storage Silos: Large, airtight silos are employed to store calcined lime, preventing moisture absorption and preserving the material's quality. These silos are often constructed from corrosion-resistant materials like stainless steel or lined with protective coatings to withstand the chemical properties of lime.
- Conveyors: Various conveyor types, including belt conveyors, screw conveyors, and pneumatic conveyors, are utilized to transport calcined lime from storage to processing units. Belt conveyors are commonly used for bulk material handling due to their high capacity and ability to handle heavy loads. Screw conveyors are ideal for vertical or inclined transport, while pneumatic conveyors use air pressure to move the material, which is particularly effective for dusty or fine powders.
- Feeding Equipment: Specialized feeders, such as rotary valves or vibratory feeders, regulate the flow of calcined lime from the storage silos to the conveyors. These devices ensure a consistent and controlled feed rate, preventing overloading or underloading of the system.
- Processing and Handling Tools: Additional equipment like hoppers, chutes, and dust collection systems are integrated to handle the material during processing. Dust collection systems are essential to manage the fine dust generated during handling, ensuring workplace safety and environmental compliance.
Design Principles for Calcined Lime Material Handling Systems
The design of a calcined lime material handling system adheres to several fundamental principles aimed at optimizing performance, safety, and longevity. These principles are tailored to address the specific challenges associated with calcined lime, including its reactivity, dust generation, and potential for heat buildup. Key design considerations include:
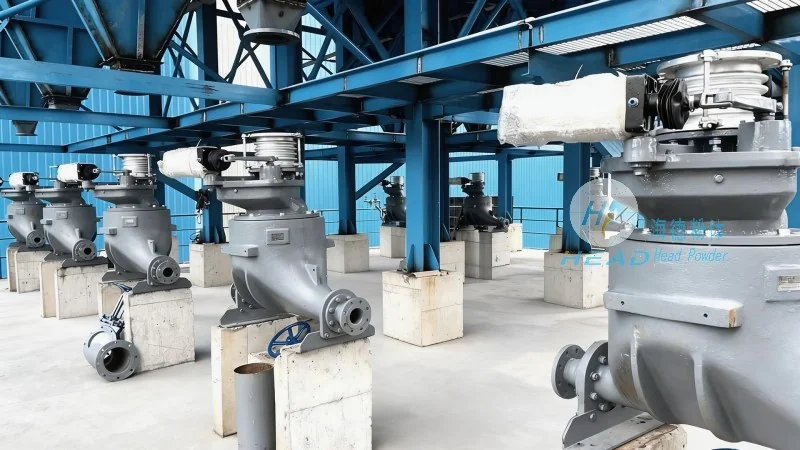
- Material Compatibility: All system components, from silos to conveyors, must be compatible with calcined lime. This involves selecting materials that resist corrosion and chemical attack, such as stainless steel, high-grade alloys, or specialized coatings. Proper material selection prevents degradation and ensures the system's durability.
- Heat Management: Calcined lime can generate significant heat during handling, especially when it comes into contact with moisture or air. The design incorporates effective heat management strategies, such as insulation, temperature monitoring, and cooling systems, to prevent overheating and maintain material quality.
- Dust Control: Dust control is a critical aspect of calcined lime handling due to the material's fine particle size and potential for respiratory hazards. The system includes dust collection and filtration systems to capture and remove airborne particles, ensuring a safe working environment and compliance with environmental regulations.
- Flow Optimization: The design focuses on optimizing material flow to minimize friction, blockages, and energy consumption. This involves selecting appropriate conveyor types, ensuring proper slope and speed, and using efficient feeding mechanisms to maintain a smooth and continuous flow of calcined lime.
- Safety and Compliance: The system is designed to meet industry safety standards and regulations. This includes features like explosion-proof components, emergency shutdown systems, and regular maintenance protocols to ensure safe operation and prevent accidents.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading manufacturer and supplier of industrial material handling systems, specializing in solutions for calcined lime and other bulk materials. With a strong commitment to quality and innovation, headpowder has established itself as a trusted partner in the industry, providing reliable and efficient equipment for various applications.
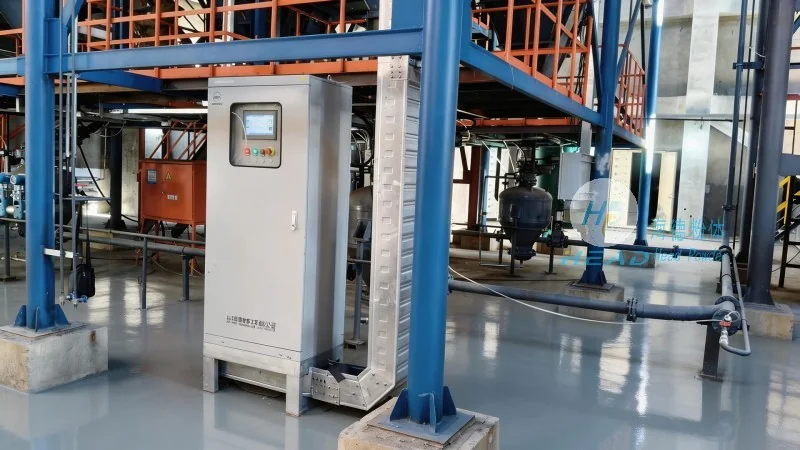
Headpowder's expertise lies in designing and manufacturing customized material handling systems tailored to the specific needs of clients. The company's team of engineers and technicians work closely with customers to understand their operational requirements and develop solutions that enhance productivity, safety, and cost-effectiveness. By leveraging advanced technology and rigorous quality control processes, headpowder ensures that its products meet the highest standards of performance and durability.
Headquartered in Shandong, China, headpowder serves clients globally, delivering high-quality material handling systems to industries worldwide. The company's focus on customer satisfaction and technical excellence has earned it a reputation for delivering reliable solutions that meet the evolving demands of the market.